5 External Factors That Determine Construction Project Success

Read 9 min

What Happens When Key Components of Your Production System Are Missing

There is a pattern that shows up on struggling projects so consistently that it can be predicted. Not guessed predicted. Given the components that are missing from a project’s production system, the symptoms and consequences that follow are almost entirely foreseeable.

That is not a pessimistic statement. It is a liberating one. Because if the consequences are predictable, so are the solutions.

The Framework Behind the Prediction

The Integrated Production Control System IPCS is the operating system that governs how a Lean project runs. It connects three interlocking systems: the First Planner System, the Takt Production System, and the Last Planner System. Each has a distinct role. The First Planner System designs the production environment before boots hit the deck. The Takt Production System creates the rhythm and flow that trades execute against. The Last Planner System manages short-interval commitments at the foreman level. When all three are functioning and integrated, variation drops, visibility goes up, and the field can execute without chaos.

But IPCS does not exist in a vacuum. Before those three systems can function, something else has to be in place the external conditions that either support or undermine everything a well-intentioned project team is trying to build. These are called external factors. And when any of them are missing, the consequences are just as predictable as missing a pull plan or skipping pre-construction meetings.

External Factor One: Paradigm

The first external factor is paradigm the fundamental worldview the owner, developer, or initiator brings to the project. Not their contract language. Not their milestone schedule. Their actual belief about what construction is for and how it should be done.

If the owner’s paradigm is aligned if they genuinely want to do the project right for the sake of people, process, and quality the project team has the conditions to implement Lean properly. If the owner’s paradigm is turn-and-burn, the consequences follow immediately. The owner will force CPM. The owner will move up milestones without adjusting scope or logic. The owner will push for rushing, panic, and overtime. And a well-intentioned contractor no matter how strong their systems or how capable their team will be forced into classical business management behaviors that are directly anti-Lean. Not because they chose it. Because the external paradigm dictated it.

This is important to name clearly: when the owner’s paradigm is misaligned, a great project team can still run a clean, safe, organized site and follow every internal process and still fail to hit the Lean outcomes the system is designed to produce. That is not the team’s fault. That is the system working exactly as designed producing the outcomes the paradigm demanded.

External Factor Two: Mindsets

Paradigm is the overarching worldview. Mindset is how that worldview gets expressed by every individual stakeholder in the system. The owner, the architect, the designers, the subcontractors, the internal corporate leadership all of them must have a mindset that allows the project to be run with respect and stability.

When they do not, the consequences are specific and predictable. An architect without the right mindset becomes adversarial slow-walking RFI responses, withholding submittal approvals, dragging out punch list sign-off. Facilities management without the right mindset withholds coordination for MEP, delays air handler sign-offs, and slows commissioning to a crawl. Internal corporate leadership without the right mindset demands overtime and push behaviors, applies classical business management pressure from above, and makes a strong field leader’s life a living nightmare even when that leader is doing everything right.

The minimum consequence of misaligned mindsets is a difficult working environment. The common consequence is being forced into behaviors that directly contradict the production system being run on the ground.

External Factor Three: Goal of the System

Every project has a stated goal: finish on time, on budget, with quality. But beneath the stated goal, there is often a different goal one that is actually driving behavior. And the system will always achieve the goal that is actually in place, not the one written in the contract.

A superintendent who wants to keep everything in their head rather than build a visible system the actual goal is individual control, and the project will run as a one-person show with firefighting at its center. An owner’s representative who wants to make a name for themselves by scrutinizing the contractor the actual goal is self-promotion, and the project will be buried in bureaucracy and adversarial documentation from start to finish.

When the goal of the system is not honest, clear, and aligned around finishing well with people and quality, the project will achieve the misaligned goal instead despite the best efforts of everyone involved. Goal misalignment does not yield a partial failure. It yields a project organized around the wrong outcome from the first day.

External Factor Four: Structure of the System

Structure is the framework inside which the project must operate contracts, legal agreements, city and jurisdiction requirements, division one specifications, prime agreements, and the composition of the project team itself. When the structure is wrong, it becomes a hard ceiling on performance.

The wrong contract structure creates adversarial incentives. The wrong legal framework means every conflict becomes a claim instead of a conversation. Missing or restrictive division one specs prevent Lean practices from being formalized. A team assembled without the right people in the right roles means the system cannot function as designed. Any one of these structural failures limits what is achievable extending timelines, hurting quality, and undermining production regardless of how capable the field team is.

Here are the structural conditions that most commonly undermine an otherwise well-run project:

  • Contract language that incentivizes adversarial behavior over collaboration
  • Division one specs that mandate CPM use, monthly reporting formats, and push-based controls
  • Prime agreements that restrict the contractor’s ability to build and lead the right team
  • Jurisdictional or city requirements that slow approvals, permits, and inspections outside the project’s control

When these structures are in place, the project team is swimming upstream. Good leaders can still produce good results. But they will work significantly harder for results that a better structure would have made achievable at normal effort.

External Factor Five: Rules of the System

The rules are the operational protocols that govern how the project runs formally through specs and agreements, and informally through culture and habit. Government projects make this especially visible. When the contract mandates CPM, requires float trend reporting, demands monthly narrative reports reviewed by an outside consultant, and prohibits the project team from running a production system on its own terms, the project team will spend significant energy managing compliance with a system that contradicts every Lean principle they are trying to implement.

The consequence is not just inefficiency. It is constant tension between what the rules demand and what the production system requires. And eventually, concessions get made not because the team gave up, but because the rules won.

If your project needs superintendent coaching, project support, or leadership development, Elevate Construction can help your field teams stabilize, schedule, and flow.

Why This Matters for Mental Health

One of the most important reasons to name these external factors clearly is this: when a project fails despite a well-run team following every right process, the people on that team should not go home blaming themselves. They should not pin their identity on the outcome of a system that was designed by paradigm, mindset, goal, structure, or rules to produce a different result.

Running a clean, safe, organized site while following every correct process and still watching the project struggle is not a personal failure. It is the external system exerting exactly the pressure it was built to exert. Knowing that in advance does not make the project easy. But it protects the people inside it from carrying shame that belongs to the system, not to them.

That matters. In an industry already facing a mental health crisis one that CPM itself is a documented root cause of naming what is actually within a project team’s control and what is not is an act of leadership and care.

The Takeaway

Grade your project’s IPCS components every month. Not as a performance review as a diagnostic. If key components are missing, the consequences are predictable. Naming them early means the team can respond with the right action rather than the wrong blame. When the external factors are favorable, run the system with full discipline and protect everything it produces. When the external factors are working against the team, document it, do the right things anyway, and protect the mental health of the people doing the work.

The system either supports flow or it undermines it. The job of leadership is to know which situation they are in and respond accordingly.

As W. Edwards Deming says, “The system that people work in and the interaction with people may account for 90 or 95 percent of performance.”

On we go.

Frequently Asked Questions

What is the Integrated Production Control System?
IPCS is the operating system that connects the First Planner System, the Takt Production System, and the Last Planner System into one integrated framework. When all three are functioning together, production becomes predictable, visible, and controllable. When components are missing, consequences follow in a predictable pattern.

If my project has bad external factors, is it hopeless?
No. A strong team following the right processes can still produce a clean, safe, organized project with good outcomes even against difficult external conditions. What changes is the degree of difficulty and the ceiling on results. Naming the external factors clearly helps the team respond appropriately and protects people from carrying blame that belongs to the system.

How often should a project grade its IPCS components?
Monthly at minimum. The goal is early identification of missing components so consequences can be anticipated and mitigated before they become production failures. The IPCS Guidebook provides a ready-made framework for this assessment.

If you want to learn more we have:

-Takt Virtual Training: (Click here)
-Check out our Youtube channel for more info: (Click here) 
-Listen to the Elevate Construction podcast: (Click here) 
-Check out our training programs and certifications: (Click here)
-The Takt Book: (Click here)

Discover Jason’s Expertise:

Meet Jason Schroeder, the driving force behind Elevate Construction IST. As the company’s owner and principal consultant, he’s dedicated to taking construction to new heights. With a wealth of industry experience, he’s crafted the Field Engineer Boot Camp and Superintendent Boot Camp – intensive training programs engineered to cultivate top-tier leaders capable of steering their teams towards success. Jason’s vision? To expand his training initiatives across the nation, empowering construction firms to soar to unprecedented levels of excellence.
Posted in All

Takt vs CPM Scheduling: Can You Use Both?

Read 8 min

Can Takt and CPM Actually Coexist?

This is one of the most common questions in construction scheduling right now and it deserves a straight answer, not a diplomatic one. Teams are being told to use Takt while their contracts still demand CPM deliverables. Schedulers are trying to run both systems in parallel. And somewhere in the middle, the project is suffering because no one has made a clean decision about which system is actually governing the work.

Let’s get clear on definitions. Because the answer depends entirely on what version of CPM you are talking about.

What Classical CPM Actually Is

Traditional CPM the way it was invented and the way it is most commonly used today has a specific set of characteristics. It is organized by deliverable, not by location, which means it cannot show where work is happening on the building or whether trades are stacking. The logic is hidden inside software that most people in the field cannot read or interpret. It is typically built by one person in a silo statistically one of the primary reasons large, complex projects fail. Its forward and backward pass algorithm removes total project flow and any intentional buffers from the plan. It causes trade stacking too many trades in one area and trade burdening one trade spread across too many areas at once.

The cultural consequences are just as damaging as the technical ones. CPM contracts are written in a way that is adversarial to trade partners. The system puts them in positions they cannot plan to or execute against, then holds them accountable for the results. It has a 15 to 23 percent on-time success rate. That is not a scheduling software problem. That is a production system failure masquerading as a scheduling format. And it is a documented root cause of the mental health crisis in construction because when the system is designed to produce panic, panic is what people experience every day.

Every aspect of classical CPM is worth examining honestly. When it has been compared against every Lean principle all 345 of them it fails every single one. That is not a bias. That is an analysis.

What Takt Actually Is

Takt is a time-by-location production system. It creates a visible rhythm that trades can follow, adjust, and protect. It shows where work is happening, when it is happening, how trades are sequenced through zones, and whether the pace is realistic relative to capacity. It integrates with pull planning, the Last Planner System, advanced work packaging, Kanban, and scrum. It builds buffers intentionally into phases, sequences, and the project end. It makes the plan honest.

Done imperfectly, Takt still works. That is not a case for doing it imperfectly it is a reflection of how much better the underlying production logic is than the system it replaces. A Takt plan built at the macro level, pulled into phase plans with buffers, expanded into a six-week look-ahead, filtered into a weekly work plan and a day plan that stack gives the field something it can actually use. Something it can see. Something that tells a crew not just what to do, but where to do it and when to hand off.

When Takt and CPM are compared directly against the definition of Lean respect for people and resources, stability and standardization, one-piece flow, flowing together on a Takt time, visual systems for total participation, and quality through continuous improvement CPM fails every pillar. Takt complies with all of them. This is not theoretical. The analysis exists, documented in full in 10 Myths of CPM.

The Coexistence Question

So back to the original question: can they coexist?

The philosophies cannot. Takt is a flow-based, people-centered, location-driven production system. CPM is a deliverable-based, date-driven, push-oriented reporting tool. Their underlying assumptions about how work should be managed are directly contradictory. Running both as governing systems on the same project creates a split the Takt plan tells the field one thing, the CPM tells the contract something else, and the team spends energy managing the gap between them instead of building.

What can coexist is this: build and run the project with Takt. Export to CPM for contractual reporting. That is a legitimate use of CPM software as a reporting output from a Takt-governed production system, not as the operating system the field lives by. Intact software does this with a button click. The project runs on Takt. The CPM report gets generated for whoever needs to see it. The field never touches the CPM because the field does not need it.

Here are the conditions under which CPM actually belongs on a project:

  • As a contractual deliverable generated from a Takt-governed production plan
  • As a simplified waterfall reference for milestone-level owner reporting
  • As a historical record after the fact not as a steering tool during production

That is the extent of CPM’s legitimate role. Anything beyond that using it to govern sequencing, manage trade flow, track production, or recover schedule is asking it to do something it was never designed to do and cannot do well.

Why CPM’s Recovery Methods Make Things Worse

When a CPM schedule shows the project is behind, there is exactly one solution it can offer: crash the critical path. Add resources. Work overtime. Rush, push, and panic. Financially incentivize the contractor. Bring out too many materials and flood the field with congestion.

Every one of those responses is the exact opposite of what a Lean production system would do. Every one of them hurts construction. Adding resources into an already congested site creates more trade stacking and more conflict. Overtime burns out the workforce, drops quality, and increases safety risk. Rushing means defects get built in rather than caught. Financial incentives without system fixes just buy you faster chaos.

There is not a single thing in the CPM system or its philosophy that helps a project recover production. It can tell you that you are late. It cannot tell you how to get back without hurting flow, people, and outcomes. That gap is not a minor limitation. It is the reason Takt exists.

What a CPM 2.0 Would Require

Could someone build a version of CPM that incorporated flow logic, location-based sequencing, capacity alignment, buffers, and crew-level planning? In theory, yes. But by the time all of those elements are incorporated, it is no longer CPM. It is Takt. The industry would spend years retrofitting a fundamentally broken philosophy when the replacement system already exists, already works, and already integrates with every collaborative planning tool in the industry.

The path forward is not a better version of the old system. It is accepting that the old system was never a production system to begin with and building on the one that is.

If your project needs superintendent coaching, project support, or leadership development, Elevate Construction can help your field teams stabilize, schedule, and flow.

The Question Worth Asking

The better question is not “can Takt and CPM coexist?” The better question is: what is actually governing your project? What does the field use to make daily decisions? What tells a foreman where to go and when to hand off? What surfaces bottlenecks before they become schedule emergencies? What gives trade partners a rhythm they can commit to?

If the answer to those questions is CPM, the project is being run reactively. If the answer is Takt, the project has a production system. And the sooner that distinction is made clearly by the leadership team, by the contract, by the culture the sooner the project can stop managing the gap between two incompatible systems and start actually building.

As Taiichi Ohno says, “Where there is no standard, there can be no improvement.”

On we go.

Frequently Asked Questions

Do I have to choose between Takt and CPM on my project?
You have to choose which system governs the field. Build and run the project with Takt. If contractual obligations require a CPM deliverable, export it from your Takt plan. The field should never be trying to execute from a CPM schedule while a Takt plan exists the conflict between the two creates more confusion than either system resolves.

Why does CPM have such a low success rate?
Because CPM is not a production system. It does not account for trade flow, zone capacity, buffers, or location-based sequencing. It is built in a silo by one person, in a format that field teams cannot read or execute from. Projects that live by CPM are reacting to a document that never reflected production reality in the first place.

What does Takt integrate with besides itself?
Takt integrates cleanly with pull planning, the Last Planner System, advanced work packaging, Kanban, and scrum. Each of these systems functions better when paired with Takt than when paired with CPM, because Takt provides the flow logic, location structure, and buffers that make collaborative planning tools work the way they were designed to.

If you want to learn more we have:

-Takt Virtual Training: (Click here)
-Check out our Youtube channel for more info: (Click here) 
-Listen to the Elevate Construction podcast: (Click here) 
-Check out our training programs and certifications: (Click here)
-The Takt Book: (Click here)

Discover Jason’s Expertise:

Meet Jason Schroeder, the driving force behind Elevate Construction IST. As the company’s owner and principal consultant, he’s dedicated to taking construction to new heights. With a wealth of industry experience, he’s crafted the Field Engineer Boot Camp and Superintendent Boot Camp – intensive training programs engineered to cultivate top-tier leaders capable of steering their teams towards success. Jason’s vision? To expand his training initiatives across the nation, empowering construction firms to soar to unprecedented levels of excellence.
Posted in All

Survey Invert Calc Sheet

Read 10 min

The Best Systems Don’t Just Catch Mistakes. They Protect the People Who Would Otherwise Be Blamed for Them.

Here’s the deal: when something goes wrong with pipe inverts on a construction project, the conversation almost always starts in the same place the foreman. Who ran the shots? Who set the grade? Who was responsible for this? And nine times out of ten, the answer points to a person before it points to a process. That’s not accountability. That’s scapegoating a skilled professional for a system failure that never gave them a structured way to document what they did, verify what they found, and catch an error before it became a costly problem in the ground.

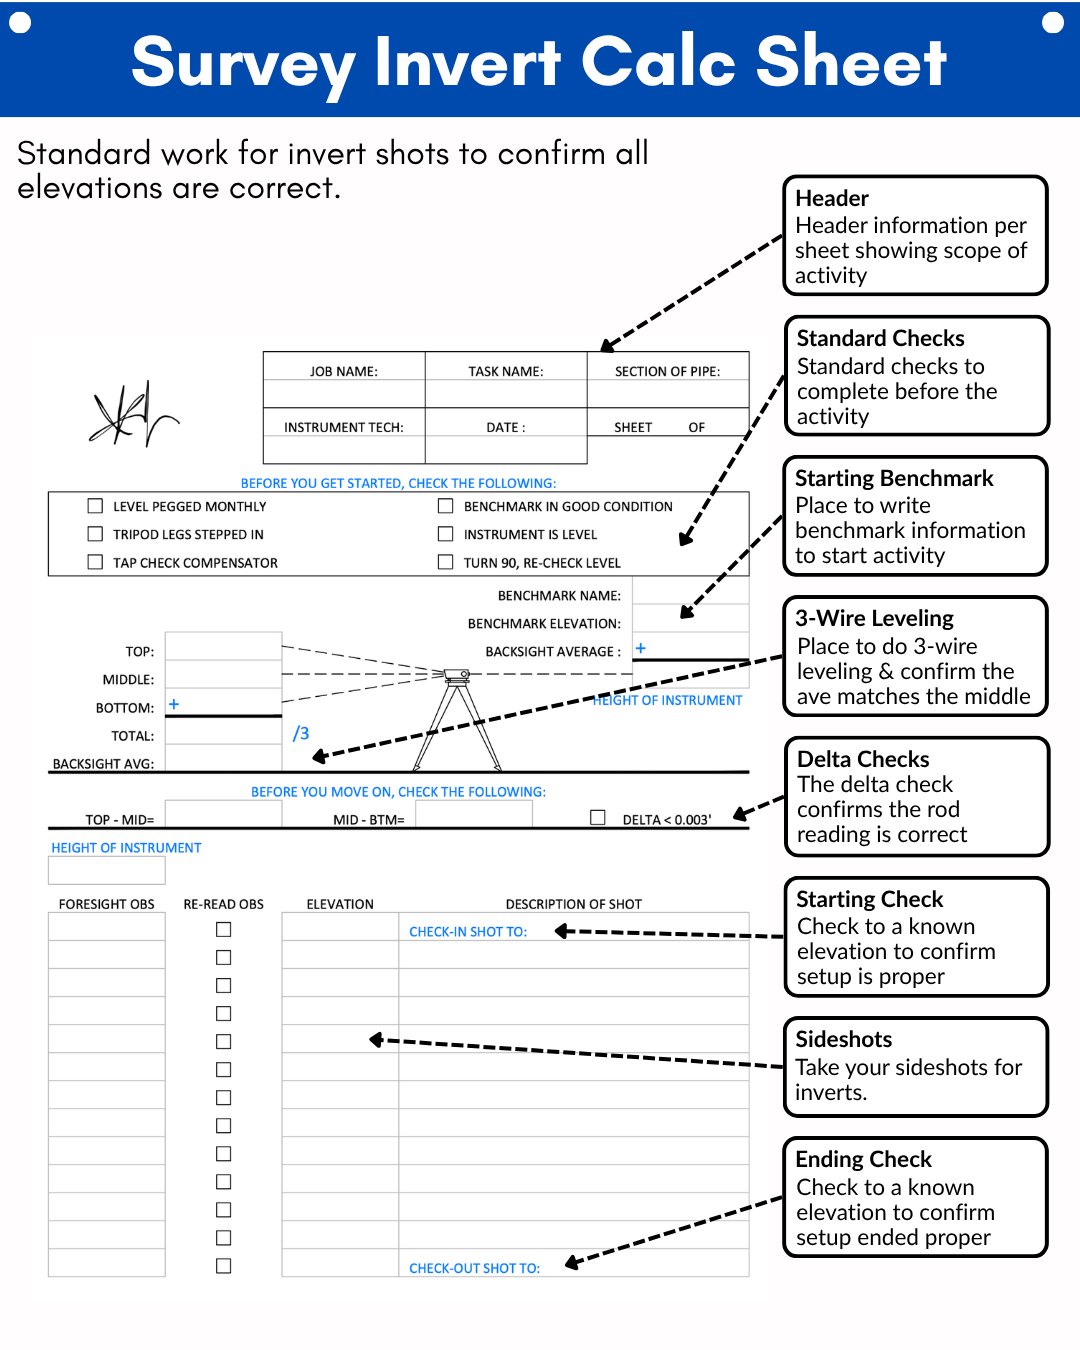
The Survey Invert Calc Sheet is not a compliance form. It’s a protection system. It’s standard work designed to verify every elevation is correct before the pipe goes in the trench and to provide the documented evidence that tells the team exactly what happened when something doesn’t go right. It protects the foreman, protects the project, and protects the crews who are out there grinding every day without the documentation that would defend them if anything ever came into question.

What Happens Without Standard Work for Survey Operations

Most pipe crews run invert shots with a level of skill that comes from years of field experience. The instrument tech sets up, takes a backsight, records the height of instrument, takes the sideshots, and moves on. The process is known. The problem is that “known” is not the same as “documented.” When the shots are being taken correctly, everything is fine and nobody notices the absence of a formal process. When something goes wrong an error in the benchmark elevation, a compensator that wasn’t tapped, a delta on 3-wire leveling that was outside tolerance but nobody wrote it down the absence of documentation becomes a serious problem.

The investigation that follows has no data to work with. Nobody knows whether the setup was checked. Nobody knows whether the benchmark was verified before work started. Nobody knows if the check-in shot to a known elevation confirmed the setup before sideshots were taken. The foreman remembers what they did, but memory in a legal or contractual dispute is not documentation. The investigation cannot find the root cause because the root cause was never recorded. So the default answer is the person standing closest to the problem the foreman who ran the shots and the system that failed to provide them proper standard work gets no scrutiny at all.

The system failed them. They didn’t fail the system.

A Story About What Documentation Changes

I was on a large civil project years ago where we had a significant invert discrepancy discovered during final inspection on a section of force main. The pipe was in. The grade was off. The cost to investigate, expose, and correct was significant, and the first conversation was about who was responsible. The pipe foreman was one of the best I had worked with meticulous, experienced, and genuinely invested in the quality of the work. But when the question came about what documentation existed for the shots that established grade on that section, there was nothing formal. No recorded backsight check. No benchmark verification at the start of the day. No check-out shot confirming the setup held through the shift.

The problem was eventually traced to a benchmark that had been disturbed by equipment traffic and was no longer at its originally surveyed elevation. The foreman had done everything right relative to the information they had. But without a documented check-in shot to an independent known elevation, there was no way to prove when the benchmark discrepancy began. The foreman absorbed accountability for a system problem. Standard work would have caught the elevation error before a single joint was made and would have protected the foreman from a consequence they didn’t deserve.

What the Survey Invert Calc Sheet Is Built Around

The calc sheet is standard work a defined, documented process that every instrument tech follows for every invert shot, every time. Standard work is the foundation that allows continuous improvement to compound without the system constantly resetting. When the process is standardized, variation becomes visible. When variation is visible, root cause analysis becomes possible. And when root cause is possible, the system improves instead of repeating the same failure in the next zone.

The header section establishes scope before the shot begins job name, task name, section of pipe, instrument tech, date, and sheet number. This is not administrative overhead. This is chain of custody for field data. When a question comes up weeks later about which shots were taken when, and by whom, the header tells the story without requiring anyone’s memory.

The pre-flight checklist level pegged monthly, tripod legs stepped in, compensator tapped, benchmark in good condition, instrument is level, turn 90 and re-check runs before any elevation is taken. These are the conditions that make the shot valid. A compensator that wasn’t tapped introduces systematic error that affects every foresight reading taken from that setup. Tripod legs that weren’t properly stepped in on soft ground can shift during the session. The checklist catches these conditions before the data is compromised not after.

Watch for these signals that invert survey work on your project lacks adequate standard work:

  • Invert discrepancies that cannot be traced to a specific cause because no setup data was recorded
  • Benchmark verification happening verbally rather than as a documented step before shots begin
  • No check-in shot to a known elevation at the start of each setup to confirm instrument configuration
  • Delta checks on 3-wire leveling not being recorded, leaving no way to verify rod reading accuracy
  • No check-out shot at the end of the day to confirm the setup held through the session

The Three-Wire Method and the Delta Check

The 3-wire leveling section of the calc sheet is where precision is verified through mathematics rather than assumption. The instrument tech reads the top, middle, and bottom crosshairs on the rod, records all three, and averages the top and bottom to confirm it matches the middle reading within a defined tolerance. The delta check confirming the difference between top and middle matches the difference between middle and bottom within 0.003 feet is the quality gate that confirms the rod reading is correct before the height of instrument is calculated.

This is Poka-Yoke applied to field survey work. The delta check cannot pass on a misread. If the rod was read incorrectly if the wrong graduation was observed the math will not close. The error is caught at the source, before it propagates into the height of instrument calculation and then into every foresight reading taken from that setup. A delta failure at this step costs sixty seconds to re-level and re-read. The same error discovered in the ground after pipe installation costs days and significant money.

The check-in shot to a known elevation before sideshots begin, and the check-out shot to the same known elevation at the end of the day, bookend the session with independent verification. If the setup was correct at check-in and confirmed at check-out, every reading taken in between has a verified bracket around it. If the check-out doesn’t match, the team knows immediately that something changed during the session and exactly which shots need to be reviewed.

Why This Is a Foreman Protection Question, Not a Paperwork Question

Jason Schroeder teaches that the foreman is the most important leadership role in construction the last planner closest to the work, the primary production leader, the person the entire system is designed to support. When foremen are forced into daily firefighting because the system failed to give them what they need, the system is failing them. And when something goes wrong and the foreman is the default answer because there is no documented system that protected them, the organization has compounded that failure with an injustice.

The Survey Invert Calc Sheet is how the system shows up for the foreman before the shot begins. It says: we designed a process that documents your setup, verifies your benchmark, confirms your accuracy, and creates a record that tells the real story if anything ever needs to be investigated. That is not micromanagement. That is what leader standard work looks like in the field. It gives the foreman the tools to back up their work and the checks to catch a problem before it costs the project or costs them professionally.

If your project needs superintendent coaching, project support, or leadership development, Elevate Construction can help your field teams stabilize, schedule, and flow. Standard work at the crew level including field survey standard work is part of the foundation that makes flow possible and people protectable.

Build the Standard Before the Pipe Goes in the Ground

Here is the challenge. Look at the invert survey process on your current project and ask: is there documented standard work that every instrument tech follows for every setup? Is the benchmark being verified to an independent check point before shots begin? Is a delta check being run on every 3-wire reading? Are check-in and check-out shots being recorded for every session?

If the answer to any of those questions is no, the process is relying on individual skill and memory to protect the project and the people doing the work. Standard work doesn’t replace skill. It documents it. It makes the skilled person’s good work visible, verifiable, and defensible when the question ever gets asked. Build the standard. Train to it. And protect the foremen who are out there grinding every day with a system worthy of the work they do.

As Jason Schroeder teaches: “If work is not standardized, reliability becomes luck.” The invert shot is not where we want to be lucky.

On we go.

Frequently Asked Questions

What is the Survey Invert Calc Sheet and what does it standardize?
It’s standard work documentation for pipe crew invert shots covering pre-flight instrument checks, 3-wire leveling with delta verification, benchmark recording, check-in and check-out shots, and a complete foresight log for every sideshot taken during the session.

What is a delta check and why does it matter for accuracy?
The delta check confirms that the rod readings from the top, middle, and bottom crosshairs are mathematically consistent within 0.003 feet. A delta failure reveals a misread before it affects the height of instrument calculation and every subsequent foresight taken from that setup.

How does standard work protect the foreman when something goes wrong?
Documented standard work creates an evidentiary record of what was done, when, and under what verified conditions. When a discrepancy is investigated, the data points to the actual root cause benchmark issue, equipment problem, or field condition change rather than defaulting to the person who ran the shots.

If you want to learn more we have:

-Takt Virtual Training: (Click here)
-Check out our Youtube channel for more info: (Click here) 
-Listen to the Elevate Construction podcast: (Click here) 
-Check out our training programs and certifications: (Click here)
-The Takt Book: (Click here)

Discover Jason’s Expertise:

Meet Jason Schroeder, the driving force behind Elevate Construction IST. As the company’s owner and principal consultant, he’s dedicated to taking construction to new heights. With a wealth of industry experience, he’s crafted the Field Engineer Boot Camp and Superintendent Boot Camp – intensive training programs engineered to cultivate top-tier leaders capable of steering their teams towards success. Jason’s vision? To expand his training initiatives across the nation, empowering construction firms to soar to unprecedented levels of excellence.
Posted in All

Pre-fabricated Wall Panels

Read 10 min

Most People See a Wall. High-Performing Project Teams See a Five-Step Manufacturing Process.

Here’s the deal: every wall on a construction project is manufactured somewhere. The question is not whether it gets built it’s whether it gets built in a controlled environment designed for precision and speed, or in a field environment designed for everything but that. On most projects, the answer is the field. Studs are cut on a chop saw in the corridor. Frames are assembled on an uneven concrete deck. MEP rough-in happens in conditions that no manufacturing engineer would design for. And the variation that results from field measurement tolerances, weather exposure, crew interruption, and ergonomic compromise gets absorbed as rework, coordination failures, and schedule loss that nobody planned for.

The teams building the fastest, highest-quality projects in construction today are asking a different question: what if the wall wasn’t built in the field at all?

What the Field Manufacturing Assumption Actually Costs

Framing is one of those scopes that looks fast on the schedule until it’s actually happening. The cut lists get generated. The studs get delivered in full-length bundles. The layout crew marks the deck and ceiling track. The framers cut, set, and fasten one stud at a time, in ambient conditions, with weather, concrete dust, and trade traffic as constant variables. And the MEP rough-in that follows happens after the frame is standing, in whatever clearance the frame allows, often in positions that no ergonomics study would recommend.

Now add the variation. A stud cut two inches short on a busy deck. A header framed at the wrong height because the dimension on the shop drawing didn’t match the field condition. A plumbing rough-in that conflicts with electrical because the two trades never looked at each other’s work in the same room before installation began. Each of those variation events costs more to fix in the field than it would have cost to prevent in a controlled shop environment. The field manufacturing assumption is not just slow it’s variable. And variability is what destroys production rhythms and compresses the schedules that Lean teams work hard to protect.

A Story That Changed How I Think About This

I was part of a team on a large multifamily project years ago where we were running interior framing and MEP rough-in sequentially, floor by floor, exactly the way it had always been done. The framing pace was reasonable. The MEP rough-in that followed was not. The electrical and plumbing trades were constantly working in framing that was inconsistently built studs at varying heights, headers that required shimming, track that had walked during the frame because nobody had designed a better system for holding it during assembly. Every inconsistency cost the MEP trades time. The inspection failure rate on rough-in was higher than expected, and the rework drove compression into the schedule that took weeks to recover.

When I talked to the framing foreman about it later, his comment stuck with me: “If I could build this wall on a table instead of a deck, it would take half the time and look twice as good.” He wasn’t wrong. The problem wasn’t the crew. The problem was that nobody had ever designed the work environment to match what the scope actually required. The system failed them. They didn’t fail the system.

What the Pre-Fabricated Wall Panel System Is Built Around

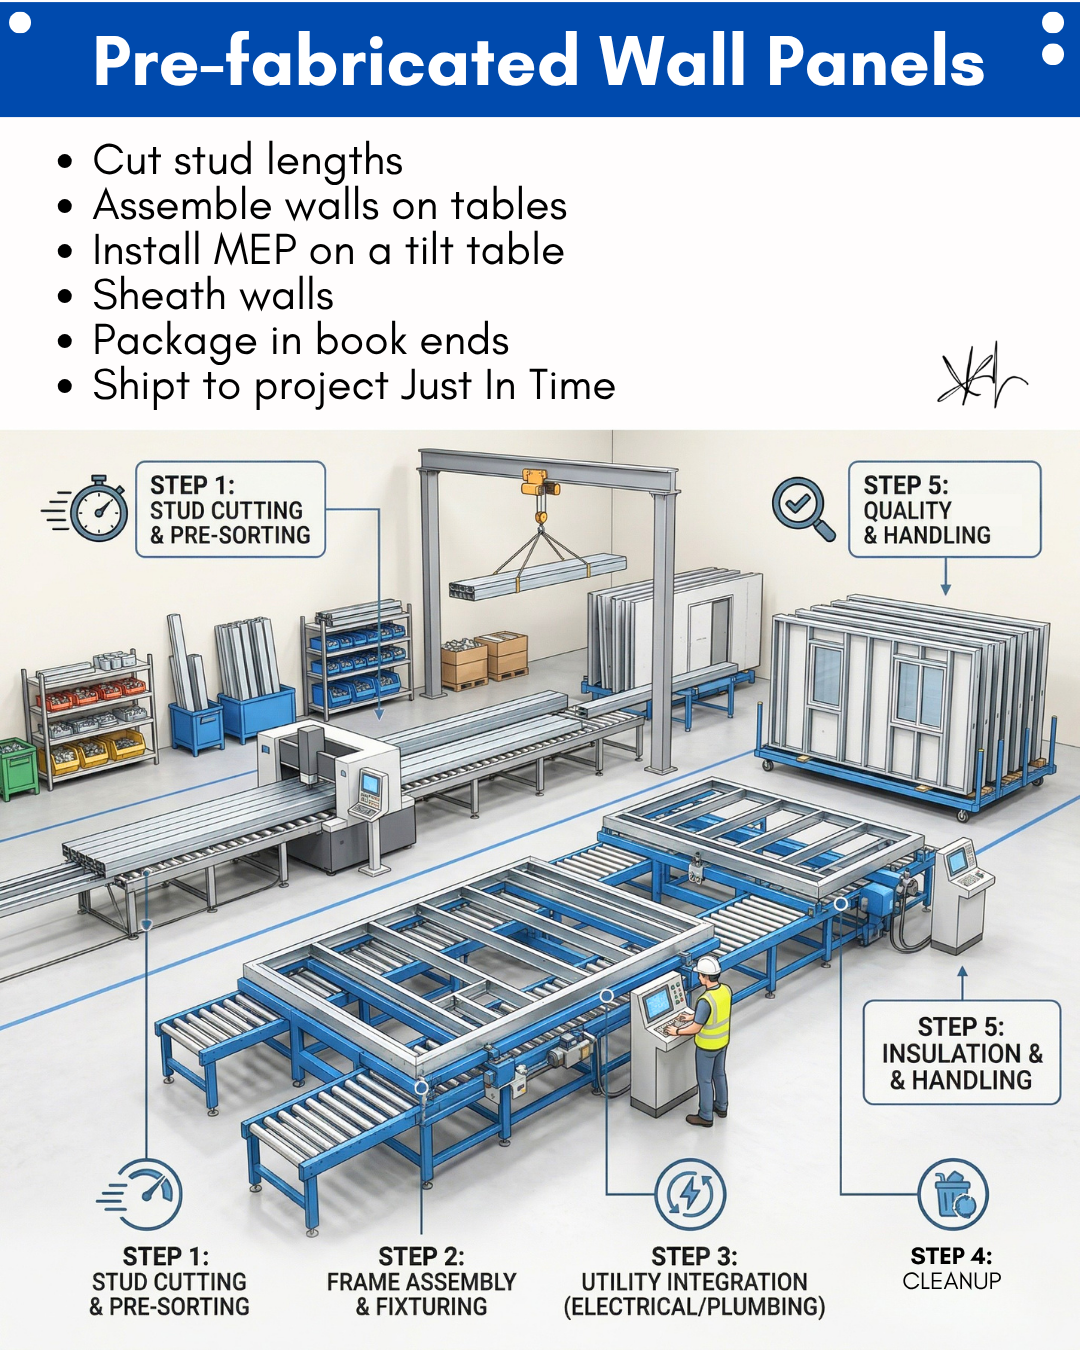
The image in this post shows a five-step manufacturing process that takes everything uncomfortable about field framing and moves it into a controlled factory environment where precision is designed in and variation is designed out.

Step one is stud cutting and pre-sorting. Automated cutting equipment processes studs to exact specified lengths based on the wall panel design. There is no tape measure in this step. No chop saw on an uneven deck. No journeyman deciding whether a piece that’s a quarter-inch short is close enough. The cut is set by the machine. Every stud for every panel comes out at the exact dimension the panel requires. Pre-sorting organizes cut members by panel assignment so the assembly step never has to search for the right piece.

Step two is frame assembly and fixturing. Frames are assembled on dedicated flat assembly tables with fixtures that hold track, studs, and headers in position while fastening happens. The fixturing does what field conditions cannot it holds the geometry true during assembly so every panel that comes off the table is square, plumb, and dimensionally consistent with every other panel. This is Poka-Yoke applied to framing: the fixture makes the wrong position physically difficult. The right position is the easy position.

Watch for these signals that field framing is producing schedule and quality problems on your project:

  • MEP rough-in is repeatedly discovering framing that doesn’t match the shop drawings
  • Inspection failure rates on rough-in are higher than expected because of field coordination issues between framing and MEP
  • Field framing crews are spending significant time on layout and measurement rather than assembly
  • Weather conditions are affecting framing quality or safety on exposed floors
  • MEP tradespeople are working in awkward positions because rough-in access wasn’t designed into the panel before framing

Steps Three Through Five: MEP Integration, Quality, and Just-in-Time Delivery

Step three is utility integration electrical and plumbing rough-in installed on the panel while it is horizontal on a tilt table. This is the step that changes the entire MEP rough-in equation. Instead of an electrician working overhead in a standing frame, the panel is flat. The tilt table brings the work to an ergonomic height and angle. The electrician installs at a comfortable position, with unobstructed access to every conduit path, every box location, and every penetration. The quality of that work the precision of box placement, the consistency of conduit runs, the cleanliness of the installation is demonstrably better when the worker is not fighting gravity and access simultaneously. And the coordination conflict that would have surfaced in the field between electrical and plumbing? Resolved at the design stage, before a single piece of material is cut.

Step four is sheathing the wall, followed by the QC and handling step. Each panel is inspected before it leaves the fabrication yard dimensional check, MEP rough-in verification, sheathing alignment, fastener quality. Defects caught in the yard cost minutes. The same defect caught in the field after the panel is installed costs hours. The panels that pass QC are packaged in book ends for transport, protecting panel geometry and preventing damage during shipping. The book end packaging is the same principle as the dunnage in the staging yard every detail of storage and transport is designed to preserve the quality that the manufacturing process created.

Shipping to the project just in time completes the system. Panels arrive at the site when the zone is ready to receive them not staged in the corridor for two weeks creating a logistics obstacle for every other trade. The truck pulls up, the panels come off, and installation begins. The job site becomes an assembly site rather than a manufacturing site, and the math on speed, safety, and quality immediately starts working in the project’s favor.

Why This Is a Lean Question, Not Just a Framing Question

Jason Schroeder teaches that leveraging prefabrication and modularization designing to the work package is one of the two major ways to accelerate a project schedule. Teams that have implemented prefabrication properly have gained five to twenty percent on overall project schedule, while trade partners have gained margin through reduced rework and faster cycle times. Those numbers are not theoretical. They are the documented outcome of moving manufacturing from the field to a controlled environment that was designed to do it well.

The Takt Production System moves trades through zones on a defined rhythm. Prefabricated panels support that rhythm because the installation step setting a completed panel rather than building a wall from raw materials is faster, more consistent, and more predictable than field framing. When each zone’s wall panel installation takes a known, consistent duration that the Takt planning can count on, the train of trades flows. When field framing varies by twenty percent zone to zone because of field conditions, the train stalls. The prefabrication decision is not just an efficiency decision. It is a production rhythm decision that affects every trade behind framing in the sequence.

If your project needs superintendent coaching, project support, or leadership development, Elevate Construction can help your field teams stabilize, schedule, and flow. Prefabrication is part of the supply chain work that feeds the production plan and it starts in preconstruction, before the schedule is built around assumptions that don’t have to be true.

Design the Wall Before You Build the Wall

Here is the challenge. On your next project with significant interior framing scope, bring the prefabricated wall panel conversation into the preconstruction process before the production plan is locked. Ask the fabricator what lead time looks like, what the panel design workflow requires from the architect and MEP engineers, and what the comparison looks like between prefabricated and field-built when all costs are fully accounted for including field rework, MEP coordination failures, inspection losses, and schedule compression.

The answer will almost always reveal that the field manufacturing assumption was not the most efficient or most reliable path. Plan it first. Build it in the yard. Deliver it just in time. And let the installation crew do what they should be doing: assembling a completed product, not manufacturing raw materials in the field.

As Jason Schroeder teaches: “What would it mean if we had the design, the prefab, the installation instructions, and all the preparation needed clearly articulated in a package for every crew so they could hit better durations all together collectively?” That’s the wall panel. That’s the question. Answer it in preconstruction.

On we go.

Frequently Asked Questions

What is a pre-fabricated wall panel and how is it different from field framing?
It’s a complete wall assembly framed, MEP-roughed, and sheathed built in a controlled factory environment and delivered to the site ready to install. Field framing builds the same wall from raw materials in ambient site conditions, which introduces more variation and takes longer.

How does MEP rough-in on a tilt table improve quality over field installation?
The tilt table positions the horizontal panel at an ergonomic working height, giving MEP tradespeople full access to every box location and conduit path without working overhead or around standing frame constraints. Quality and installation speed both improve significantly.

How does just-in-time delivery of panels support site logistics?
Panels arrive when the zone is ready to receive them not weeks early creating staging obstacles. This keeps corridors and staging areas clear, protects panel quality during storage, and keeps the logistics system aligned with the production plan.

If you want to learn more we have:

-Takt Virtual Training: (Click here)
-Check out our Youtube channel for more info: (Click here) 
-Listen to the Elevate Construction podcast: (Click here) 
-Check out our training programs and certifications: (Click here)
-The Takt Book: (Click here)

Discover Jason’s Expertise:

Meet Jason Schroeder, the driving force behind Elevate Construction IST. As the company’s owner and principal consultant, he’s dedicated to taking construction to new heights. With a wealth of industry experience, he’s crafted the Field Engineer Boot Camp and Superintendent Boot Camp – intensive training programs engineered to cultivate top-tier leaders capable of steering their teams towards success. Jason’s vision? To expand his training initiatives across the nation, empowering construction firms to soar to unprecedented levels of excellence.
Posted in All

The One Thing to Fix on Your Jobsite First (Superintendent Tips)

Read 8 min

The First Thing to Fix on Monday Morning

If someone said you could only fix one thing on your jobsite Monday morning one thing the answer might surprise you. Not the schedule. Not the pull plan. Not the weekly work plan meeting.

The bathrooms.

That is not a joke. It is not a quirky leadership metaphor. It is the most honest answer to where real Lean transformation begins and it comes from Paul Akers, who built one of the most celebrated Lean companies in the country. He said if you want to start with Lean, start in the bathroom. That advice was taken seriously. And the projects that applied it proved the principle true.

What the Bathroom Actually Reveals

How a project team treats the humans who build the building the environment it gives them, the dignity it affords them is the most accurate indicator of the level of care across every other part of the project.

If the bathrooms are dirty, poorly stocked, unventilated, and degrading, the message to every worker on that site is clear: you are not important enough to be taken care of. That message does not stay in the bathroom. It travels into every zone, every morning huddle, every interaction between the crew and leadership. Workers read the environment the way a project manager reads a schedule. They know exactly what the project thinks of them by the conditions they are given.

Graffiti on bathroom walls is not random vandalism. It is a cultural output. Pee bottles are not a workforce problem. They are a leadership signal. When workers feel disrespected, they respond in kind not because they are bad people, but because the system communicated that no one cared, so why should they. The first step on every project is to win over the workforce. And the bathroom is the first opportunity to do it or the first opportunity to fail.

What a Remarkable Restroom Actually Looks Like

Before running a first project as superintendent, a decision was made: read Paul Akers’ Two Second Lean twice and actually do it. The bathroom project that followed became one of the defining experiences of the career.

The team needed a three-wide trailer. What was negotiated instead was an eight-wide. Half became a lunchroom. The other half was fully built out holes drilled in the trailer floor, vents run up through the roof, custom stalls built for both male and female facilities. Real wall-hung toilets. Epoxy white walls. Plungers in every stall. Replenishable supplies. Sinks, trash cans, urinals, signage. A place to hang a hard hat. A sound bar installed by a worker who knew car audio, so music played and privacy was protected. Automatic air fresheners. Sealed insulation so there were no smells. Chuck Norris jokes on the walls.

Every worker on that project had access to a clean, dignified, functional restroom the same standard as the project management team. Because that is the standard. If the facilities are not good enough for the project management team’s grandmother, they are not good enough for the workforce.

The result? No graffiti. Not in the bathroom. Not in the lunchroom. Not anywhere on the jobsite. No pee bottles. No vandalism. Total participation from the workforce because the workforce had been shown, from day one, that they were valued.

The Algorithm Behind the Principle

There is a simple formula that governs how projects perform. It is not complicated. How the workers are treated is how they will treat the building. How they treat the building is how the building will treat the client. How the building treats the client is the project team’s overall reputation.

That chain of cause and effect starts at the bathroom door. It does not start in the schedule review. It does not start in the milestone meeting. It starts in the first environment workers walk into every day the one that tells them whether this project sees them as craftspeople worthy of care or as production units to be managed and extracted from.

The teams that understand this build remarkable projects. The teams that skip it spend the rest of the project fighting a workforce that never fully bought in because leadership never gave them a reason to.

Here are the conditions that a well-maintained, dignified worker facility produces on a jobsite:

  • Workers arrive to a clean, respectful environment and bring that standard with them into their work
  • No graffiti, vandalism, or disrespect because the project modeled respect first
  • Total participation in cleanliness and site standards because the team feels ownership, not resentment
  • A culture signal that travels from the bathroom into every other system on the project

This Is a Leadership Investment, Not a Budget Line

The most common pushback is simple: the PM did not budget for it. And the response to that is equally simple: it does not matter. How the workers are treated and how they are built up as human beings first that is how the rest of the jobsite will go. No budget constraint justifies sending people to degrading facilities for months at a time. And practically speaking, the cost of decent restrooms is trivial compared to the cost of a disengaged workforce, vandalism, turnover, and a project site that never achieves total participation.

The investment is not in bathroom fixtures. It is in the workforce. It is in the signal that goes out to every trade partner, every crew member, every foreman from the moment the trailer is set up: this project respects people. This project takes care of the humans who build it. This project earns trust by demonstrating it not by demanding it.

That investment pays back in the only currency that matters on a project: people who show up committed, who take ownership of the work, who treat the building the way they were treated.

If your project needs superintendent coaching, project support, or leadership development, Elevate Construction can help your field teams stabilize, schedule, and flow.

Where Lean Actually Starts

There is a sequence to Lean implementation that cannot be skipped. Respect for people and resources must come first. Stability a clean, safe, organized environment must be established before any other Lean system can function. Total participation follows because people who feel respected are willing to participate. Visual systems work because a clean environment is a visible one. Quality and continuous improvement emerge because the foundation is solid enough to build on.

Pull the sequence apart and the whole system collapses. You cannot have total participation without respect. You cannot have stability without cleanliness. You cannot have cleanliness without leadership that takes it seriously enough to go first to model the standard, enforce it, resource it, and live by it alongside the workforce.

That is why the bathroom matters. Not because bathrooms are the most complex Lean challenge. Because they are the most honest one. They strip away all the project management language and the Lean vocabulary and the scheduling systems and ask the most basic question: do you actually care about the people who build your buildings?

The answer is visible from the bathroom door.

This week, walk your project facilities. Not to inspect them for compliance to experience them the way a worker experiences them. Ask whether what you find there reflects the standard of care you want applied to everything else on the project. If the answer is no, that is Monday’s first priority.

As Jason Schroeder says, “We’re building people who build things.”

On we go.

Frequently Asked Questions

Why does bathroom quality matter so much on a construction project?
Because it is the most direct signal of how leadership values the workforce. Workers read the environment they are given. Clean, dignified facilities communicate respect and set the standard for how workers treat the building. Neglected facilities communicate indifference and the project culture reflects that back immediately.

What if the PM did not budget for better restrooms?
The budget objection does not hold up against the cost of a disengaged workforce. The investment in decent facilities is small compared to the cost of vandalism, low morale, disengagement, and a site that never achieves total participation. This is a leadership decision, not a budget decision.

How does this connect to Lean implementation?
Lean begins with respect for people. Without it, no Lean tool, system, or methodology will take root. The bathroom is the most immediate, visible test of whether that respect is real or theoretical. Paul Akers taught that if you want to start with Lean, start in the bathroom and every project that has taken that seriously has proven him right.

If you want to learn more we have:

-Takt Virtual Training: (Click here)
-Check out our Youtube channel for more info: (Click here) 
-Listen to the Elevate Construction podcast: (Click here) 
-Check out our training programs and certifications: (Click here)
-The Takt Book: (Click here)

Discover Jason’s Expertise:

Meet Jason Schroeder, the driving force behind Elevate Construction IST. As the company’s owner and principal consultant, he’s dedicated to taking construction to new heights. With a wealth of industry experience, he’s crafted the Field Engineer Boot Camp and Superintendent Boot Camp – intensive training programs engineered to cultivate top-tier leaders capable of steering their teams towards success. Jason’s vision? To expand his training initiatives across the nation, empowering construction firms to soar to unprecedented levels of excellence.
Posted in All

Pre-fabricated Duct Bank

Read 9 min

If Duct Bank Keeps Showing Up on the Critical Path, the System Needs a New Approach

Here’s the deal: cast-in-place duct bank is one of those scopes that looks manageable on the schedule until you’re actually running it. The form work. The rebar. The conduit spacing. The concrete placement. The curing time. The stripping. And then the wait because nothing else can happen in that zone until the curing is done, and curing does not negotiate with your Takt time. The duct bank sits there, controlling the sequence around it, holding up the train while the schedule absorbs the hit and the team figures out what to do next.

Most project teams treat it as a fixed constraint. It takes what it takes. You plan around it, buffer it, and hope the curing schedule holds. The best teams ask a different question: does this have to happen on site at all?

What the On-Site Process Is Actually Costing

Cast-in-place duct bank on a construction site is an eleven-step field operation happening in an environment that was not designed for controlled manufacturing. The formwork setup requires precision in conditions that are anything but controlled. Concrete placement and vibration happen alongside active construction traffic. Curing requires time that the production plan cannot shrink regardless of how much schedule pressure exists. And throughout the entire sequence, the crew executing it is consuming critical path time that could have been spent on installation rather than manufacturing.

Add up the crew hours in formwork, rebar, conduit spacing, concrete placement, curing management, and form stripping. Then add the site real estate the operation consumes during the process. Then add the quality variation that comes from field pours compared to controlled yard conditions vibration from nearby construction, inconsistent curing in varying weather, formwork that’s been repaired three times. The on-site duct bank process is not just slow. It’s variable. And variability is what breaks production rhythms.

Jason Schroeder teaches that procurement feeds production and the supply chain must be zoned to match the production plan. When a manufacturing process that can be controlled offsite is instead happening in the zone consuming space, crew capacity, and schedule it is waste embedded in the critical path. The system was designed that way by default. It doesn’t have to stay that way.

A Story About What a Schedule Bottleneck Actually Costs

I was part of a team on a large data center project where duct bank was running through a critical sequence of the civil scope. The cast-in-place approach was what had always been used on similar projects, so nobody questioned it going in. Within the first three weeks, it was clear the curing windows were compressing the sequence downstream. Two trades were delayed waiting for zones to clear. The buffer we had built into that phase was consumed entirely by the duct bank sequence. By week five, the team was in recovery mode on a scope that should have been straightforward.

What we needed was a manufactured product that showed up ready to install. What we had was a field manufacturing operation on the critical path. The design of the supply chain had failed the production plan not because anyone made a bad decision, but because nobody had asked whether there was a better system.

What Pre-Fabricated Duct Bank Actually Is

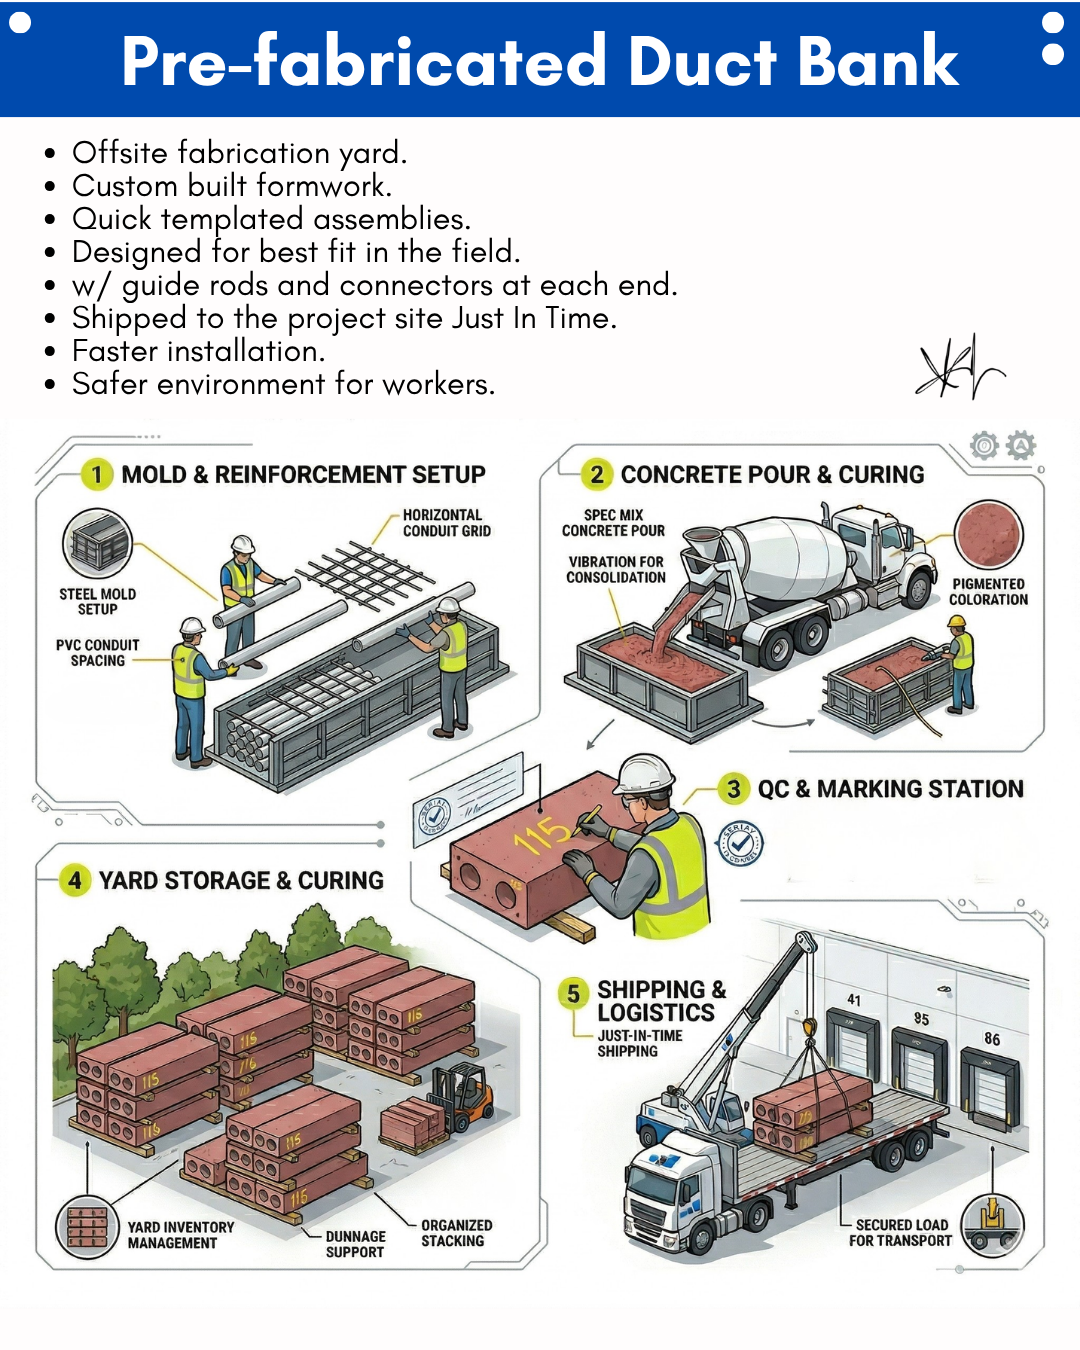
Pre-fabricated duct bank is exactly what it sounds like: duct bank sections manufactured in a controlled offsite fabrication yard using steel molds, spec mix concrete, and precision conduit spacing and then delivered to the project site just in time for installation. The image in this post shows the five-step process clearly.

Step one is mold and reinforcement setup at the fabrication yard. Steel mold forms hold the PVC conduit spacing in a horizontal conduit grid, creating a consistent geometry that is repeated precisely across every section. The mold controls the tolerances. The conduit spacing is set by template, not by field measurement. Every section that comes out of this mold is identical to the one before it. This is Poka-Yoke applied to concrete manufacturing the form physically prevents the wrong conduit spacing from being cast in, so variation is designed out before the pour happens.

Step two is the concrete pour and curing. Spec mix concrete is placed under controlled conditions, vibrated for consolidation, and pigment-colored for identification. The curing happens in the yard not in the zone, not on the critical path, not consuming field crew time and site real estate. The concrete cures while the project’s production work continues uninterrupted. That parallel activity is the core schedule advantage of prefabrication: the manufacturing time does not consume installation time.

Watch for these signals that duct bank is functioning as a production bottleneck on your project:

  • Duct bank curing windows are holding up trades in adjacent or downstream zones
  • The field crew executing duct bank could otherwise be advancing critical installation scope
  • Site real estate consumed by duct bank forms and curing areas is limiting logistics flow
  • Quality variation between sections is requiring remediation before the next scope can proceed
  • Schedule compression is forcing curing times shorter than specification requires

Step Three Through Five: Quality Control, Storage, and Just-In-Time Delivery

The QC and marking station in the yard is where each section is inspected and numbered before it leaves the facility. This is quality verification at the point of manufacture not at the point of installation where fixing a defect requires a field repair in an active construction zone. Every section that passes QC is marked with its sequence number so installation sequencing in the field is unambiguous. The crew setting sections doesn’t make decisions about what goes where. The marking communicates it.

Yard storage and curing uses organized stacking with dunnage support and yard inventory management to maintain section integrity during storage. Sections are ready when the production plan requires them not staged on site weeks early consuming staging area and creating coordination obstacles for other trades. Just-in-time delivery means the truck arrives at the site when the zone is ready to receive, not before and not after. The sections come off the truck, go into position, and installation begins.

The guide rods and connectors at each end of every section make field alignment fast and precise. Two sections brought together reference the guide rod geometry rather than requiring field measurement and adjustment. The alignment is built into the product. The installation crew spends their time setting sections, not solving geometry problems on the jobsite. This is what designing to the work package looks like in practice the manufacturing decision was made upstream to make the installation work easier and faster downstream.

Why This Is a Lean Question, Not Just a Concrete Question

Jason Schroeder teaches that leveraging prefabrication and modularization is one of the two major ways to speed up a project the other being proper zoning. When scope that can be manufactured in a controlled environment is instead manufactured in the field, the project absorbs all the variation that field manufacturing produces weather, congestion, crew interruption, quality variability as schedule loss that compounding affects every trade behind it in the Takt sequence.

The pre-fabricated duct bank eliminates that variation at the source. The product is manufactured to consistent tolerances in a controlled yard. It arrives in a condition verified by a QC station that has better inspection conditions than any active construction site. And it installs in a fraction of the time of the cast-in-place approach because the manufacturing work is already done. Less waiting. Less rework. Less congestion. The critical path shortens not because the team pushed harder, but because the work was designed better upstream.

If your project needs superintendent coaching, project support, or leadership development, Elevate Construction can help your field teams stabilize, schedule, and flow. Prefabrication is one of the most practical tools available to shorten schedule duration, and the conversation starts in preconstruction before the critical path is already locked.

Ask the Question Before the Scope Is Locked

Here is the challenge. On your next civil or MEP project with significant duct bank scope, bring pre-fabricated duct bank into the preconstruction conversation before the schedule is built around the cast-in-place assumption. Ask the fabricator what lead time looks like, what the delivery schedule requires, and what the cost comparison is when you factor in crew hours, site congestion, curing time, and quality management on the cast-in-place approach.

The answer will almost always reveal that the on-site manufacturing cost, when fully accounted for, is not far from the prefabricated cost and the schedule advantage of pulling that work offsite is significant. Design to the work package. Move the manufacturing out of the zone. Let the production plan run without a concrete curing window on the critical path.

Taiichi Ohno taught that the most dangerous waste is the waste you cannot see. The cast-in-place duct bank bottleneck is hiding in plain sight on every project schedule that treats it as a fixed constraint. It doesn’t have to be fixed. It can be solved in the fab yard, before the project even starts.

On we go.

Frequently Asked Questions

What is pre-fabricated duct bank and how is it different from cast-in-place?
It’s duct bank manufactured offsite in a controlled fabrication yard using steel molds and spec mix concrete, then delivered just in time for installation. Cast-in-place happens in the field and consumes critical path time for forming, pouring, and curing.

How does prefabrication eliminate schedule bottlenecks caused by duct bank?
Curing happens in the yard while field production continues. The manufacturing time does not consume installation time the two activities run in parallel rather than in sequence, which is the direct source of the schedule advantage.

What does the QC and marking station in the yard accomplish?
It verifies each section before it leaves the facility and marks sequence numbers for field installation. Quality defects are caught in a controlled environment rather than discovered at the point of install where correction is far more expensive.

If you want to learn more we have:

-Takt Virtual Training: (Click here)
-Check out our Youtube channel for more info: (Click here) 
-Listen to the Elevate Construction podcast: (Click here) 
-Check out our training programs and certifications: (Click here)
-The Takt Book: (Click here)

Discover Jason’s Expertise:

Meet Jason Schroeder, the driving force behind Elevate Construction IST. As the company’s owner and principal consultant, he’s dedicated to taking construction to new heights. With a wealth of industry experience, he’s crafted the Field Engineer Boot Camp and Superintendent Boot Camp – intensive training programs engineered to cultivate top-tier leaders capable of steering their teams towards success. Jason’s vision? To expand his training initiatives across the nation, empowering construction firms to soar to unprecedented levels of excellence.
Posted in All

Lean Leader’s Desk

Read 10 min

Your Workspace Is Either Working for You or Working Against You

Here’s the deal: I have worked in chaotic job site trailers and purpose-built Lean workstations, and the difference in what comes out of each one is not even close. The chaotic trailer produces reactive leadership. Papers get lost. Screens are too few to hold the whole picture at once. The desk is covered in layers of things that should have been filed, discarded, or acted on three days ago. And the leader sitting in it is spending energy managing the clutter before they can manage the project.

The Lean workstation produces something different. The leader who walks in, sits down, and has immediate access to the BIM model, the schedule, the field documents, the printed plan set, and the whiteboard where the day’s critical thinking is already mapped out that leader starts working in seconds. No context switching. No searching. No excuse not to be ready for every conversation that walks through the door. The workspace does not make the leader. But it either multiplies their capacity or diminishes it from the moment they arrive.

What the Chaotic Trailer Actually Produces

Jason Schroeder teaches something that is uncomfortable to sit with the first time you hear it: you cannot take a superintendent with a dirty desk, a disorganized truck, and a cluttered workspace and expect them to run a clean, safe, organized project with hundreds of workers, multiple trade partners, and a tight schedule. Whatever you have in the mind will be physically manifest on the project. The desk and the project are mirrors of each other.

This is not a character judgment. It is a system diagnosis. A superintendent who has never been given a standard for their workspace has never had the opportunity to build the mental clarity that a 5S’d environment creates. They are not failing the system never set them up to succeed. And when the workspace reflects chaos, the project team that walks into that trailer absorbs the chaos before a single decision is made. The tone is set by the environment before anyone opens their mouth.

I remember walking into a project trailer on a large healthcare project where the lead superintendent’s desk had three layers of unsorted submittals, two monitors showing the same thing, plans spread across the full table surface with no organized system, and a whiteboard so covered with outdated notes it hadn’t been updated in two weeks. The superintendent was sharp and experienced. But every conversation in that trailer started with someone searching for something. Every decision got made in the gaps between finding the information needed to make it. The trailer was costing the team time before the workday even reached the field.

What the Lean Leader’s Desk Is Built Around

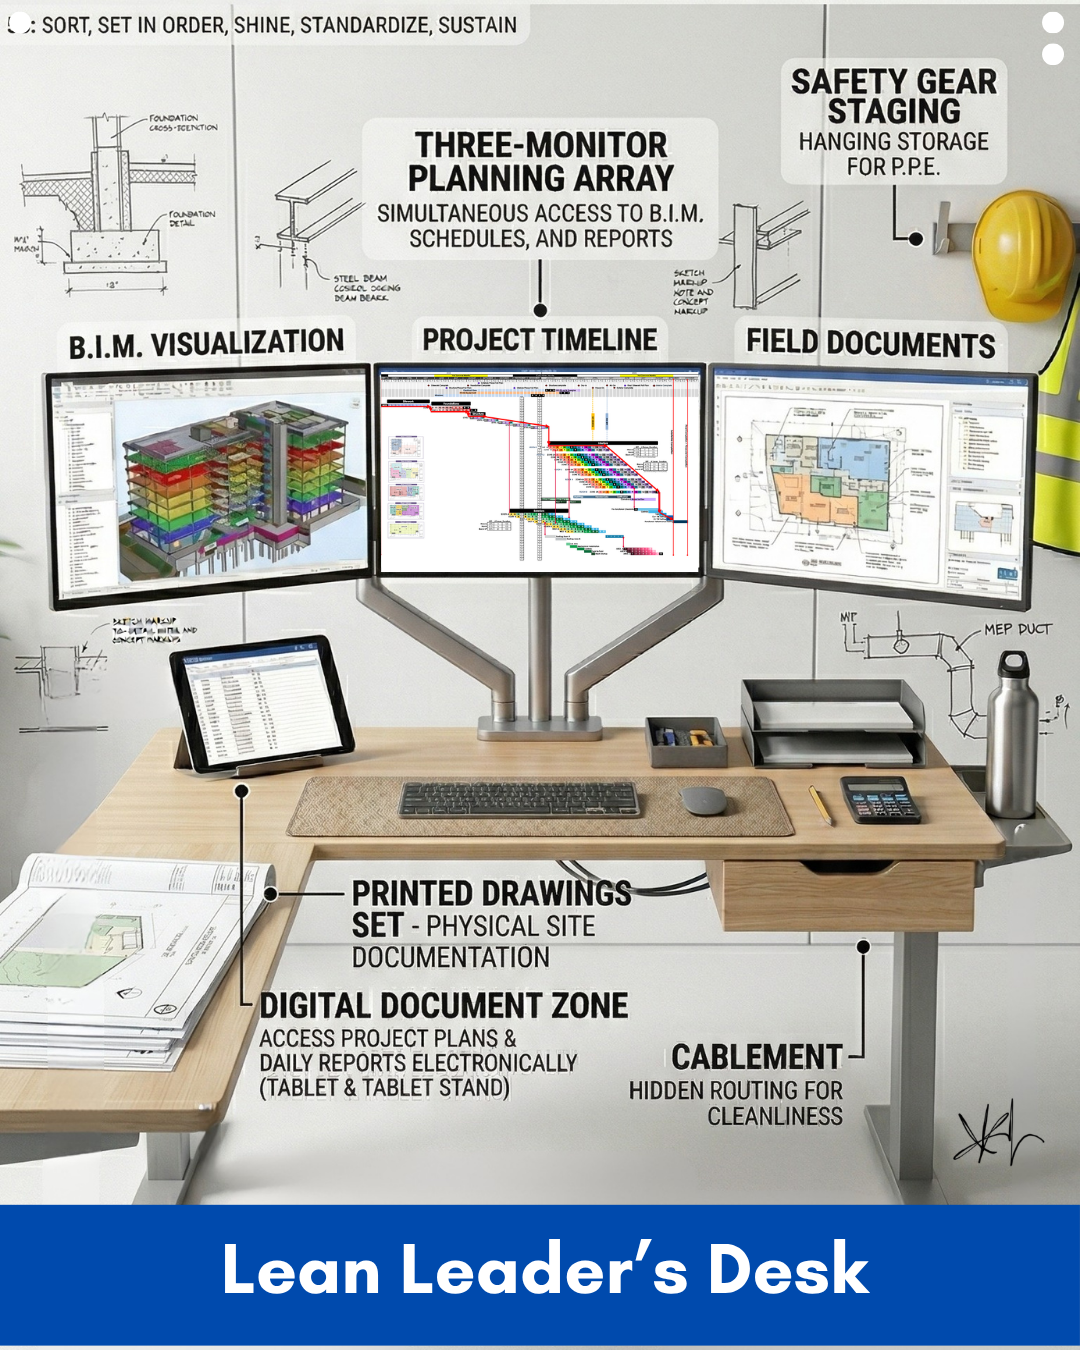
The image in this post shows what a workspace looks like when it’s designed with the same intention applied to the gang box, the staging yard, and the morning huddle intentionally, visually, and with the work it enables firmly in mind.

The three-monitor planning array is the operational center. One screen carries the BIM model for spatial visualization and coordination review. The center screen holds the project timeline schedule, Takt plan, or look-ahead for real-time production reference. The third screen holds field documents: submittals, RFIs, daily reports, and inspection records. All three are visible simultaneously. This is not a luxury. It is a seeing system. Jason Schroeder teaches that every good tool used to manage a project is a seeing system. Multiple screens mean the leader can see the whole picture at once rather than toggling between windows and losing context with every switch.

The printed drawings set on the left side of the desk is physical documentation that stays current. When a subcontractor foreman walks into the trailer with a coordination question, the super is not fumbling to find the right drawing or waiting for a file to load. The set is organized, accessible, and within arm’s reach. That five-second difference having the plan in hand before the conversation starts rather than after changes the quality of the conversation and the confidence with which the decision gets made.

Watch for these signals that a project leader’s workspace is costing the project rather than supporting it:

  • Leaders arriving at the desk and spending the first fifteen minutes locating documents needed for the morning meeting
  • Submittals, RFIs, and daily reports spread across the desk surface with no organized filing system
  • A single monitor requiring constant toggling between the BIM model, schedule, and field documents
  • No whiteboard or designated visual thinking space, meaning planning stays in email and conversation rather than becoming visible
  • PPE not staged at the workstation, requiring the leader to locate gear before every field walk

The Digital Document Zone and Cable Management

The tablet and tablet stand create a dedicated digital document zone a designated spot for accessing project plans and daily reports electronically that is always in the same place and always ready to use. This is Set in Order applied to the desk: every tool has a home, every tool is accessible without searching, and the desk surface itself is clear enough to work on.

Cable management is routed hidden through the desk structure, keeping the surface clean and organized. This is not an aesthetic preference. Cord clutter on a desk creates the same friction as cord clutter on the floor it signals disorder, slows access to equipment, and adds visual noise that competes with the information the leader is trying to process. A clean desk surface is a clean thinking surface. The physical environment shapes the mental environment, and the mental environment shapes every decision that comes out of it.

Safety gear staging hardhat and vest hung at the workstation means the leader is never fumbling for PPE before a field walk. The gear is in the same place every time. The transition from desk to field takes seconds rather than the low-level searching that compounds across every site visit over a six-month project.

The Sit-Stand Desk and What It Signals

The sit-stand desk is a non-negotiable on long project days. A superintendent or project manager who sits for ten straight hours does not arrive at the afternoon coordinator meeting with the same clarity they had at the morning huddle. Physical position directly affects cognitive performance, and construction leaders are making decisions that affect schedules, budgets, safety, and people’s livelihoods every hour of every day. A desk that supports movement is not a wellness choice disconnected from production it is a tool for sustained cognitive performance in a role that demands it from mobilization to closeout.

The whiteboards on the wall complete the system. Ideas should not live in someone’s head or buried in an email thread. They should be visible, sketchable, revisable, and shared. A whiteboard is where a coordination conflict gets mapped. Where a zone transition gets sequenced. Where the afternoon foreman huddle agenda gets built. A blank wall is the cheapest collaboration tool a leader can install, and it produces more useful planning output than any software subscription on the market when the person standing at it knows what they’re solving for.

Why This Is a Lean Question, Not a Comfort Question

The Lean Leader’s Desk is not about making the trailer nicer. It is about applying the same discipline to the leader’s workspace that the leader is responsible for applying everywhere else on the project. 5S the desk the same way you 5S the field. If you are holding foremen to a gang box standard with shadow boards and labeled bins, your own desk should be held to the same standard. If you are requiring trade partners to maintain organized staging areas with designated zones and clear access paths, your own workspace should meet that standard too.

Culture is shaped by the worst behavior the leader is willing to tolerate and the leader’s own behavior is the most visible example on the project. When the superintendent’s desk is organized, current, and fully equipped, it communicates the same thing that a clean gang box communicates to the crew: we take this seriously, and that standard applies everywhere, starting with us. If your project needs superintendent coaching, project support, or leadership development, Elevate Construction can help your field teams stabilize, schedule, and flow. That starts with the leaders who run the work and the workspace they use to run it from.

5S the Desk Before the Project Starts

Here is the challenge. Before the next project mobilizes or this week if the project is already running walk into the job site trailer and apply 5S to the leadership workspace. Sort: remove everything that doesn’t belong. Set in Order: give every document, every tool, every piece of PPE a labeled home. Shine: clean the surface and commit to ending every day with it returned to the standard. Standardize: decide what the desk should look like and hold to it. Sustain: make it a daily habit the same way crews do morning 5S in their zones.

Then add the three-monitor array. Mount the whiteboard. Set up the tablet stand. Route the cables. Stage the PPE. Organize the printed plan set on the left side.

Do that before the first trade mobilizes and see how different the conversations in that trailer feel from day one.

As Jason Schroeder teaches: “A clean, controlled environment reveals problems early and prevents hidden waste from compounding.” Build the workspace that makes you the leader your project needs from the first morning huddle to the final punch walk.

On we go.

Frequently Asked Questions

How does the sit-stand desk connect to project performance?
Physical position directly affects cognitive clarity over a long day. A leader who can shift position stays sharper through the full range of morning meetings, coordination calls, and afternoon field walks.

Why is the printed plan set on the left side non-negotiable?
Because when a foreman or trade walks in with a question, the super needs to respond with the plan in hand in seconds not waiting for a file to load. Physical access to current drawings is a decision-making tool, not a backup.

How does a Lean desk workspace connect to project culture?
If leadership holds the field to a 5S standard but operates from a chaotic desk, the standard is visibly hollow. A 5S’d workspace communicates that the discipline starts with the leader which is the only place it ever credibly starts.

If you want to learn more we have:

-Takt Virtual Training: (Click here)
-Check out our Youtube channel for more info: (Click here) 
-Listen to the Elevate Construction podcast: (Click here) 
-Check out our training programs and certifications: (Click here)
-The Takt Book: (Click here)

Discover Jason’s Expertise:

Meet Jason Schroeder, the driving force behind Elevate Construction IST. As the company’s owner and principal consultant, he’s dedicated to taking construction to new heights. With a wealth of industry experience, he’s crafted the Field Engineer Boot Camp and Superintendent Boot Camp – intensive training programs engineered to cultivate top-tier leaders capable of steering their teams towards success. Jason’s vision? To expand his training initiatives across the nation, empowering construction firms to soar to unprecedented levels of excellence.
Posted in All

Does Jobsite Safety Really Slow Your Crew Down?

Read 8 min

Is Safety Slowing Your Crew Down?

Here is the honest answer: yes. Safety slows crews down. And that is a good thing.

If that sounds wrong, it is worth asking why. Because the discomfort with that statement reveals something important a deeply embedded belief that speed is the goal and that anything slowing us down is the enemy. That belief is one of the most expensive ideas in construction.

The Industry Needs to Slow Down

The two biggest problems in construction are disrespecting people and pushing. Those two things are connected. When a team is in push mode just get it off the truck, just push through the problem, we will figure it out later it is not just the schedule that suffers. People suffer. Safety suffers. Quality suffers. Families eventually feel it at home.

The construction industry does not need to go faster. It needs to go smarter. It needs a one-thirds to two-thirds ratio, at minimum, between planning and execution. That means for every unit of time spent executing, at least half that much time should have been spent preparing. When that ratio flips when teams spend all their time executing and none of it planning the result is reactive, unsafe, chaotic work. Not because the crews are incapable. Because the system sent them in unprepared.

Safety is not a tax on productivity. Safety is the proof that preparation happened.

Stop, Call, Figure It Out

One of the most important habits a crew can build is the discipline to stop when something looks wrong, smells wrong, feels wrong, or sounds wrong. Not push through it. Not assume it will be fine. Stop. Pull the andon. Call the team together. Figure it out before moving forward.

This is the construction version of the same principle that runs the best manufacturing floors in the world. In Toyota plants, any worker can pull the andon cord and stop the entire production line. Not as a punishment. Not as a failure. As a system response to a signal that something is not right. Passing defects downstream is always more expensive than stopping to fix them at the source. Paul Akers documented that rework costs a minimum of eight times the original cost and probably closer to a hundred.

On a construction site, the math is even more direct. Ten minutes for a crew to pause, assess, and get it right versus an accident. There is no version of that comparison where pushing through wins. And beyond the math is the reality that we are talking about a human life. There is no schedule worth that.

What Slowing Down Actually Enables

Slowing down for safety is not the same as working slowly. The Navy SEAL principle slow is smooth, smooth is fast captures exactly what happens when teams build the discipline to ease into work properly. When a crew takes the time to pause, confirm the plan, check their conditions, do a point-and-call to confirm readiness, and then execute they do not have to stop for accidents. They do not have to stop for rework. They do not have to stop for the cascade of problems that comes from pushing into unready conditions.

The speed comes from the smoothness. The smoothness comes from the discipline. And the discipline comes from leaders who refuse to let their teams be pressured into skipping the preparation that makes safe, quality work possible.

Slowing down to be organized, to clean the site, to do proper safety planning, to train the crew before a new task these are not delays. They are the investment that prevents far more costly stops later. A clean site surfaces hazards before they become incidents. An organized site means crews are not on treasure hunts when they should be executing. A trained crew makes fewer mistakes and catches more problems before they get built in.

Here are the conditions that slowing down creates on a well-run project:

  • Crews arrive to ready conditions full kit, clear plan, safe zone and execute without unnecessary stops
  • Problems are surfaced and solved upstream before they reach the field and compound
  • Rework drops because quality is built in at the source, not inspected for after the fact
  • Incidents decline because hazards are identified and eliminated before crews are exposed to them
  • The team builds trust in the system because the system consistently protects them

Safe, Clean, and Organized Is the Standard Not a Goal

This needs to be said directly: a superintendent who cannot keep a project safe, clean, and organized is not a superintendent. A foreman who cannot keep a crew safe, clean, and organized is not a foreman. There is no such thing as an unsafe crew that is a good crew. There is no such thing as an unsafe foreman who is a good foreman. These are not separable things.

Safety, cleanliness, and organization are not extra credit. They are the foundation. Everything else production, schedule, quality, trade partner relationships, team morale sits on top of that foundation. Remove the foundation and none of the rest holds up. A dirty, unsafe, disorganized site is not a site that is working hard. It is a site that has lost control.

The leaders worth promoting, worth hiring, and worth trusting are the ones who treat safe, clean, and organized as a non-negotiable standard not something to achieve when things calm down, but the baseline condition before anything else is allowed to happen.

If Safety Feels Like an Obstacle, That Is the Problem

If someone on a leadership team looks at safety requirements and their first reaction is frustration at the slowdown, that reaction is the signal to pay attention to. Not the safety. The reaction. It means the mental model underneath is still built around speed as the primary value and people as the variable adjusted to serve that value.

That model produces accidents. It produces rework. It produces burned-out crews. It produces projects that sprint into chaos and then spend the back half of the schedule scrambling to recover. And it produces the kind of environment where people go to work and are not certain they will go home the same way they arrived.

The mental model worth building is this: speed is a byproduct of preparation, not the opposite of it. When the site is safe, crews move with confidence. When the site is clean, hazards are visible and eliminated before anyone is exposed. When the site is organized, work flows without friction. Safety does not slow down a good project. Safety is what a good project looks like.

If your project needs superintendent coaching, project support, or leadership development, Elevate Construction can help your field teams stabilize, schedule, and flow.

The Leadership Question

Walk your project this week and ask whether your team has been trained and empowered to stop, call, and figure it out or whether the culture has quietly taught them to push through and hope for the best. Ask whether the ratio of planning to execution reflects the standard that keeps people safe. Ask whether the site is genuinely clean, safe, and organized, or whether that standard has been allowed to slide under production pressure.

The answer to those questions tells you more about the health of your project than any schedule report. And if the answers are not what they should be, the fix is not to push harder. It is to slow down, get it right, and build the system that protects your people every single day.

That is what leadership looks like. Not the fastest project. The safest one. And in the end, the safest projects are also the ones that finish on time, on budget, and with a team that would follow that leader again.

“The most dangerous kind of waste is the waste we do not recognize.”
— Shigeo Shingo

On we go.

Frequently Asked Questions

Does slowing down for safety really improve overall project speed?
Yes. The time invested in preparation, safety planning, and crew training prevents the far more costly stops caused by accidents, rework, and reactive problem-solving. Slow is smooth, and smooth is fast that principle holds on every well-run project.

What should a crew do when something looks or feels unsafe?
Stop. Call the team together. Figure it out before moving forward. Do not push through hoping it will be fine. The cost of pausing is always less than the cost of an incident or defect that gets built in and discovered later.

Is a superintendent who prioritizes safety slowing the project down?
No. A superintendent who cannot maintain a safe, clean, and organized site has already lost control of the project. Safety is not separate from production it is the foundation that makes consistent production possible.

If you want to learn more we have:

-Takt Virtual Training: (Click here)
-Check out our Youtube channel for more info: (Click here) 
-Listen to the Elevate Construction podcast: (Click here) 
-Check out our training programs and certifications: (Click here)
-The Takt Book: (Click here)

Discover Jason’s Expertise:

Meet Jason Schroeder, the driving force behind Elevate Construction IST. As the company’s owner and principal consultant, he’s dedicated to taking construction to new heights. With a wealth of industry experience, he’s crafted the Field Engineer Boot Camp and Superintendent Boot Camp – intensive training programs engineered to cultivate top-tier leaders capable of steering their teams towards success. Jason’s vision? To expand his training initiatives across the nation, empowering construction firms to soar to unprecedented levels of excellence.

Posted in All

Why Most Lean Construction Rollouts Fail?

Read 9 min

If Lean Is So Great, Why Do Most Lean Rollouts Fail?

It is one of the most honest questions in construction. You have seen the whiteboards. You have attended the trainings. You have read about Toyota and the principles that transformed an entire industry. And then you watched the rollout land flat on your project, your company, or your industry and wondered what went wrong.

The answer is not the tools. The tools work. The answer is the culture they were dropped into.

The System Lean Was Dropped Into

To understand why Lean fails in the West, you first have to understand the system that was already there. Classical business management the inherited Western approach that most companies operate from is built on a specific priority stack: profits first, control of people second, and protection of the internal leadership team. Not because the people running these companies are malicious. Because that is the model they were handed, the model their institutions reinforce, and the model that every financial incentive in the system rewards.

In the United States specifically, the legal and financial structures that surround business actively incentivize conflict over cooperation. Legal systems are built around adversarial processes dispute, claim, litigation. Financial institutions carry a fiduciary responsibility to shareholders, which most of the time comes at the expense of the actual people doing the work. Companies trying to implement Lean are trying to build a people-first culture inside a system that was architecturally designed to do the opposite.

That tension does not resolve itself by posting values on the wall or putting sticky notes on a pull plan.

What Lean Actually Prioritizes

A Lean company operates on a completely different priority stack. People first. Process second. Quality third. Profits are a condition of staying in business they matter but they are the result of getting the first three right, not the goal that drives daily decisions.

The question a Lean company asks is not “what maximizes profit this quarter?” It is “what is best for our people and our clients?” When that question drives decisions, the right business outcomes follow. When the question is flipped when profit drives first and people are the variable adjusted to protect margins Lean cannot root. The tools become decorations. The language becomes branding. And within two to three years, the initiative is quietly abandoned and the team goes back to the way things were.

This is not theory. It is a pattern that repeats itself across industry after industry, company after company, project after project.

Why Lean Works in Japan

To understand the gap, it helps to look at where Lean did root deeply, organically, and permanently. Japan’s production culture is not superior because of better tools or smarter engineers. It is rooted differently because the cultural foundation underneath the tools is different.

Japan’s Shinto and Buddhist traditions fundamentally value the individual as part of a whole. Working in total participation contributing to the group, not standing out as an individual hero is not a management concept there. It is a cultural default. The society was built around it. When Lean principles arrived in that environment, they found soil that was already prepared.

In North America, the cultural default runs the opposite direction. The educational system teaches people to sit down, receive instruction, and not disrupt the conveyor belt. The cultural mythology glorifies the lone cowboy the individual who goes their own way, rebels against the system, and wins through sheer will and personal grit. Total participation is the opposite of that ideal. Cooperation is culturally coded as weakness. Following a system feels like a loss of autonomy.

And then companies try to roll out Lean a system built entirely on total participation, group ownership, and process discipline into that cultural environment and wonder why it does not stick.

The Lean Definition That Changes Everything

Here is the definition of Lean that cuts through all of it: Lean is the willingness to learn and implement excellence for the benefit of people and humanity.

Read that again. It is not a production method. It is not a scheduling format. It is not a toolkit. It is a willingness a fundamental orientation toward learning, improvement, and people. Without that orientation, no Lean tool, trick, concept, or methodology will ever work. The andon cord without the culture behind it is just a cord. The pull plan without the respect behind it is just stickies on a board. The Takt plan without the commitment to total participation is just a pretty schedule.

This is why Lean fails. Not because the tools are wrong. Because the people deploying the tools never made it about people in the first place.

What the Failure Pattern Looks Like

When Lean rolls out without the cultural foundation, a predictable sequence follows. The tools get introduced but not embedded. Participation is voluntary, sporadic, and driven by whoever is most enthusiastic in the room. The first time production pressure builds, the Lean behaviors are the first things abandoned because they were never non-negotiable. Leaders revert to push and control because that is what the system underneath rewards. And people who tried to participate learn that the system was not actually safe for them to change, challenge, or improve.

The failure is not in the people who stopped participating. It is in the leadership that never built the conditions for real participation to exist.

Here are the conditions that make or break a Lean rollout:

  • Leaders who stand up for people, create standards, and enforce the system until it sticks
  • A cultural commitment to total participation not as an invitation, but as an expectation
  • Processes and environments designed to reduce burden on people, not extract more from them
  • One piece flow and focused work protecting people from being spread across too many things at once
  • The removal of fear so people can stop, call, and wait when something is wrong instead of pushing through

When these conditions are absent, Lean is a language being spoken without a shared grammar. Everyone nods. Nobody understands. Nothing changes.

The Role of Leadership

There is a balance that Lean leadership requires in Western culture that is easy to misread. Japan’s cultural foundation means that total participation happens organically, with relatively minimal authority required to sustain it. In North America, that organic pull does not exist in the same way. A gallon of influence and a teaspoon of authority that is the ratio. Heavy on earning trust, building relationships, and demonstrating that the system genuinely serves people. With enough authority to hold the standard when the pressure is on and the temptation to revert is highest.

Weak leadership is one of the primary reasons Lean fails. Not leaders who lack intelligence or effort, but leaders who are not willing to stand up for the people in the system, create clear standards, and protect the implementation until it becomes the culture not just the current initiative. Lean requires leaders who protect people from the classical management system that surrounds the organization, even as that system continues to exert pressure from the outside.

If your project needs superintendent coaching, project support, or leadership development, Elevate Construction can help your field teams stabilize, schedule, and flow.

What Makes It Work

The companies and projects where Lean actually works share one thing in common: somebody made it genuinely about people. Not as a talking point. Not as a company value written on a poster. As an operational commitment that shaped every decision how work was designed, how problems were solved, how people were treated when things went wrong, and whether the system existed to serve the people inside it or extract from them.

When that commitment is real, the tools work exactly as designed. Pull plans generate real conversation and real commitment. Takt plans create flow because the trades trust that the system is set up for them to succeed. Weekly work plans are honored because the culture treats missed commitments as learning opportunities, not punishments. Total participation happens because people feel safe enough and valued enough to actually participate.

That is what Lean is. And it has never failed when it was actually tried. The rollouts that fail are almost always rollouts of Lean without people tools deployed into a classical management system that was never restructured to support them. The solution is not better tools. The solution is the willingness to build something different from the ground up, starting with genuine respect for the people the system is supposed to serve.

As Jason Schroeder says, “Respect for people is not soft it’s a production strategy.”

On we go.

Frequently Asked Questions

Why do Lean tools fail even when teams are trained on them?
Because tools without culture are just methods. Lean requires a fundamental reorientation toward people first and when that reorientation has not happened at the leadership level, the tools get used superficially and abandoned under pressure.

Is Lean actually possible in Western construction culture?
Yes, but it requires intentional leadership. Western culture defaults toward individual performance and push-based management. Lean requires building total participation deliberately with a gallon of influence and a teaspoon of authority until the culture shifts.

What is the most important thing a leader can do to make Lean stick?
Stand up for people, create clear standards, and refuse to let the system revert under pressure. Lean takes root when leaders protect the implementation long enough for the results to become visible and the behaviors to become normal.

If you want to learn more we have:

-Takt Virtual Training: (Click here)
-Check out our Youtube channel for more info: (Click here) 
-Listen to the Elevate Construction podcast: (Click here) 
-Check out our training programs and certifications: (Click here)
-The Takt Book: (Click here)

Discover Jason’s Expertise:

Meet Jason Schroeder, the driving force behind Elevate Construction IST. As the company’s owner and principal consultant, he’s dedicated to taking construction to new heights. With a wealth of industry experience, he’s crafted the Field Engineer Boot Camp and Superintendent Boot Camp – intensive training programs engineered to cultivate top-tier leaders capable of steering their teams towards success. Jason’s vision? To expand his training initiatives across the nation, empowering construction firms to soar to unprecedented levels of excellence.

Posted in All