Logistics Is #1: How to Build a Site Logistics Plan

Read 4 min

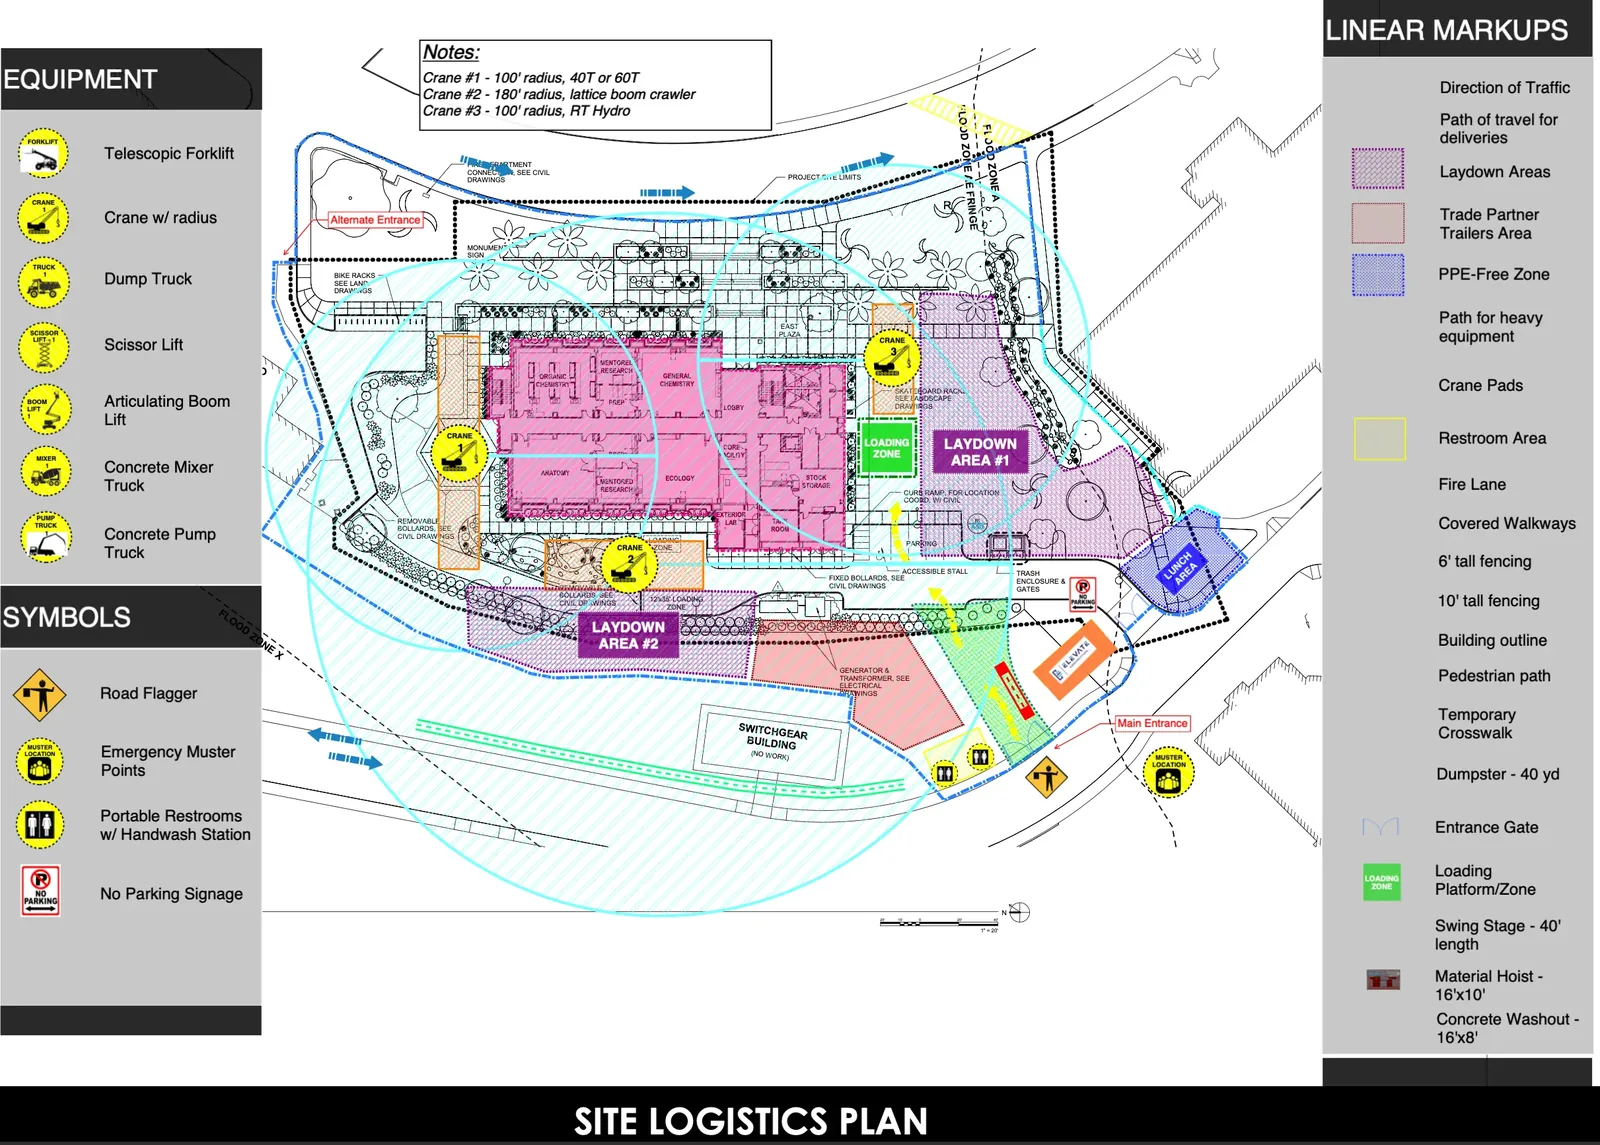
Short answer: A construction site logistics plan is a map of how people, materials and equipment move on your site: entrances, trailers, laydown, cranes and hoists, deliveries, traffic and emergency access. Update it often and use it for day planning, not just once at mobilization.

What is a site logistics plan?

Your Logistics Map cannot just be a map you create, post, and use one time. It is a strategic planning tool that will allow you to properly control your project. It should be intelligently designed, easy to follow, nice to look at, and kept up-to-date. Every good superintendent will utilize a system to control logistics in an intentional and remarkable way.

Example site logistics plan with crane, laydown and traffic routes

The key to production is not just the work, but effective material supplies to the work.

I remember that we began using a logistics plan for day planning at a pharmacy project where I worked. On the day plan maps, we would identify where materials were to be staged, where work was taking place, and then send that drawing to every worker in the field. Our forklift operator, crane operator, and foremen began using that map to control the site. It was remarkable to take a static plan and turn it into a daily planning tool.

What should a site logistics plan include?

Plan the appropriate items and visually communicate to control logistics with the other leaders on the project site. You will want to plan for the following things at a minimum:

  • Area control
  • Clear access ways
  • Trailer position and organization
  • General site configuration and design
  • Flow of deliveries
  • Traffic patterns
  • Pedestrian patterns
  • Site security
  • New utility construction
  • Equipment mobilization and demobilization
  • Loading platforms
  • Pumping
  • Slick lines and placing booms
  • The hoist
  • The crane
  • Equipment staging
  • Staging locations

Get help when creating your daily logistics plan. If you do this, you will begin the planning of your terrain, which has been a habit throughout centuries with the best generals in war.

What to decide first

Determine the following:

  • Flow of construction
  • Entrances to the jobsite (you really need two, if possible)
  • Trailer location (always get it off-site when possible, or out of the construction area)
  • Trade partner offices
  • Dumpster location
  • Temp restrooms (keep them grouped together, not spread out)
  • Material laydown
  • Fire lane
  • Temp water and temp power
  • Parking lots
  • Temp fence
  • Site organization
  • Site signage
  • Emergency gathering points
  • Disaster planning
  • Emergency personnel access and planning

If you want or need help with your logistics plan, talk to us about consulting, call 602.571.8987 or email jasons@elevateconstructionist.com.

Free logistics plan templates

Download our two free templates below (zip files): the Site Logistics Plan template (PDF) and the Logistics Planning template (the same PDF with its Bluebeam toolbox objects).

PLAN TEMPLATE:

PLAN TEMPLATE WITH TOOLBOX OBJECTS:

On we go!

FAQ

How often should you update a logistics plan?

Whenever the site changes, and ideally daily as a day-plan map that shows staging, work areas and deliveries.

How many site entrances do you need?

Two if at all possible, so deliveries and emergency access aren’t blocked by one choke point.

People Also Read:
Lean Logistics Explained: How to Make Jobsite Flow Actually Work

If you want to learn more we have:

-Takt Virtual Training: (Takt Virtual Training)
-Check out our YouTube channel for more info: (Elevate Construction on YouTube)
-Listen to the Elevate Construction podcast: (Elevate Construction Podcast)
-Check out our training programs and certifications: (Training Programs and Certifications)
-The Takt Book: (The Takt Book on Amazon)

Discover Jason’s Expertise:

Meet Jason Schroeder, the driving force behind Elevate Construction. As the company’s Founder and COO, he’s dedicated to taking construction to new heights. With a wealth of industry experience, he’s crafted the Field Engineer Boot Camp and Superintendent Boot Camp – intensive training programs engineered to cultivate top-tier leaders capable of steering their teams towards success. Jason’s vision? To expand his training initiatives across the nation, empowering construction firms to soar to unprecedented levels of excellence.

Posted in All

Creating a Takt Plan

Read 12 min

Short answer: To create a Takt plan, set your start and end dates, study the drawings, find the flow, size preliminary Takt zones and a Takt time, pull plan one representative zone, package the work into Takt wagons, copy the train across all zones, optimize with (wagons + zones – 1) x Takt time, add buffers and verify with your trades.

What are the steps to create a Takt plan?

Probably one of the most useful outlines we can provide for Takt is the step by step outline for how to create one. We hope to help you visualize the process in this post. But first, here is the list of steps in summary:

· Identify your start and end date.

· Research your drawings.

· Identify the general flow of the project based on known constraints.

· Identify preliminary Takt zones.

· Identify preliminary Takt time.

· Pull plan a typical sequence to start.

· Create the Takt sequence.

· Create the Takt phase.

· Identify logistics flow.

· Optimize the throughput time with the Takt formula.

· Network phases together.

· Develop work steps.

· Trigger planning buffers in the system.

· Add buffers.

· Create standard work.

· Identify bottlenecks.

· Verify with trade partners.

· Create logistics plan/drawings.

· Create Takt zone maps.

· Perform a risk analysis.

· Create a Basis of Schedule (BOS).

· Align procurement.

· Review in a “fresh eyes” meeting.

· Create roadblock tracking maps.

· Track historical production.

· Add a TPNR (Takt Point of No Return).

One of the best ways to get into this system is to create your first Takt plan, so let’s get started. But first, we want to explain a few concepts of overall structure.

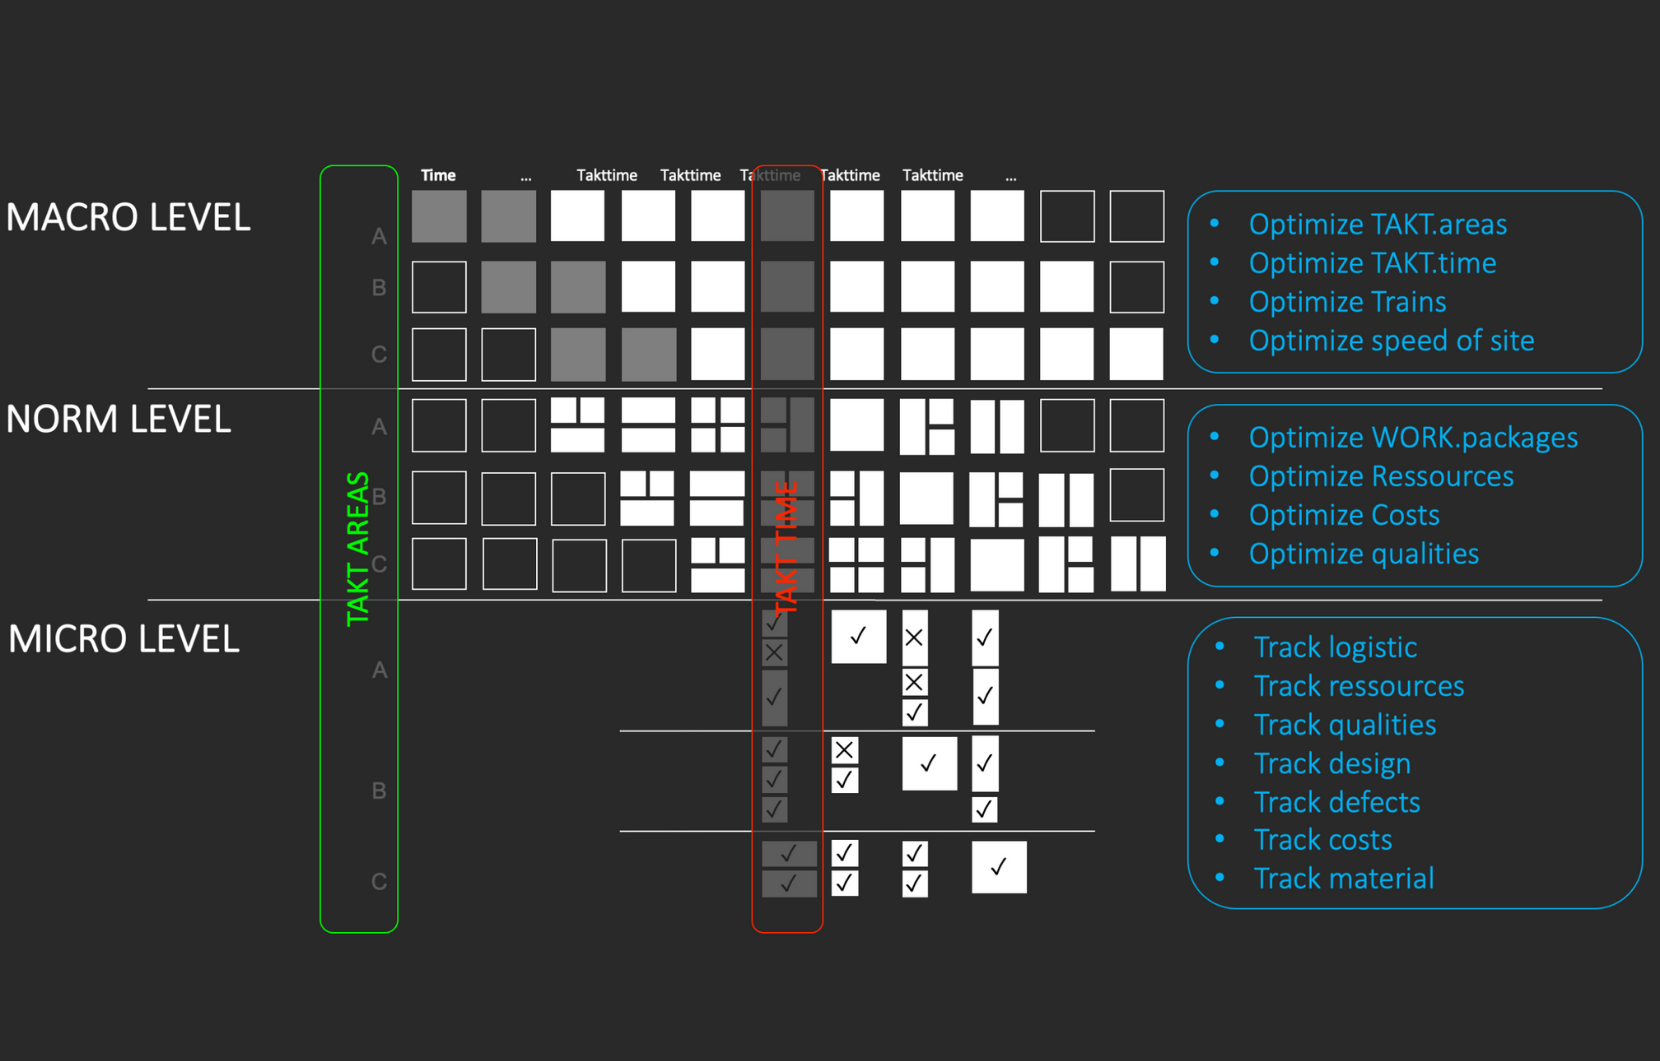
The three levels of Takt planning

● Macro level, the process analysis – In the macro-level, the overall Takt plan is created.

● Norm-level Takt planning – In the norm-level, the Takt plan harmonization takes place.

● Micro level – This level of Takt planning is crucial to the system and cannot be omitted. In this step, the management of Takt control takes place.

Slide of the three levels of Takt planning: macro level (Takt areas, time and trains), norm level (work packages, resources, costs) and micro level (tracking)

Identify Your Start and End Date

Some projects come with a stipulated start and end date. Some projects’ start and end dates need to be identified through your efforts of creating a Takt plan. To be successful in creating your plan, you will start here and know what constraints you have as you begin the planning process.

Research Your Drawings

This step may seem like a given, but it needs to be said. One of the strengths of Takt is that it gives our builders back the time they need to carry out the basics of a builder which means studying the drawings each day, forward planning in the schedule, and reflecting daily. As the builder studies the design and gets a feel for the flow, the sequence, and the general strategic approach for the project with others, he/she will immediately see and identify the flow of the project.

Identifying Flow

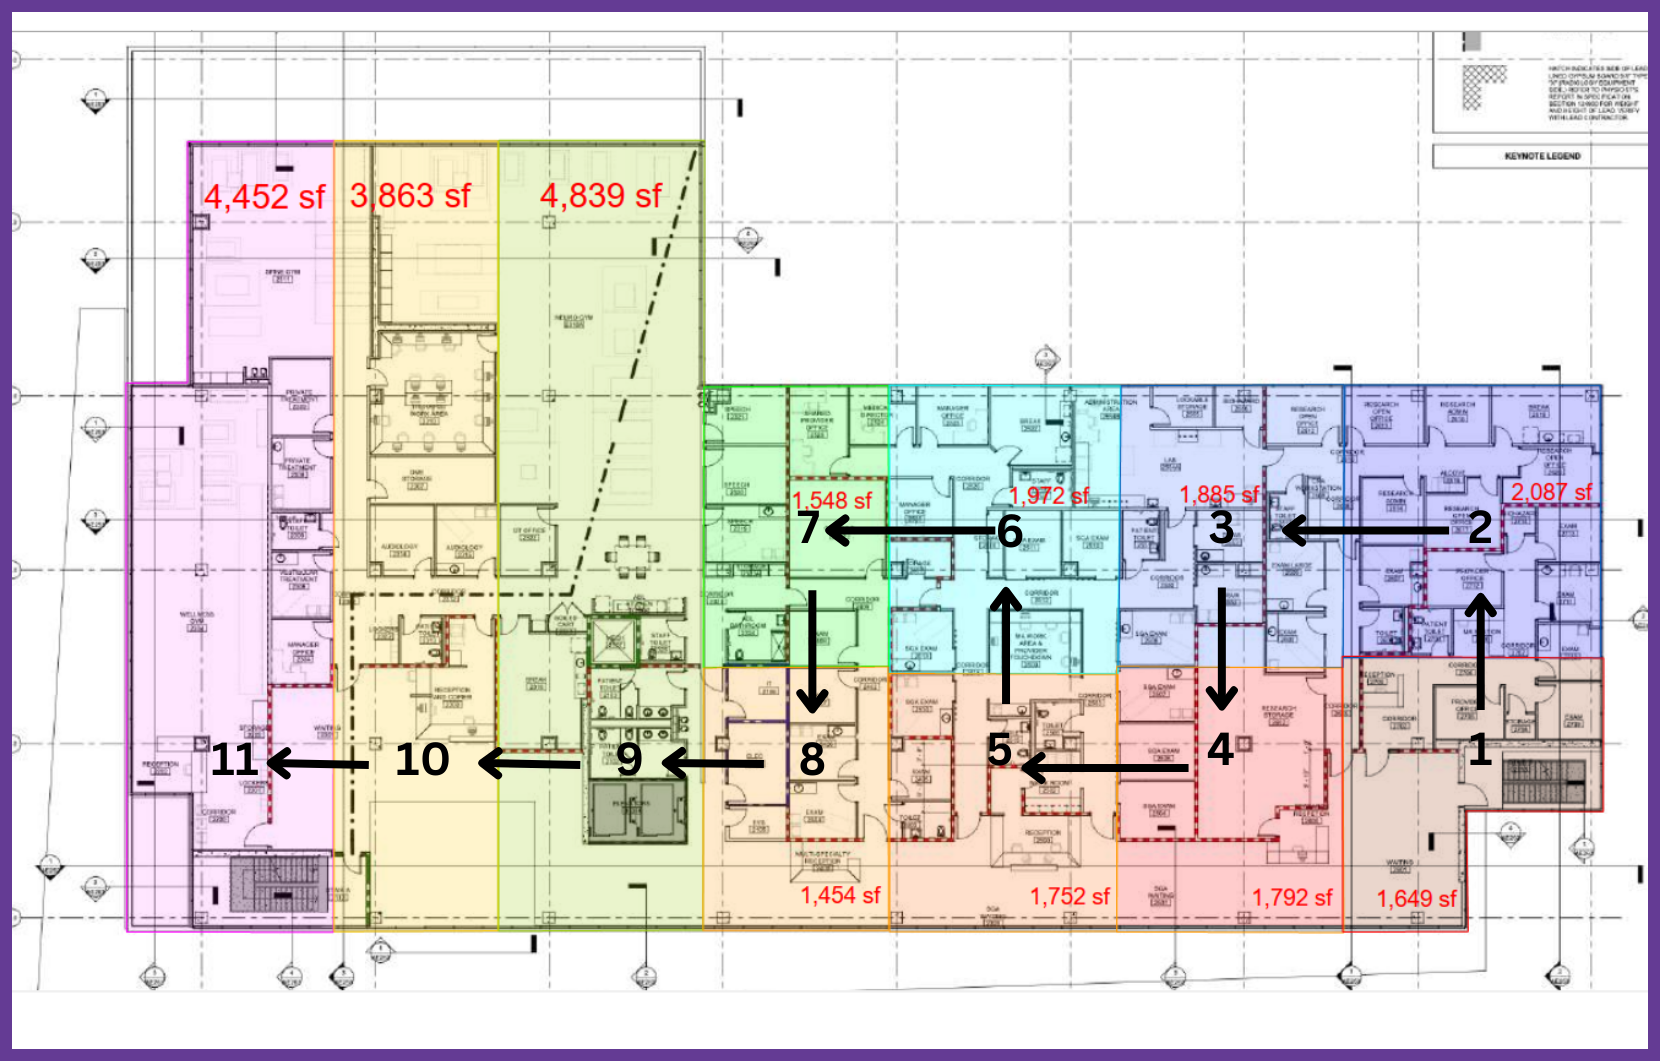
Builders can get a feel for the general flow of the project after digging into the drawings. Constraints like staging, material flow, material access, adjacent structures, hoisting, and project access will begin to form a picture of how the project will need to generally flow. Does the construction begin from east to west, or west to east? Does the interior run from top down or bottom up?

Floor plan split into 11 color-coded Takt zones with square footage and arrows showing the flow from zone 1 to zone 11

Identifying Preliminary Takt Zones

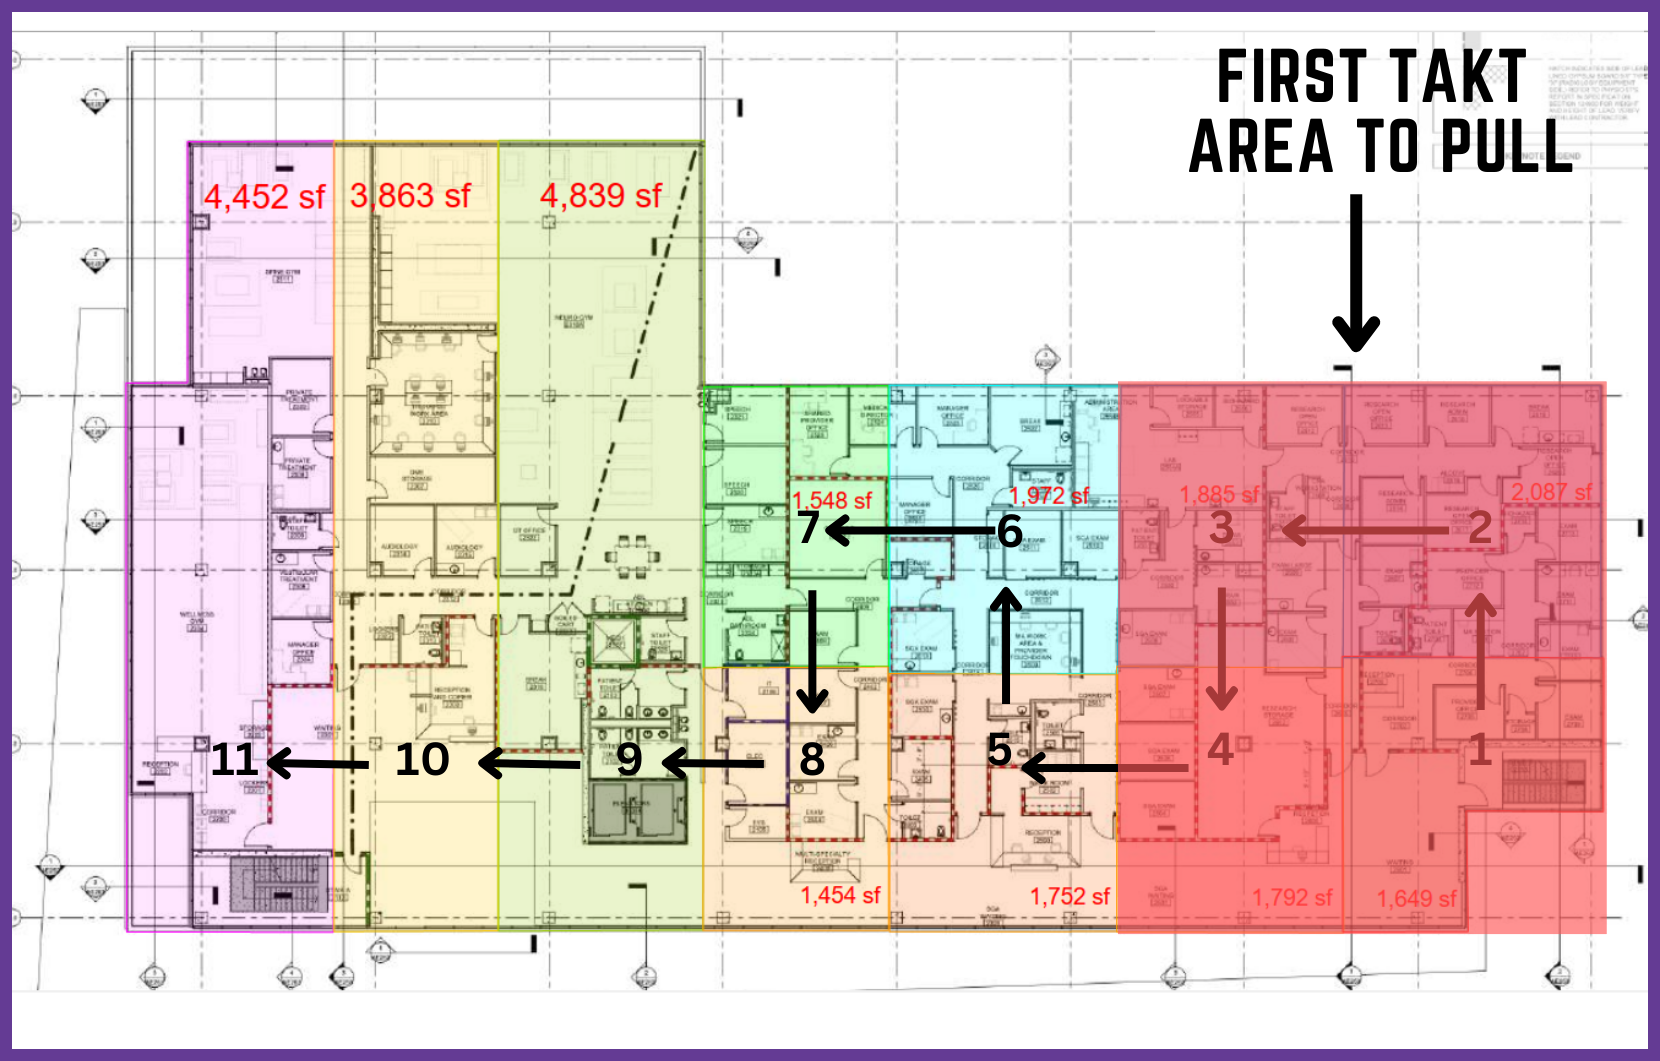
Takt zones, sometimes known as geographical areas, production areas, or sequences, are the areas defined within the phase to identify work that will be scheduled on a rhythm per the Takt time. To get portions of work broken down to fit within a drumbeat, we must break the work up into zones that can be completed according to that drumbeat. This is easy to do, especially if the first planners know the general direction of the flow and how much area can be completed within the Takt time. So, the first planners literally guessed (and yes, I said guessed) the right size areas needed to break up the floor, exterior, or general work area.

The same floor plan with the first Takt area to pull highlighted in red

Pull Plan the Representative Zone

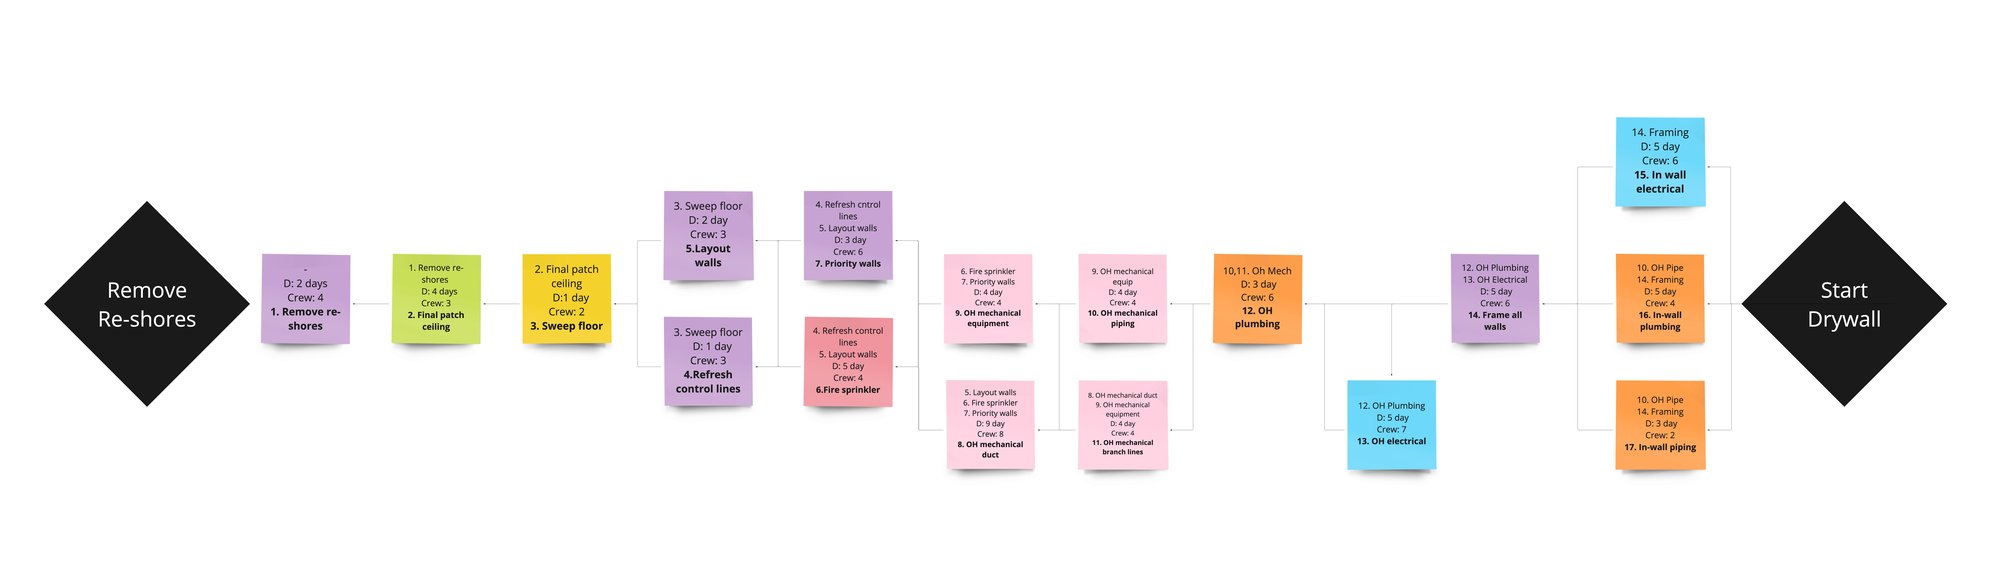
Now that we have a preliminary Takt zone size, we can outline the sequence of one representative Takt zone. Before you begin the pull plan, you may want to consider getting quantities for the representative area to better help trades visualize the commitments they are making.

The team will collaboratively pull the sequence inside the first representative Takt zone by following these steps:

  1. Ask trades to come prepared with their activities, tags, or Sticky Notes ahead of the meeting and to think about what each activity needs for them to begin.
  2. When opening the meeting establish the following:

1. The Time Frame

2. The trade colors

3. The Sticky Note format

4. The parking lot

5. The rules of the meeting—we recommend asking the group to make the rules of the pull plan together. Common rules teams list are:

1. No one touches each other’s tags

2. Make commitments to each other

3. Work from the milestone back

4. Turn the sticky to a diagonal if it has an unmet constraint

5. Sidebar non-pertinent conversations

6. Each trade will ask for the preceding tasks to be placed on the board

7. And so on…

  1. Begin building the sequence of the pull plan until there are no more predecessors or needed activities
  2. When the sequence is done, the team can work the plan forward to ensure it fits within the target duration and also to introduce parallelization of activities. The team will ensure the activity sequence is optimized.

Pull plan of one representative Takt zone, from removing re-shores to starting drywall, on color-coded sticky notes

Work Packaging & Leveling

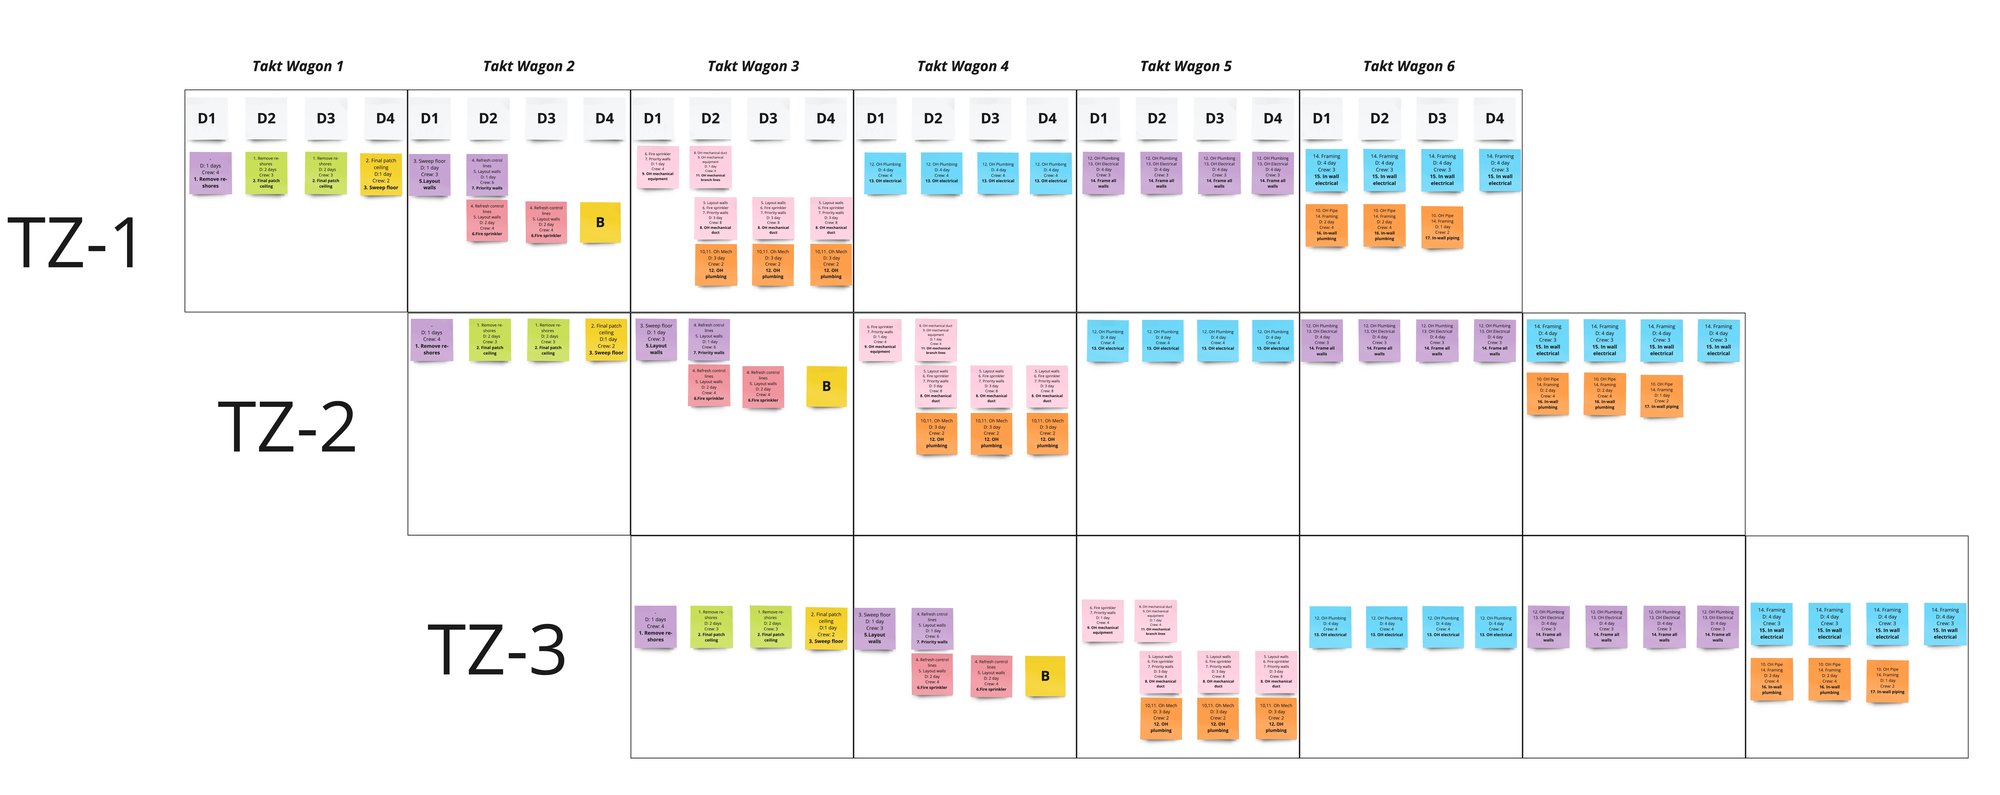
Once this is done and the first representative Takt zone is pulled, it is time to organize these into work packages and Takt wagons in a preliminary manner. When observing the sequence, it may become clear what average Takt time each activity fits within. The duration of each work package will inform you what Takt wagon it needs to fit within.

Takt wagons 1 to 6 laid out across Takt zones TZ-1, TZ-2 and TZ-3, with sticky notes for each day

Package Wagons into Takt Trains

A Takt sequence or Takt train is a sequence of Takt wagons. Each Takt wagon includes one or more work packages, and each work package contains multiple work steps. By this point, stickies from the pull plan sequence have become either a Takt wagon, a work package, or a work step depending on size and how it is packaged. Knowing how they translate comes from facilitation and experience but generally, if the activity was a large summary of a general scope of work that occurs by itself in a Takt time scale, it may become a Takt wagon. If it is a specific scope of work that summarizes steps that work in the same area as another scope, it would become a work package. If the activity was a detailed step as a part of a scope of work then it is likely a work step. For now, we need to know what Takt wagons will fit within our single representative Takt zone within one Takt time.

The current work steps or work packages should all be generally packaged within Takt wagons. This sequence or train is then placed in the Takt plan within the Takt time scale.

Build your Takt Phase

Now we need to show the relationship between the other Takt zones. This is where we copy the sequence down to other rows in the Takt phase at the right stagger. The stagger is important because the stagger between the start of each train may not follow only one Takt time. If there is a Takt time of 5 days, each train may not be offset from each other by 5 days. Rather, they may have a stagger of 10 days and use two Takt times between starts. Either way, we will copy these sequences down at the correct stagger. When you have completed this you will see if it generally fits within the overall project duration or phase duration, but only in a preliminary sense.

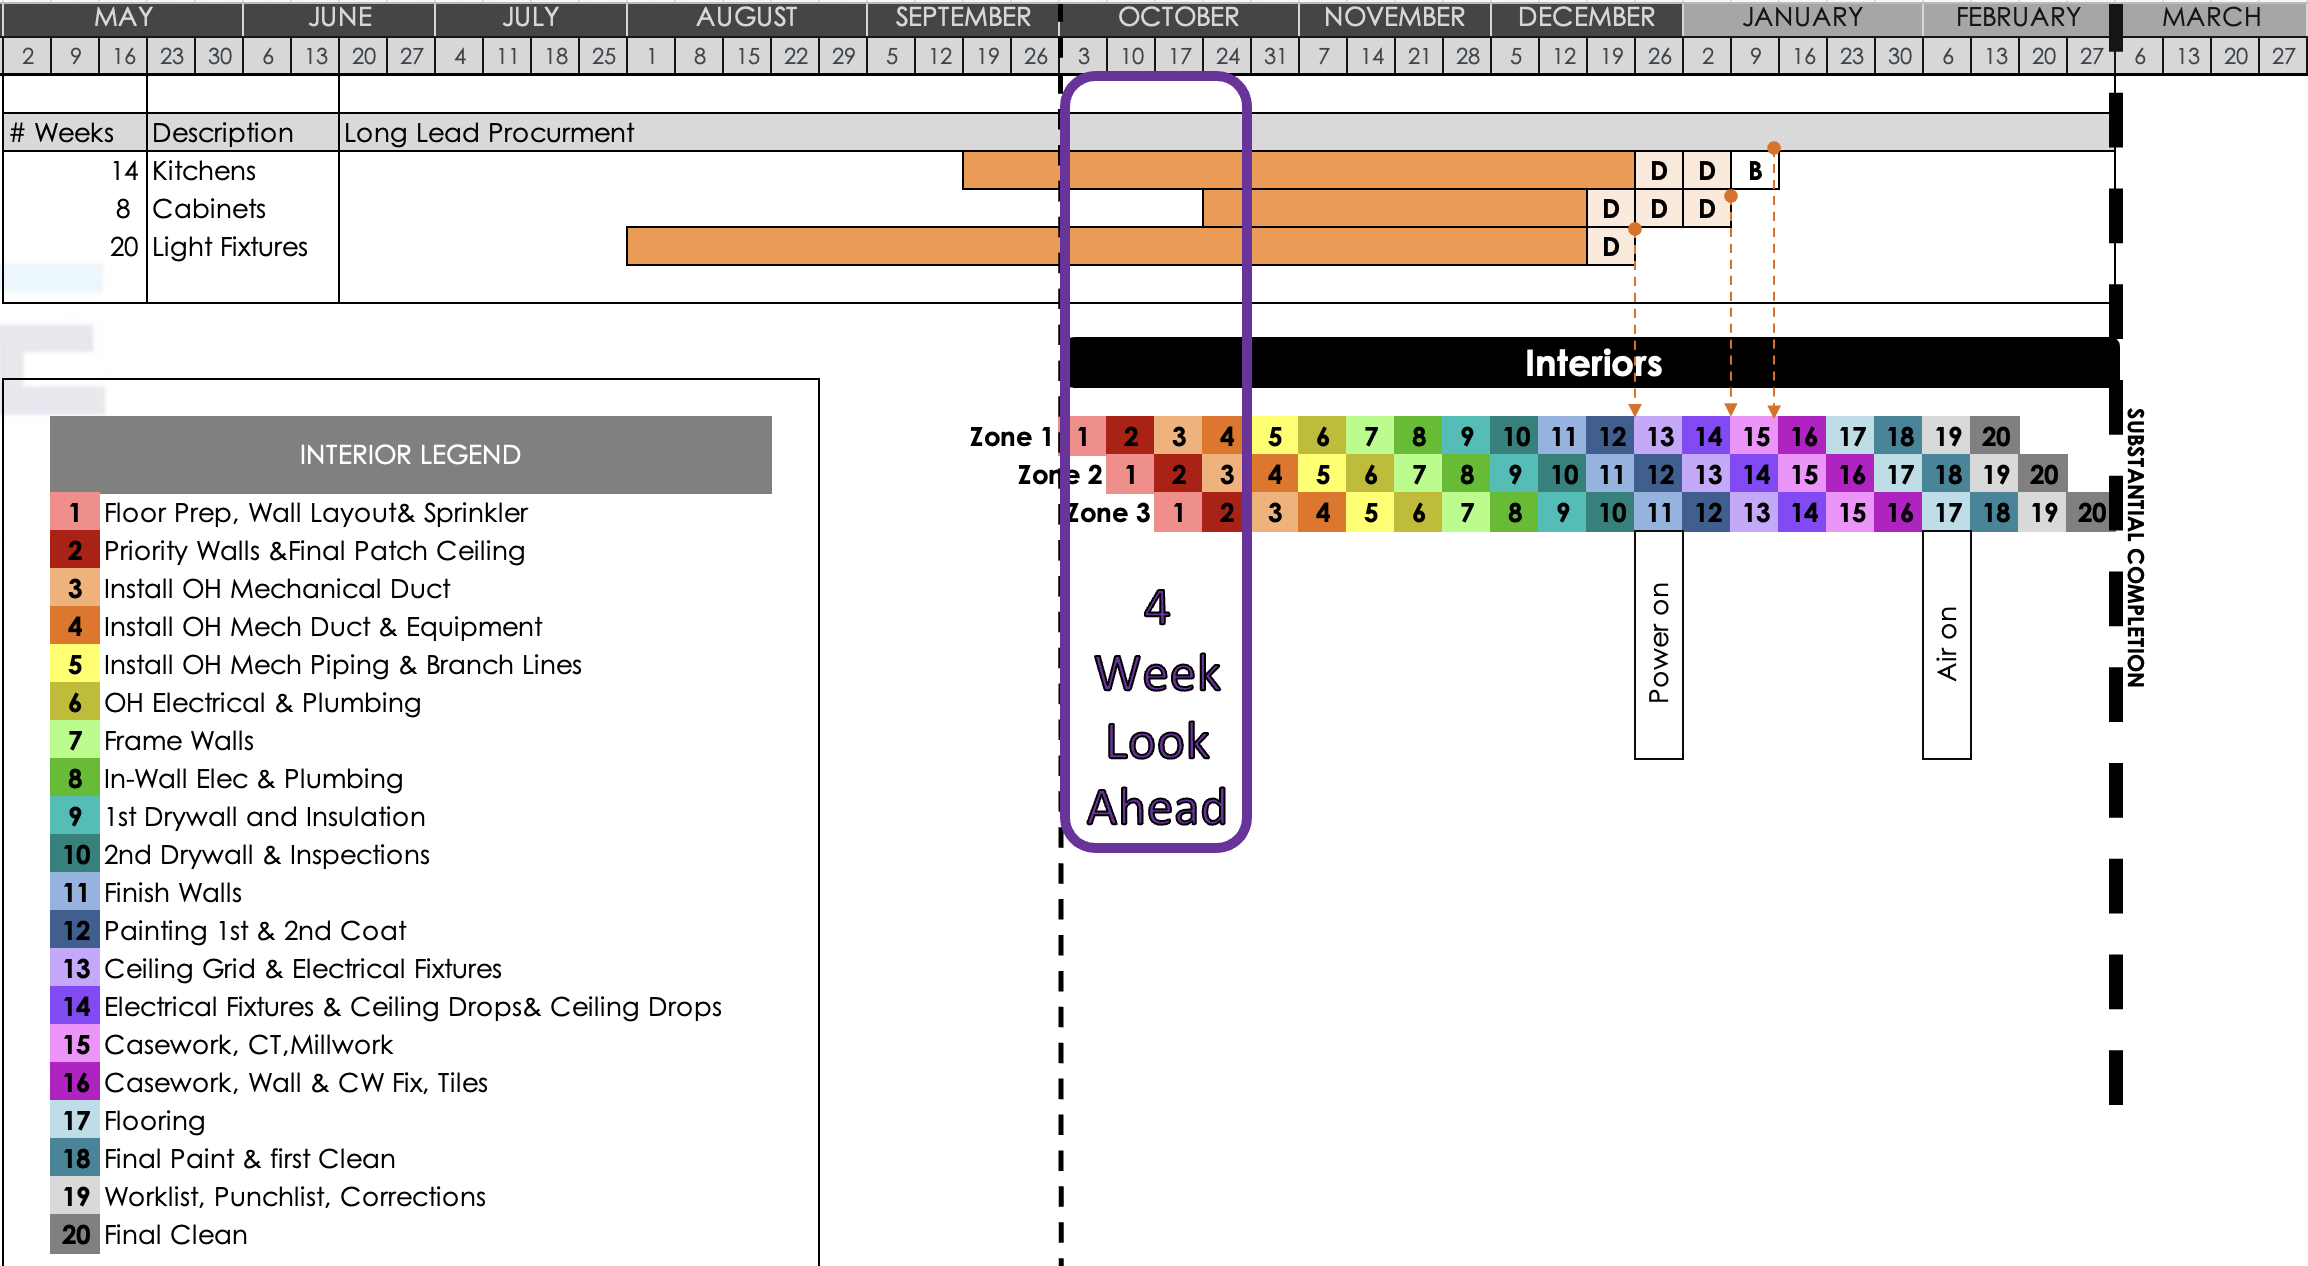
Takt plan with long-lead procurement bars, a 20-item interior legend running across three zones, and a 4-week look-ahead window

Takt Optimization

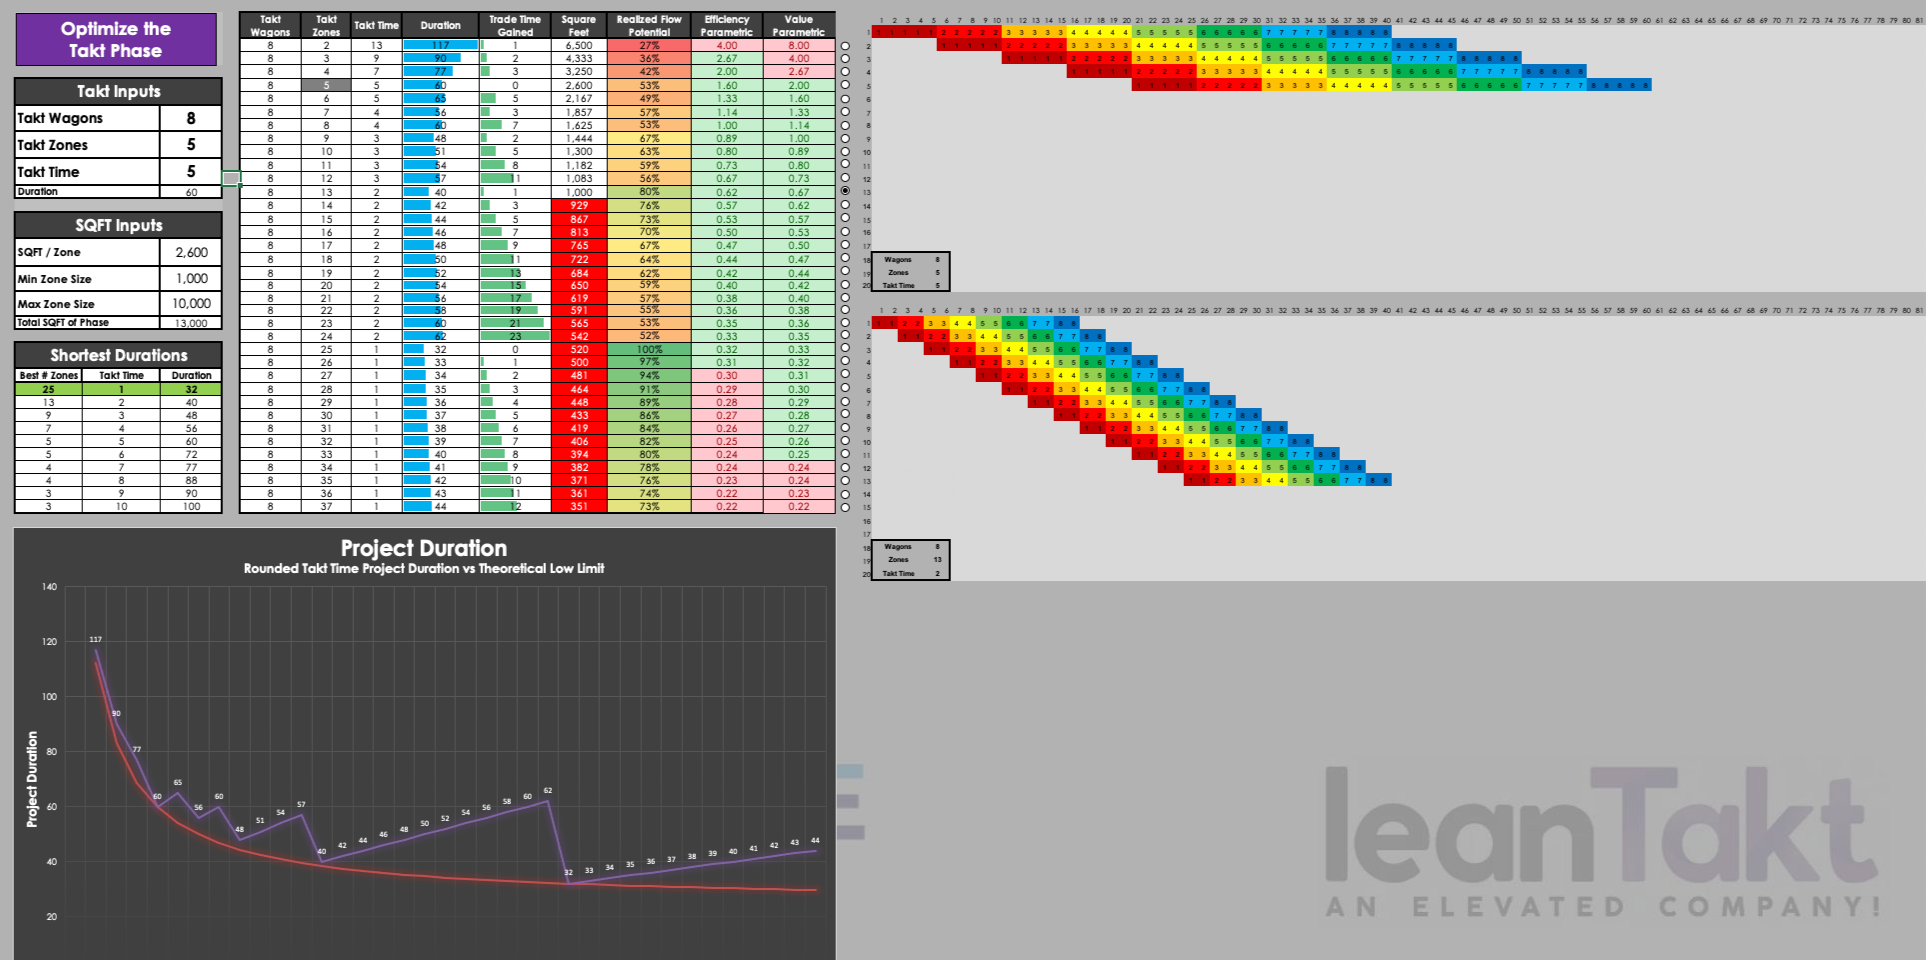
Now you have preliminary Takt zones, Takt time, and sequence. But remember, these are all preliminary. We need to do one more thing, and it is super fun and rewarding. Here is a part of the true power of Takt planning. To optimize your phase we need to introduce a formula:

(TW + TZ -1) x TT = duration or throughput time

This means the number of Takt wagons plus the number of Takt zones minus 1. That sum multiplied by the Takt time in days equals your phase duration or throughput time.

We need to confirm the number of Takt wagons, Takt zones and the Takt time in our phase before moving forward by using this formula and analysis. Now that you know your ideal throughput time, confirm this with the trades and adjust your plan accordingly.

Optimize the Takt Phase spreadsheet comparing numbers of Takt wagons, zones and Takt times against phase duration, with a project duration chart

Network your Phases Together

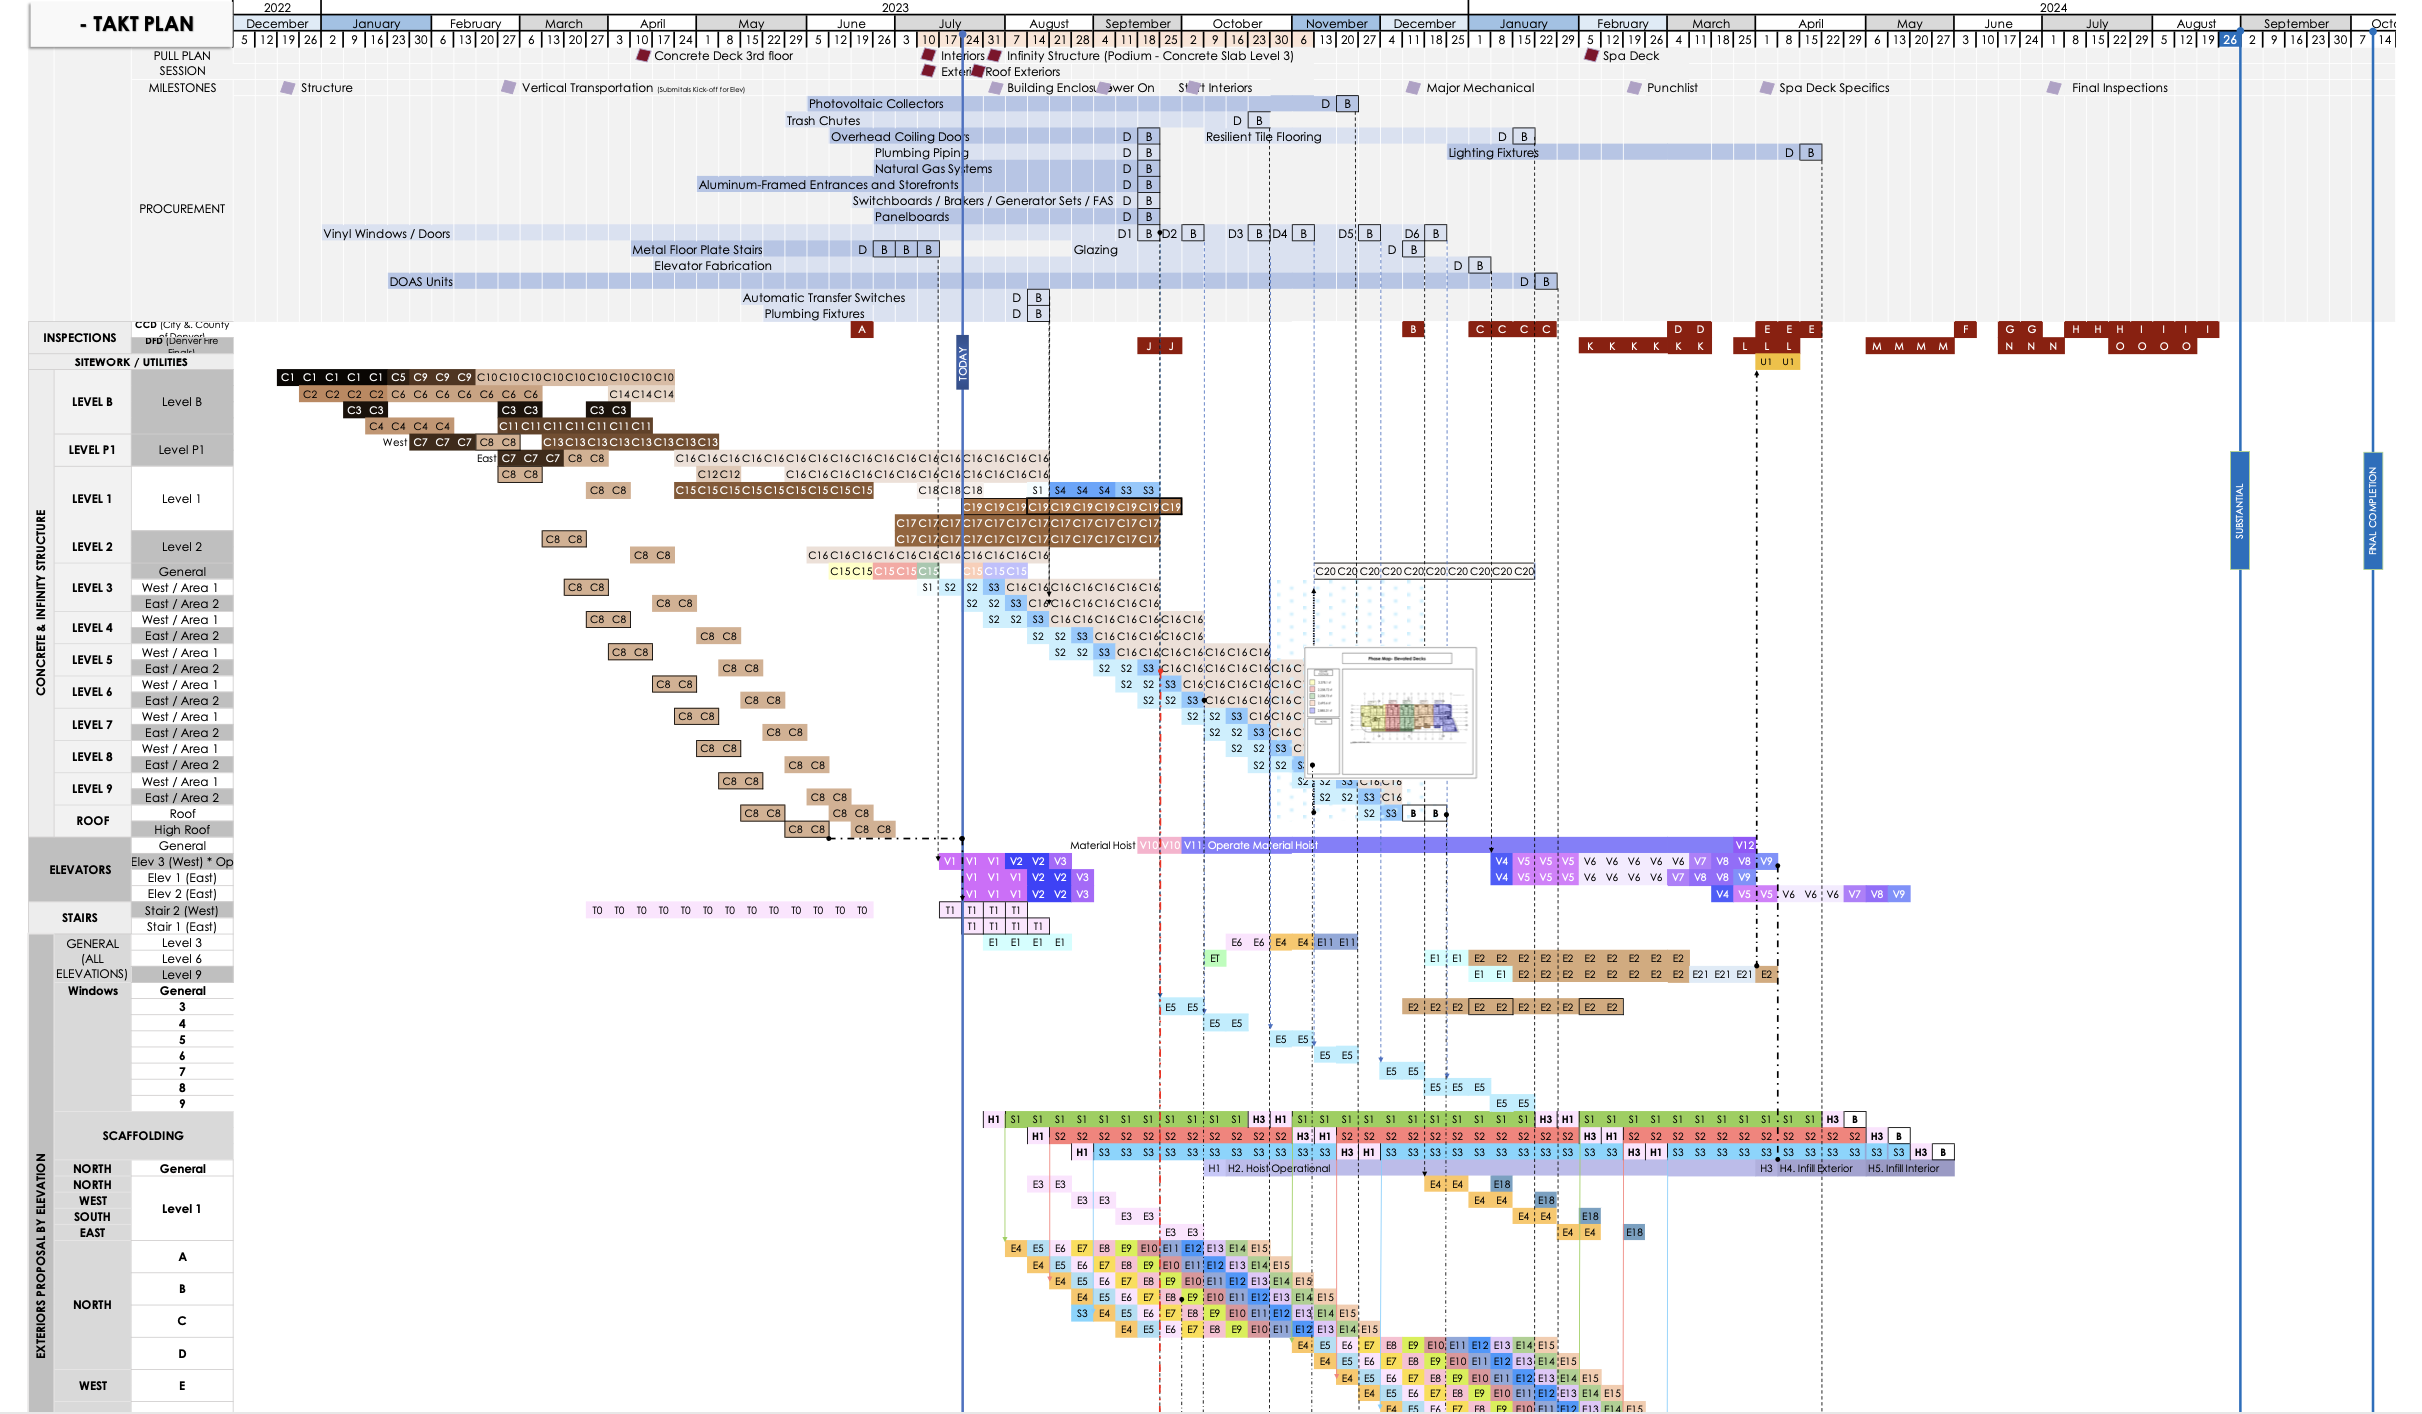
It is important to see all phases of the project and how they network together. This should be done on one sheet regardless of the size of the format. We want to confirm the proper interdependence ties between design, permitting, coordination, contracting, procurement, mobilization, foundations, superstructure, exterior, interior rough-in, interior finishes, roofing, commissioning, site work, and final inspections. Without this, we do not have a proper overall project duration with a reasonable end date that will prevent a crash-landing.

The mobilization phase should provide enough space before foundations can mobilize and begin. The foundations should be far enough along before the superstructure can go vertical and the vertical crews must be high enough or complete so the exterior can begin. The exterior framing should be complete enough that interior walls and demising walls can be framed. Exterior dry-in should be done in time for drywall to begin. For commissioning to begin, the building must be enclosed and HVAC must be available.

This is where Takt planning as a visual is genius. The coordination and peer reviews and the eventual “fresh eyes” meeting can focus on these transitions and how they support the overall flow of the project.

Takt plan with procurement, inspections and color-coded trade sequences by level and zone

Buffer Management

No schedule should ever plan on 100% productivity or efficiency. This would mean we are planning for no variation in construction which would not be responsible. Marion Russell, Greg Howell, Simon Hsiang and Min Liu published an IGLC paper called “Causes of Time Buffer in Construction Project Task Durations”. They surveyed 180 construction personnel about 47 possible causes of time buffer, such as unforeseen conditions, labor shortages, supply chain variances and weather.

There must be buffers in the plan. There are three types of buffers that can be used within Takt plans which include material inventory, capacity and time.

Without buffers we enter a push environment and spiral into a failing situation with overburden, unevenness, and waste (ultimately taking more time). When we have enough buffers, teams can constantly stay in flow. This is due to buffers allowing for statistical fluctuations as described in the Theory of Constraints. If you have buffers, you can gain time. If you don’t have buffers, you will lose time. It is a paradox, but it is true. A plan without buffers is destined to fail.

Create Finalized Takt Zone Drawings

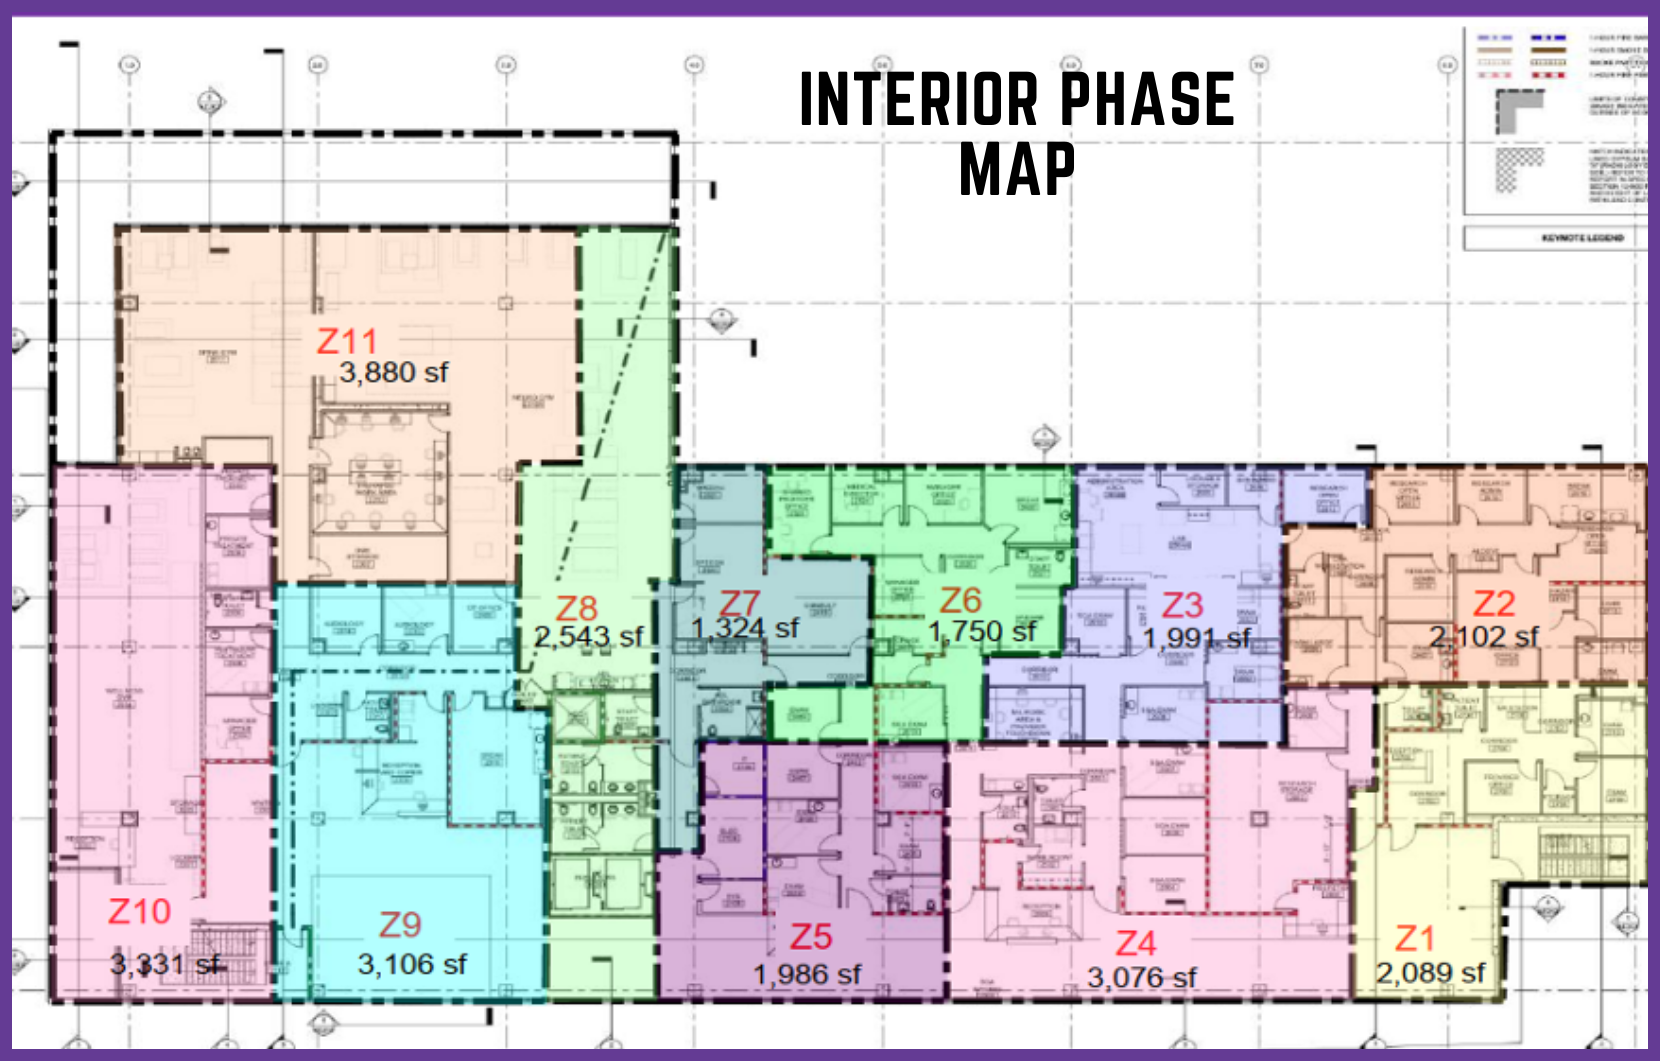
You should have Takt zone drawings for all major phases. Mobilization, foundations, superstructure, exterior and interior work will all have phasing. These Takt zones show the amounts of work that need to be completed according to the Takt time. These drawings should accompany the contract and bidding documents as an exhibit to ensure the system has been properly priced, included in the bid, and aligned with procurement efforts.

Interior phase map with 11 Takt zones, Z1 to Z11, and the square footage of each

Roadblock Tracking Maps

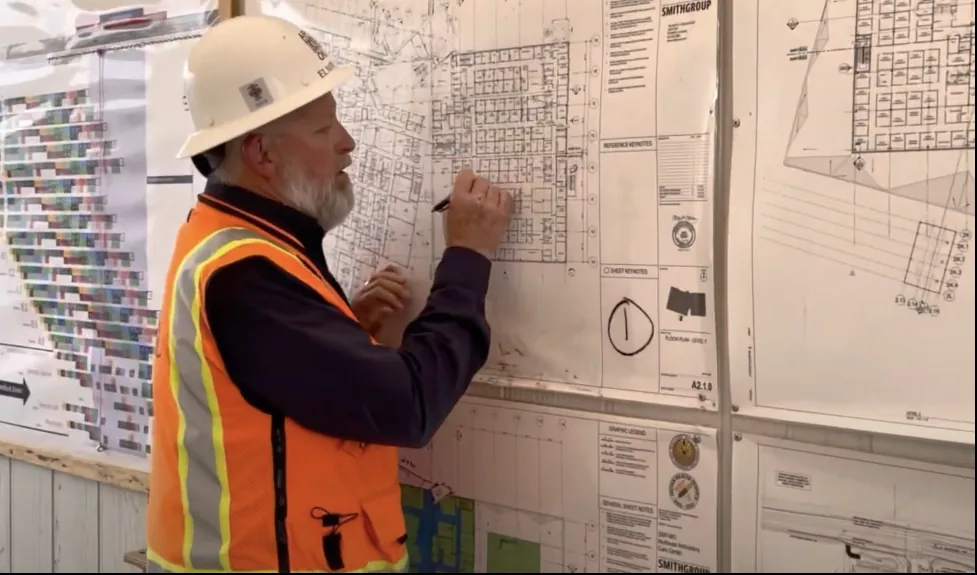
Roadblock tracking maps are crucial to the system. They are used to show the differentiation between typical and non-typical areas and also to track roadblocks visually throughout the system. They can be based on the Takt zone maps and can either be physical drawings with plexiglass coverings on your conference room wall or a Bluebeam Project to which everyone has access. The point is to spend most of the time focusing on the removal of roadblocks as the number one standing tactical order.

Builder in a hard hat and safety vest marking up Takt zone drawings on a wall

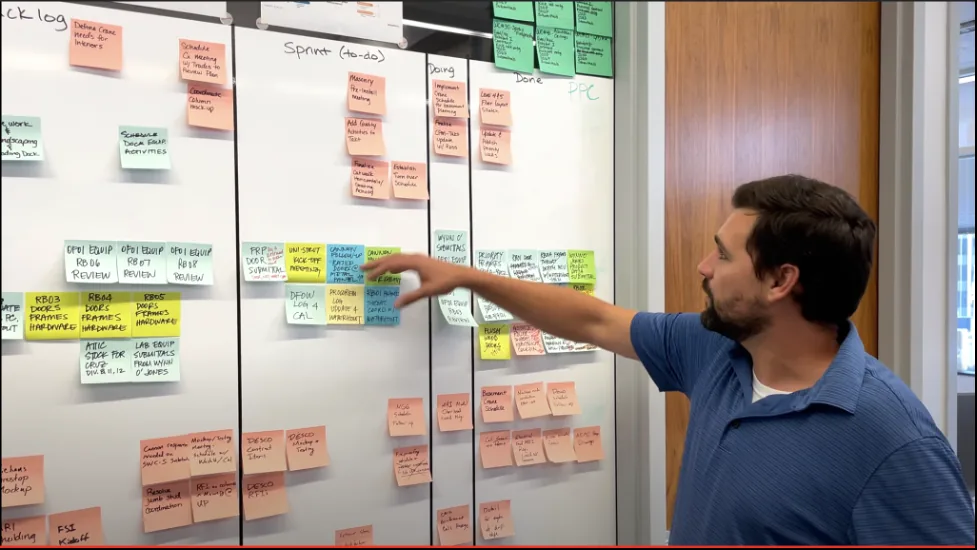
Once you can see them visually you can even use scrum to clear the roadblocks in the most efficient manner.

Team member pointing at a scrum board with backlog, sprint, doing and done columns of sticky notes

Conclusion

Although there are more steps to the process, you now have a Takt plan at the fundamental level. One of the best ways to get started is to experiment with a Takt template in Excel and just have fun. If you do not know Excel, this is such an opportunity for you to learn such a critical and amazing tool. As we leave you to take the Takt template for a drive, let’s remember the fundamental requirements of a Takt plan so we can constantly align anything we create with that vision. A Takt plan is:

  • A visual location-based schedule showing time and space
  • Showing work, trade, and logistical flow (when, what, where, who, how)
  • Scheduled on a rhythm
  • With the appropriate buffers
  • That stabilizes the pace of work with one-process flow and limiting work in process
  • With a reasonable overall project duration
  • It is a system that creates stability in the field which enables—
  • Additional team and builder capacity
  • Consistent crew sizes
  • Consistent material inventory levels
  • The ability to find and remove roadblocks ahead of the work
  • The ability to finish as we go
  • A solid quality program

Good luck! You are about to enter a completely new world of stability and flow.

Want to build your first Takt plan with us? Join the Takt Production System Masterclass.

Want your team trained on this? See our Last Planner® System and Takt training.

On we go!

FAQ

Is creating the Takt plan most of the work?

No. Typically Takt planning takes about 20% of the effort and Takt control in the field is the other 80%.

What is the formula for Takt phase duration?

(Number of Takt wagons + number of Takt zones – 1) x Takt time.

If you want to learn more we have:

-Takt Virtual Training: (Takt Virtual Training)
-Check out our YouTube channel for more info: (Elevate Construction on YouTube)
-Listen to the Elevate Construction podcast: (Elevate Construction Podcast)
-Check out our training programs and certifications: (Training Programs and Certifications)
-The Takt Book: (The Takt Book on Amazon)

Discover Jason’s Expertise:

Meet Jason Schroeder, the driving force behind Elevate Construction. As the company’s Founder and COO, he’s dedicated to taking construction to new heights. With a wealth of industry experience, he’s crafted the Field Engineer Boot Camp and Superintendent Boot Camp – intensive training programs engineered to cultivate top-tier leaders capable of steering their teams towards success. Jason’s vision? To expand his training initiatives across the nation, empowering construction firms to soar to unprecedented levels of excellence.

Posted in All

Takt Theory

Read 14 min

Short answer: Takt is German for beat or rhythm. In construction, Takt planning breaks the job into zones of similar work and moves trades through them on a fixed rhythm (the Takt time), so work flows one zone at a time instead of in batches.

Takt Planning is a detailed one-page, one-process flow schedule that focuses on throughput, production, bottlenecks, and ultimately, creating flow. It is accompanied by Lean practices to be the most effective scheduling tool in the industry for construction because it creates stable construction environments, enables total participation, and provides a basis upon which to improve all aspects of construction.

In German, the word Takt means beat frequency or the regularity with which something gets done. When used with Lean, it means standardization, predictability, and the heartbeat of the project’s production system. Our definition of lean and how it applies to construction is simple and important to define as there has not been a standard until now on what Lean is. We take a similar approach to Niklas Modig in his book This Is Lean, but in this post, we will give our basic definition and links where you can learn more.

What is lean?

  1. Respect for People and Resources
  2. Stability and Flow
  3. Total Participation & Visual Systems
  4. Continuous Improvement & Quality

I go deeper into these principles, and how your team can assess where it is and improve, in our training.

Promo slide for Jason Schroeder’s The Foundation of Construction Excellence online course

Now we understand the basics of the principles that when applied with Takt make all the difference. So let’s dive into the Takt theory side of the equation and for that we start with the basic definitions.

Takt definitions

Takt: German for beat, pulse or rhythm (the same word is used for a conductor’s baton beat).

Takt in Takt Planning: The individual cell representing the intersection of time and space. This can be empty or include a Takt wagon. It is the basic unit of a Takt plan.

Takt Plan: The strategic and logistical visual plan that shows the Takt trains in relationship to each other per the specified Takt time with columns of time and rows of Takt zones (geographical location) or general sequences.

Takt Control: A tactical system of holding the dates, stabilizing procurement, limiting work in process, and finishing as you go. It is the process of using the execution plan within the Takt plan that is constantly evolving and making short-cycled adjustments of the Takt plan to increase flow and improve the execution of the work. Typically, Takt planning takes 20% of the time in development, and the remaining 80% is spent in Takt control.

Takt Phase: The grouping of Takt trains by zones that compile to make up similar types of scope, e.g., structural, rough-in, and exteriors. Takt time and throughput time are specific to Takt phases.

Takt Zone: A production area that is determined by its repeatability and ability to fit into a rhythm with other areas to balance the overall production schedule. This is a batch of geographical area that is either increased or decreased to achieve flow.

Takt Train: A series of wagons in a Takt zone. This is also sometimes called a Takt sequence.

Takt Wagons: One or more work packages or scope(s) of work packaged into a single cell in a Takt train usually shown on Excel, or a Takt wagon in a Takt planning app.

Work Packages: Features of work or scopes within a Takt wagon. If found within the same Takt wagon, they should not constrain or hinder each other in any way.

Work Steps: The tasks in the installation process within the work package. For example, if your work package was OH Electrical, then the steps might be conduit runs, light boxes, fire alarm, cable tray, low voltage, etc.

Takt Time: Measurable beat time, rate time, or heartbeat. In Lean, Takt time is the rate at which a finished product needs to be completed in order to meet customer demand. It is the syncopation or rate of beats such as one might find on a metronome. To expound, Takt time is the duration of the time scale into which the Takt wagons are fit. If the Takt time is five days, the wagons fit into multiples of that duration. If a wagon includes the work package of overhead mechanical and that overall duration is fifteen days, and the Takt time is five days, there will be three Takt wagons that say, “Overhead Mechanical” in three Takt time slots.

Takt plan with procurement, inspections and color-coded trade sequences by level and zone

Where does Takt come from?

Takt time is taken from the German word Taktzeit, meaning cycle time. According to Mark Graban, Colin Ducharme and Todd Ruddick’s MIT lecture notes on Takt time, “The word was likely introduced to Japan by German engineers in the 1930s,” which explains why Lean and Takt have an interwoven history.

The actual word originates from the Latin word tactus meaning touch, sense of touch, feeling. Some earlier meanings include beat triggered by regular contact, clock beat from the 16th century, beat indicating the rhythm pertaining to music, and also regular unit of note value from the 18th century.

Takt is focused on the rhythm of sequences or geographical areas on the project site sometimes known as location-based scheduling. European countries have successfully been using this type of scheduling for years. Early Takt plans have been found from Norway with ship building. Also, in Russia and Germany over a century ago with a very detailed and sometimes complex mathematical analysis. Takt planning has been called a variety of names over the years: One-Process Flow Scheduling, Linear Scheduling, SIPS, Line of Balance, or Even Flow Production. It feels appropriate to call it by the name of Takt because it has a good brand name throughout the industry currently and allows us all to rally behind the concept together.

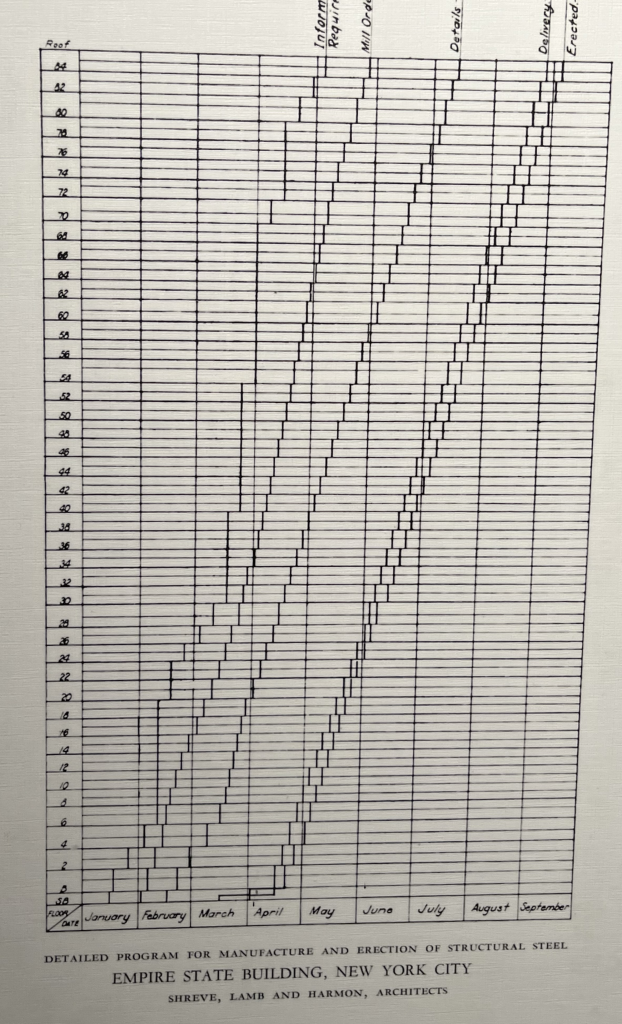
Takt planning can be seen in the construction of the Empire State Building

Empire State Building detailed program for manufacture and erection of structural steel, floor by floor and month by month

and more recently in the United States Pentagon Renovation constructed by Hensel Phelps in 2002. This planning was termed SIPS, or Short Interval Production Scheduling, which is what we have termed above a Takt phase and are very similar in execution.

Hensel Phelps Pentagon Renovation SIPS schedule with color-coded trades moving area by area

Despite both of these projects being wildly successful, CPM continues to be the dominant scheduling system in the United States. The argument for CPM is typically the favoring of data and data mining; however, visual schedules and uniting the workforce around a common plan should be more important. Additionally, Takt is not only rich with data, it is also the only scheduling system based on mathematical production equations and production laws.

Aerial photo of the Pentagon split into five numbered wedges next to a floor plan divided into color-coded phases

Batching vs. One-Piece Flow

The biggest difference between CPM and Takt is one-process-flow vs. batching. One-process flow describes a condition where work is finished one scope or process at a time from beginning to end, instead of in large batches. Processes or work moves from phase to phase or step to step in a flow on the shortest path possible on its way to the customer. Examples of one-process flow are as follows: Sending out meeting minutes right after the meeting, filling out an inspection report right after the visit, answering emails as they arrive, finishing work areas by scope while there and work is in progress, excavating, installing, inspecting, and backfilling sections of pipe in segments, and starting, building, and completing phases of work before starting another one. To do this, we need to be open to one-piece flow.

Diagram comparing batching with one-process flow, from unprocessed materials to finished areas

One-piece flow is a concept centered around flow units progressing from inception to the customer on the shortest path possible. All parts are working in unison accepting and passing work to the next trade in line (sequence). It means that we reduce the amount of work in process and we finish one piece of work as we go and move work down the line in smaller amounts as opposed to batching.

What is batching in construction?

Batching occurs when product, work, or assemblies are completed in groups to increase the efficiency of resources rather than flow. Batching work in construction looks like doing one scope of work throughout the entire floor or entire building without respect to flow. A good example to show the difference between one-piece flow and batching is the envelope game. In the envelope game two contestants are given twenty envelopes, papers, and stamps.

The first contestant is told to fold all papers at once, stuff the papers at once, lick and seal them at once, and then stamp them at once. The second contestant is told to fold, stuff, lick, seal, and stamp each of them one at a time. Each contestant starts at the same time and is asked to finish as fast as possible. It is nerve wracking to watch this game because the batching contestant looks sure to win, but with two minutes to spare, the one-piece flow contestant finishes first. One-piece flow is faster and always will be because it releases work on a rhythm and allows work to flow.

The batching system is usually preferred because it looks like it goes faster, but that is simply because it is riddled with motion and transportation (picking envelopes up, putting them down, over and over) which is waste. With Takt systems or flow systems, we finish as we go or follow the concept of one-piece flow which means the work is delivered to the customer in the fastest way possible. This creates flow.

Why does flow matter in construction?

Flow is a priority for construction. Why? Because flow enables the very long supply chains upon which we rely in construction by holding to consistent dates, and it reduces the material inventory levels and worker counts on a project site at the end of that supply chain by allowing us to bring out materials just-in-time.

This is important because the reduction of material inventory is essentially the reduction of overproduction in construction which then reduces all other wastes! When overproduction and excess material inventory are reduced, the need for fixing defects, over processing, waiting, transportation, and motion are reduced because we are using the genius and capabilities of the team, maintaining a consistent schedule and flow one-process or one Takt-ed process at a time.

The effects that waste, variation, and roadblocks have on production in the field are widely recognized and accepted, and at a minimum, they culminate in wait times and prevent good flow. If we maintain flow, prepare our work, stabilize our supply chains, and hold our dates according to a good Takt time, we will have a good flow of information, worker counts, and materials because the dates, rhythm, targets, and expectations all remain consistent, steady, and continuous, just like when water flows.

Holding the line

Just-in-time deliveries really only work with Takt planning and really only work when project teams hold to the rules of Takt by holding the dates. Now, there are some exceptions to this rule. If there is a major shift needed for project success that can be coordinated with all participating contractors onsite and that can be coordinated with procurement, then this type of change may be acceptable.

But for the most part, gaining time in Takt planning is done in the plan analysis where we optimize throughput time and gain buffers by running simulations that determine the ideal project duration based on the number of Takt wagons, Takt zones, and the Takt time. When a project is coming out of the ground, expediting, or advancing the schedule is more appropriate because there are fewer contractors. Therefore, it is more acceptable in the early phases, but only under rare circumstances should dates be moved and start dates be adjusted when there are over ten contractors onsite working in rough-in, exteriors, or finishes.

With Takt systems we need to hold the line, keep the rhythm, and be disciplined, otherwise we leave the system and the project descends into chaos. Therefore, Takt planning requires project teams to hold others accountable, control the site, and hold the line. This is very difficult for a team and can be a reason project teams may be hesitant to use the Takt system. It is also why trades may be hesitant to participate with Takt because they will be held accountable. You can be sure that weak leaders and non-accountable trades will not like Takt. Takt keeps the system stable, and then the team can accelerate when the system is stable.

Bottlenecks

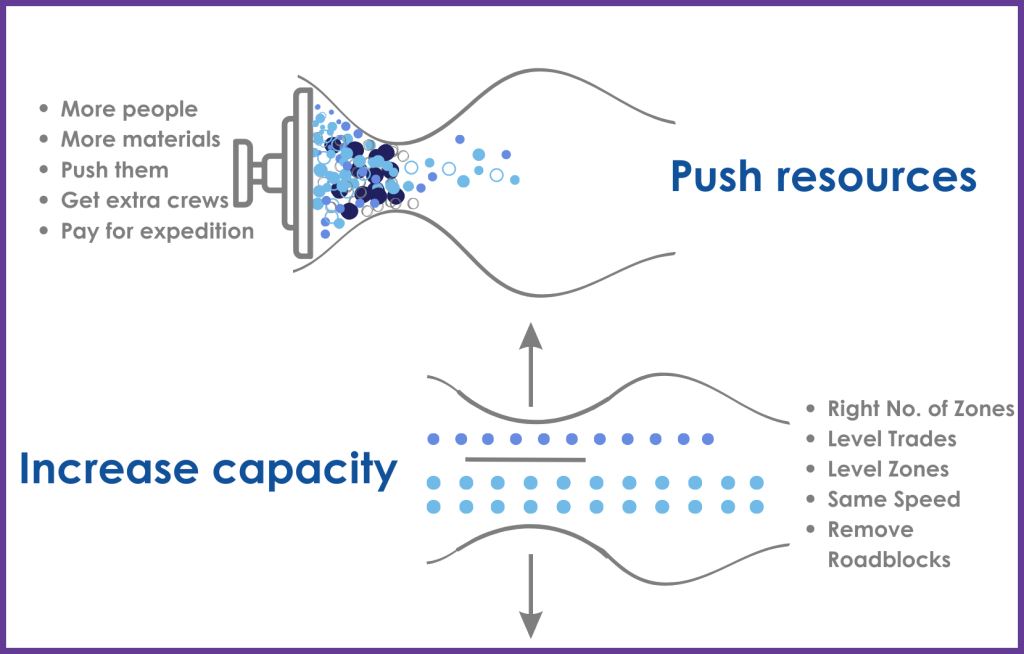
Some may be very concerned about our comment to slow down certain resources but consider what happens when, after we have optimized and sped up all bottlenecks, we continue to let the faster trades continue to go fast. What happens? People are stacked in certain areas without flow, without geographical control, burying certain scopes, and/or installing too early which increases the amount of defects and use of resources such as the project management team’s time. This affects the trades that really need the help. There is little merit to going faster than the general throughput.

The Law of Bottlenecks: According to Modig, the Law of Bottlenecks states that throughput time is primarily affected by the process that has the longest cycle time. In construction, the overall throughput of the phase is mostly affected by the process with the longest duration within the system.

Slide comparing pushing more resources into a bottleneck with increasing capacity through the right number of zones, level trades and roadblock removal

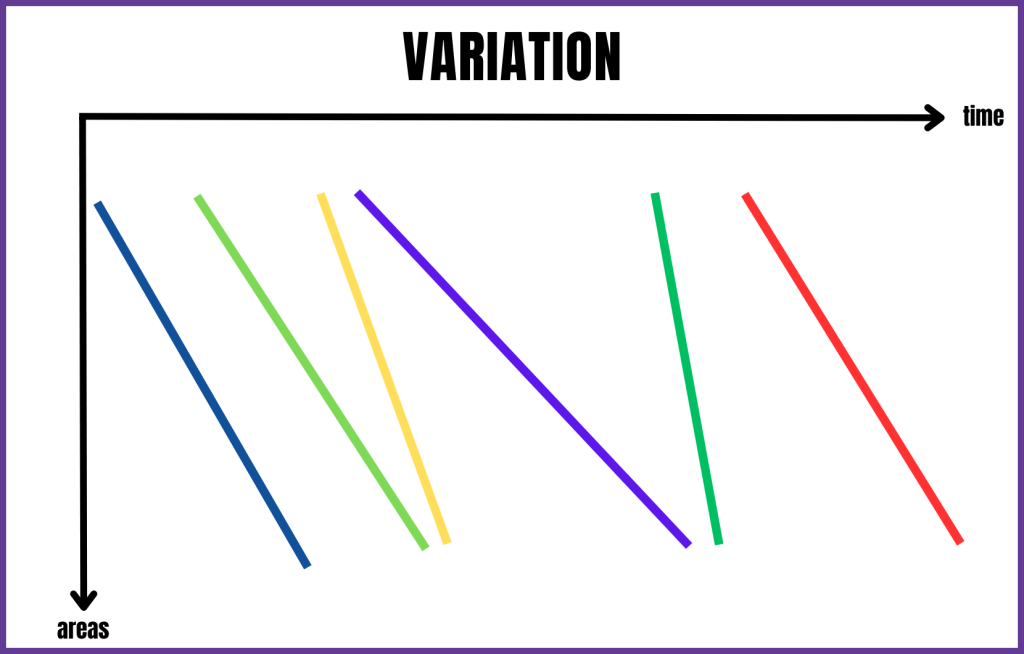
Best practice is to first optimize the bottlenecks for the slower installations and then to even out the throughput of the remaining work; therefore, the entire system. Because CPM does not allow us to see our bottlenecks, we cannot optimize them so the system ends up with a longer overall project duration, overproduced areas, fluctuating worker and material inventory levels, and a number of detrimental starts and stops.

Variation chart: trade lines with different slopes across areas and time

The tricky thing with bottlenecks is that new ones will show up when you optimize the first ones or the largest ones so it is a continual game of increasing flow by adjusting the throughput of the system. This is the key to achieving the shortest overall duration, with the smallest crew sizes, with the most minimal material inventory, in a visual system that identifies problems when they happen, in a continuous flow that allows an evenness the team can use to focus their attention on the removal of roadblocks.

Roadblock removal

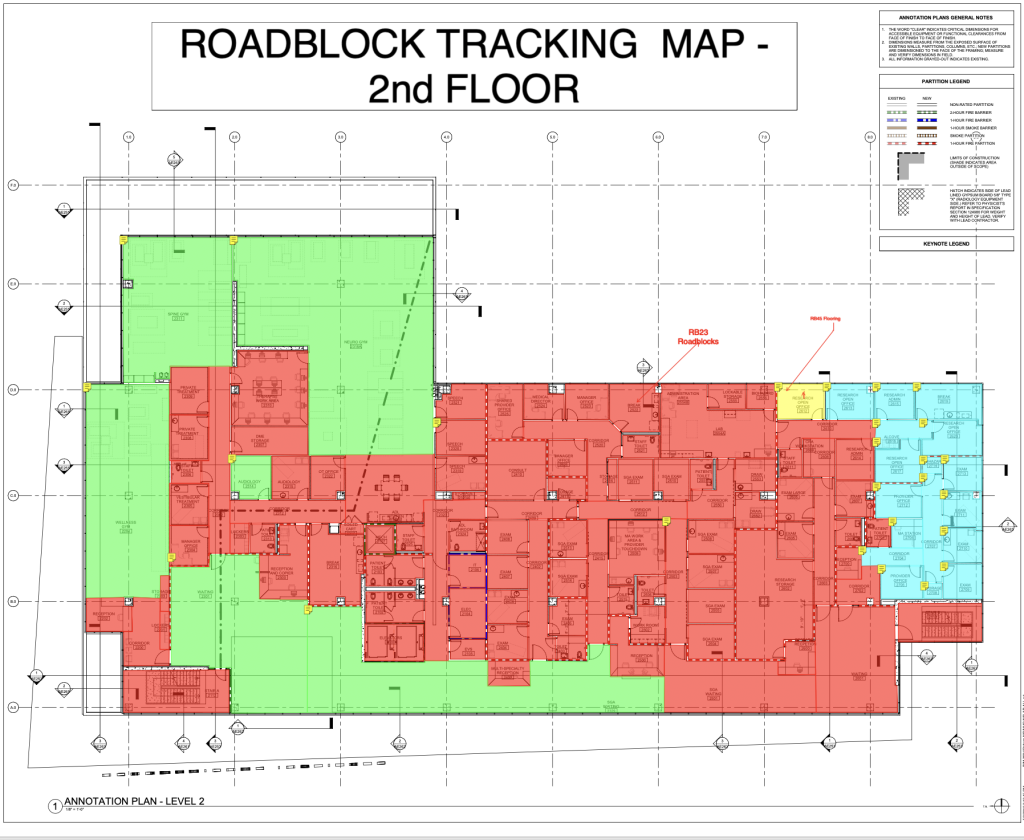
Roadblock tracking maps are crucial to the system. They are used to show the differentiation between typical and non-typical areas and also to track roadblocks visually throughout the system. They can be based on the Takt zone maps and can either be physical drawings with plexiglass coverings on your conference room wall or a Bluebeam Project to which everyone has access. The point is to spend most of the time focusing on the removal of roadblocks as the number one standing tactical order. We will soon explain how this is done.

For now, we need to understand that the goal of Takt is to even out the flow by removing roadblocks that become visual. As we remove roadblocks, reduce variation, and increase our visibility and effectiveness, we will understand the true production rate or throughput for this type of work in this geographical area and you can now set a realistic Takt time and hold it.

Roadblock tracking map floor plan with red and green zones

Ready to build your first Takt plan? Join the Takt Production System Masterclass.

Want your team trained on this? See our Last Planner® System and Takt training.

On we go!

FAQ

What does Takt mean?

Takt is German for beat or rhythm. In lean, Takt time is the pace work must hit to meet demand.

Is Takt the same as line of balance?

They’re close relatives. Line of balance, linear scheduling and SIPS are all location-based methods; Takt adds a fixed rhythm, zones and work packaging.

If you want to learn more we have:

-Takt Virtual Training: (Takt Virtual Training)
-Check out our YouTube channel for more info: (Elevate Construction on YouTube)
-Listen to the Elevate Construction podcast: (Elevate Construction Podcast)
-Check out our training programs and certifications: (Training Programs and Certifications)
-The Takt Book: (The Takt Book on Amazon)

Discover Jason’s Expertise:

Meet Jason Schroeder, the driving force behind Elevate Construction. As the company’s Founder and COO, he’s dedicated to taking construction to new heights. With a wealth of industry experience, he’s crafted the Field Engineer Boot Camp and Superintendent Boot Camp – intensive training programs engineered to cultivate top-tier leaders capable of steering their teams towards success. Jason’s vision? To expand his training initiatives across the nation, empowering construction firms to soar to unprecedented levels of excellence.

Posted in All

988 Suicide & Crisis Lifeline

Read 3 min

Short answer: If you or someone on your crew is in crisis, call or text 988 (or chat at 988lifeline.org). It’s free, confidential and available 24/7 anywhere in the U.S. Veterans press 1 after dialing.

“988” is the three-digit, nationwide phone number to connect directly to the 988 Suicide and Crisis Lifeline.

What is the 988 Suicide & Crisis Lifeline?

Too many people experience suicidal crisis or mental health-related distress without the support and care they need. There are urgent mental health realities driving the need for crisis service transformation across our country. In 2020 alone, the U.S. had one death by suicide about every 11 minutes—and for people aged 10-34 years, suicide is a leading cause of death.

There is hope. The 988 Suicide and Crisis Lifeline – previously known as the National Suicide Prevention Lifeline – is a national network of more than 200 crisis centers that helps thousands of people overcome crisis situations every day. These centers are supported by local and state sources as well as the Department of Health and Human Services’ Substance Abuse and Mental Health Services Administration (SAMHSA).

As of July 16, 2022, all calls and text messages to “988” route to a 988 Suicide and Crisis Lifeline call center.

The 988 Suicide and Crisis Lifeline provides 24/7, confidential support to people in suicidal crisis or mental health-related distress.

Call or text 988, or chat at 988lifeline.org. It’s free, confidential and open 24/7.

How do you reach 988?

  • Support for loved ones: You can also dial 988 if you are worried about a loved one who may need crisis support.
  • FCC Rules: Under FCC rules, calls and texts to 988 will be directed to the Lifeline. Calls and texts to 1-800-273-8255 (TALK) will also continue to reach the 988 Lifeline even after the nationwide implementation of 988.
  • Saving Lives: The FCC actions reflect its commitment to saving lives and connecting individuals to necessary intervention services. Switching to the easy-to-remember 988 makes it easier for individuals in crisis to access the help they need and decrease the stigma surrounding suicide and mental health issues.
  • Important Step: The 988 Suicide and Crisis Lifeline is an important step toward strengthening and transforming crisis care in this country. It serves as a universal entry point so that no matter where you live, you can reach a trained crisis counselor who can help.
  • Help for Veterans: After dialing 988, press 1 to reach the Veterans Crisis Line, which serves veterans, service members, National Guard and Reserve members, and the people who support them.

Source: SAMHSA, 988 Suicide & Crisis Lifeline and the 988 Lifeline.

Why we post this for construction

Construction has one of the highest suicide rates of any industry. Put 988 on your orientation slides, your huddle board and your hard hat stickers so every worker knows it before they ever need it. More on mental health in construction.

We at the Elevate team feel it is important that this information is posted for our industry. We encourage you and your organization to make this information available to your employees and create awareness around it.

Leaders: make 988 part of your orientation. Our orientation guide is here.

On we go!

People Also Read:
Mental Health, Feat. Jake & Jason

Discover Jason’s Expertise:

Meet Jason Schroeder, the driving force behind Elevate Construction. As the company’s Founder and COO, he’s dedicated to taking construction to new heights. With a wealth of industry experience, he’s crafted the Field Engineer Boot Camp and Superintendent Boot Camp – intensive training programs engineered to cultivate top-tier leaders capable of steering their teams towards success. Jason’s vision? To expand his training initiatives across the nation, empowering construction firms to soar to unprecedented levels of excellence.

Posted in All

The Updated Contract Inclusions List

Read 12 min

Short answer: If you want lean behaviors on your project, write them into the contract. Below are clauses you can paste into your exhibits or work orders for real-time cleanup, just-in-time deliveries, daily huddles, a daily crew setup, QC checklists, zero tolerance safety, approved foremen, contractor grading, safety training, delivery scheduling and Takt.

What should a lean construction contract include?

Do you want to implement Lean on your project? If so, you must specify it. That does not mean you have to pay extra for it, although there are some more upfront costs when running a lean project. Really, you are moving some small costs up front to prevent massive contingency usage later. Here are some examples of things you can include in your exhibits, work orders, work authorizations, or contracts to buy the behaviors you want:

Cleanliness

Cleanliness will be real time for all crews onsite. Workers and crews will keep their areas clean and swept to support a safe and productive work environment. The focus will be on the habits of the workers, and not simply cleanup at the end of the day. Workers and crews will be trained on cleaning as they go, and not allowing things to hit the floor. They will be expected to stay clean and organized so they can achieve better quality, better production, and a safer work environment. No composite cleanup crews will be used on the project for any contractor. If a worker or crew makes a mess, they will be asked to stop and clean it and work with better habits moving forward. Cleanup at the end of the day is still encouraged, but cleanliness is enforced while the crews work.

Just-In-Time Deliveries

Deliveries of materials shall be coordinated to the right inventory buffer. Too much material inventory will not be allowed, and zero inventory is not productive. The right sized inventory buffers for your scope shall be coordinated with the superintendent. Do not assume deliveries will be brought out all-at-once, by building, or by floor. Deliveries by default should be by sequence area or Takt zone and approved by the superintendent. Staging at the place of work should not be assumed and, again, must be approved beforehand. In some instances, deliveries may need to be broken up to accommodate the materials arriving just-in-time to be installed within the proper lead time.

In summary, materials can be coordinated to arrive onsite from the vendor to the place of work, or materials can be coordinated to arrive to a laydown area and then to the place of work. Material inventory will only be allowed at the place of work according to the agreed-upon inventory buffer (Shown by “amount” by “time”). These buffers will be shown on the schedule or in the procurement log.

Worker & Foremen Huddles

All workers will attend a daily worker huddle at the start of the day to communicate safety items and the plan for the day. Attendance is mandatory. It is expected that the content shared in the huddle will communicate items to workers that will keep them safer and more productive throughout the project. Additionally, trade foremen are required to plan the next day with the group and coordinate deliveries, work areas, safety, labor, and material laydown. Attendance is mandatory and crucial to enabling workers in a safe and productive manner.

Daily Crew Setup (15-25 Minutes)

Workers will be expected to spend the first portion of their day preparing the work of the crew. The recommended agenda is shown below:

Consider a 15 to 25-minute duration for all craft to set up their day. Provide them 5s & 8 waste cards and encourage habits daily.

  • 5 min worker huddle with entire site.
  • 15-20 min crew setup:
  • Walk area of work
  • Pre-task plans
  • 5s area
  • Sort (Seiri)
  • Set in order (Seiton)
  • Shine/Sweep (Seiso)
  • Standardize (Seiketsu)
  • Sustain/Self-discipline (Shitsuke)
  • Set up work area for success by eliminating the 8 wastes
  • Inventory – Storing parts, pieces, documentation ahead of requirements
  • Over production – Making more than is IMMEDIATELY required
  • Transport – Moving people, products & information
  • Motion – Bending, turning, reaching, lifting
  • Waiting – For parts, information, instructions, equipment
  • Over processing – Tighter tolerances or higher-grade materials than are necessary
  • Defects – Rework, scrap, incorrect documentation
  • Non-utilized talent – Underutilizing capabilities, delegating tasks with inadequate training
  • Gather all tools and needed equipment
  • Barricade (safe off) work areas

The point of this time is to ensure the workers are all prepared for the day with tools, equipment, instructions, materials, and a place to work.

QC Checklists & Inspections by Foremen

Each phase of work shall have a checklist or Feature of Work board with visuals before crews go to work. A representative from each trade will be responsible to research the plans, specs, codes, safety manual, and any other pertinent information before the pre-install. After the meeting, the information is to be summarized and formatted before the work begins. Each crew is to have with them a quality checklist for the work or a visual that has been reviewed by the general contractor. Every crew, every day, has a pre-task plan and quality expectations.

iPad for Foremen

Foremen will be expected to view the plan for the day, scheduling software, a project management software, and other project management applications. Each foreman is to have an iPad for his or her work.

Zero Tolerance Systems

As Steve Gruenert and Todd Whitaker put it, “The culture of any organization is shaped by the worst behavior the leader is willing to tolerate.” On our projects, because of our respect for each person, we will have a respectful and caring “zero tolerance” policy on certain items that are part of, and completely consistent with, our safety program.

Communication and enforcement of our safety program provides equal opportunity for everyone to work and be respected.

The following are items in which we use a “zero tolerance” approach as part of our efforts to ensure enforcement:

· Any violation of safety that is contrary to site standards, project orientation, and OSHA basic standards.

· Anything that is indicative of bad behavior, bad attitudes, not paying attention, or not being trained for the task.

· Any violation that is high risk that creates imminent danger to persons or property (i.e. ladder use, electrical, fall protection, confined space, excavations violations, etc.).

· Not wearing P.P.E. including hard hat, safety vest, safety glasses, and proper protective clothing. This is a very important issue. Please know that wearing proper P.P.E. (and specifically safety glasses) has a psychological effect. It sets the standard of behavior onsite. If someone will not wear their safety glasses, they likely will not wear their fall protection properly. The important standards will be kept like the minimum standards are.

· Clean jobsite and daily housekeeping including proper staging of materials in approved and designated locations.

· You can expect that we, as the general contractor, will provide this safe and productive workplace. In turn, we will require your efforts also by supporting this “zero tolerance” policy and we will do this by:

o The site orientation will explain this approach to everyone.

o Everyone onsite must set the example and enforce the policy.

o We will hold huddles daily which will remind people and train them on the standards.

o If someone is observed being unsafe, we will say to them, “Because I care about your safety, we need to give you time to focus, re-train, or plan the work. So, let’s have you go through orientation in the office, or receive training from your supervisor before continuing work, and you can come back once oriented or re-trained. (Unless it is a major violation)”

o We will send an email to that person’s company explaining why that person was paused for their own safety and the benefit of their family, ask that the person be re-trained, and offer them an opportunity to come back once they have gone through orientation. (Unless it is a major violation).

o We will log the name and violation on a log to track repeat offenders that cannot come back.

o If it is minor, they come back through orientation.

o If they do it again, they cannot come back.

o If it is a serious violation that is high risk, they cannot come back.

We know that each person must make a conscious effort to be safe for themselves and all those around them. So, again, why do we take a zero-tolerance approach? It is based on respect for people. We take care of and treat people well because we respect them. We are safe because we respect all people and their families. We provide adequate facilities, bathrooms, lunchrooms, and treat people fairly because we respect them. We keep perfectly clean jobsites because we respect the productivity of other trades. We do not tolerate safety violations because we respect people’s lives and the well-being of their families. We do not tolerate unsafe behaviors because we respect people.

Approved Foremen

All foremen must be approved by the onsite team. Foremen must comply with the following requirements, or they will be removed from the project.

· Be located in the jobsite trailers or onsite.

· Bring materials to the site, “Just in Time!”

· Enforce site safety rules from Safety Manual

· Keep crew operations clean and organized 100% of the time. Do not wait until the end of the day.

· Do not let materials touch the ground. Either new materials or trash.

· Spend time every morning teaching about the 8 wastes, 5 S-ing, and lean concepts. Allow crews time every morning to get their day set up, clean, and organized.

· Participate as a project team member in the last planner meetings and morning huddles.

· Encourage your crews to come up with lean improvement ideas.

· Maintain parking for your company and ensure there is no impact to the customer.

· Material deliveries for equipment and supplies will be posted in a visible location for the entire team to see. All deliveries will be scheduled per jobsite rules.

· Every foreman supervising in the field will attend a pre-install meeting before commencing the Feature of Work and prepare for the meeting by reading all associated plans, specifications, and shop drawings. The product of this review will be a subcontractor provided checklist of critical quality items pertaining to the installation. If the foreman or superintendent does not come prepared, the meeting will be summarily cancelled and rescheduled as soon as a commitment can be made to properly research the scope.

· Contractor will participate in phase planning sessions to develop the overall schedule.

· Foremen will identify and help the team remove roadblocks ahead of the work.

· Foremen will have a good attitude and partner with the project team.

Foremen by Geographical Area

The project will be broken up into geographical areas for operational control. Each area will be supervised with a superintendent and field engineer. Foremen huddles and morning huddles may be done separately. As such, each trade must provide a dedicated foreman or lead for each area to communicate, coordinate, and schedule work.

Contractor Grading

The general contractor and all trade partners will be graded weekly based on non-subjective criteria. The score will be scaled from F to A based on performance. This score will be communicated to the owner, all internal company leaders, all trade leaders and will be posted in the project conference room. The purpose of this is to manage expectations as a group and elevate everyone to high levels of performance. It is expected contractually that onsite teams reach a “B” or higher within 6 weeks of arriving onsite.

Worker & Foremen Safety Training

All workers will be OSHA 10 trained to be onsite. All foremen will be OSHA 30 trained to be onsite. If OSHA 10 trained workers are not available, an OSHA 30 trained foreman must be onsite with that crew 100% of the time.

Scheduling & Delivering Materials

Material deliveries will be scheduled on the project delivery software or on the delivery board on a first-come, first-served basis. Delivery times will be held. If deliveries arrive on the project out of sequence or not on time, they will be re-routed to a designated queuing area. All deliveries will be coordinated so they are offloaded to the proper area. Forklift operators, hoist operators, and crane operators will only stage per the coordinated logistics plan for the day. All materials will be packaged on color-coded pallets, on wheels, or otherwise mobile.

Takt Construction

This project will use Takt construction. It is expected that each contractor participates in pull plan sessions to create the Takt sequences and that each contractor will follow the Takt Production System explained in the book Takt Planning & Integrated Control. This system also requires the participation of trade foremen in the Trade Partner Weekly Tactical meeting and Daily Foremen Huddles. Each contractor shall work within their zone within their Takt time.

Want help writing lean into your contracts and exhibits? Talk to us about consulting or grab our templates.

On we go!

FAQ

Does writing lean into a contract cost more?

Not much. You move small costs up front, like setup time and huddles, to avoid using big contingency later.

What is a zero tolerance safety policy?

A clear rule that certain safety violations stop the work and send the worker back through orientation, and repeat or high-risk violations remove them from the project.

People Also Read:
Why Lean Must Be Written Into Construction Contracts
Lean in Contracts

If you want to learn more we have:

-Takt Virtual Training: (Takt Virtual Training)
-Check out our YouTube channel for more info: (Elevate Construction on YouTube)
-Listen to the Elevate Construction podcast: (Elevate Construction Podcast)
-Check out our training programs and certifications: (Training Programs and Certifications)
-The Takt Book: (The Takt Book on Amazon)

Discover Jason’s Expertise:

Meet Jason Schroeder, the driving force behind Elevate Construction. As the company’s Founder and COO, he’s dedicated to taking construction to new heights. With a wealth of industry experience, he’s crafted the Field Engineer Boot Camp and Superintendent Boot Camp – intensive training programs engineered to cultivate top-tier leaders capable of steering their teams towards success. Jason’s vision? To expand his training initiatives across the nation, empowering construction firms to soar to unprecedented levels of excellence.

Posted in All

The Eight Wastes: The Enemy Against Lean

Read 6 min

By: Lucía Armenta

Short answer: The 8 wastes of lean construction are defects, overproduction, waiting, non-utilized talent, transportation, inventory, motion and extra-processing, remembered as DOWNTIME. Each one uses time or money without adding value for the customer.

As builders, we must recognize that waste is a major obstacle on the job site. We need to take steps to avoid, decrease, and ultimately eliminate waste wherever possible.

In the world of Lean, waste is defined as anything that doesn’t directly create value. Therefore, we must prioritize the waste reduction from the design phase to the construction phase. By doing so, we can increase efficiency, minimize costs, and ultimately provide greater value to our clients.

The eight wastes of lean: the DOWNTIME acronym

What are the 8 wastes of lean construction?

An easy way to remember the eight wastes of lean is the acronym DOWNTIME:

· Defects

· Overproduction

· Waiting

· Non-utilized talent

· Transportation

· Inventory

· Motion

· Extra-processing

1. Defects

These are errors, mistakes, or deficiencies that occur during the construction process. Examples include poor workmanship, incorrect installation, incorrect measurements, or insufficient quality control. Defects can also result from mistakes or omissions in the design or planning stages, such as incorrect specifications, incorrect drawings, or incorrect material selection. To minimize defects, lean construction focuses on improving the overall quality of workmanship and ensuring that all team members are trained to identify and address potential issues in the construction process.

2. Overproduction

This waste refers to producing more than what is required or producing it too early in the process, which can result in excess inventory, waste of resources, and decreased efficiency. It can occur when there is a lack of coordination between teams, inadequate planning, or unclear specifications. In the construction process, producing too many units of a certain material before it is needed can result in excess inventory. To avoid overproduction, lean construction emphasizes the importance of just-in-time production, where materials and products are produced only when needed in the construction process.

3. Waiting

Waiting wastes occur when workers or resources are idle or waiting for materials, information, or equipment to arrive, which results in delays and decreased efficiency. They can occur at any stage of the construction process, from design to project completion. Examples of waiting wastes include waiting for materials to arrive on the job site, waiting for instructions or approvals, waiting for equipment to become available, and others. To minimize waiting wastes, lean construction emphasizes the importance of efficient project planning, scheduling, and communication.

4. Non-utilized talent

This waste refers to the underutilization or untapped potential of workers and teams, which results in a loss of value and decreased efficiency. It can occur when workers are not given the opportunity to fully utilize their skills, knowledge, and experience or when workers are not empowered to make decisions or participate in the improvement process. To minimize non-utilized talent, lean construction emphasizes the importance of empowering workers, providing adequate training and resources, and promoting collaboration and communication.

5. Transportation

This waste refers to the movement of people, equipment, or materials that do not add value to the construction process and can lead to waste and inefficiency. It can occur when materials or equipment are transported unnecessarily or over long distances, resulting in increased costs, delays, and potential damage or loss. To minimize transportation waste, lean construction emphasizes the importance of proper coordination and planning of the construction process. This includes identifying potential transportation bottlenecks and inefficiencies, consolidating transportation activities where possible, and using just-in-time delivery of materials and equipment.

6. Inventory

This waste refers to materials, equipment, or other resources that are not immediately needed for the construction process and are stored or held more than what is necessary to meet customer demand. It can occur when excess materials or equipment are purchased or produced in anticipation of future needs, resulting in unnecessary costs, storage space, and potential waste or damage. To minimize inventory waste, lean construction emphasizes the importance of just-in-time delivery of materials and equipment, where the resources are delivered only when needed for the construction process.

7. Motion

This refers to unnecessary movement of people while they work, such as walking back to the gang box, searching for tools, bending, reaching or climbing more than the task needs. It can occur when workers must repeatedly move between different work areas or when tools and equipment are not located in a convenient or easily accessible location, or when workers are not properly trained or have insufficient tools or equipment, resulting in excessive or inefficient movement. To minimize motion waste, Lean Construction emphasizes the importance of proper planning and organization of the construction process.

8. Extra-processing

Doing more work than the customer needs or values, such as extra steps, extra approvals, double handling of paperwork, re-inspecting work that was built right, or finishes nobody asked for. It adds cost and time without adding value. To minimize it, Lean construction defines what the customer actually needs and standardizes the work to that.

How the wastes feed each other

Finally, all the wastes of Lean construction are interrelated and can lead to inefficiencies and increased costs. Defects, overproduction, waiting, non-utilized talent, transportation, inventory, motion, and extra-processing can occur at any stage of the construction process, from design to project completion.

Each waste can contribute to the occurrence of other wastes and can create a cycle of waste that reduces efficiency and customer value. The goal of Lean construction is to minimize all types of waste through proper planning, coordination, and continuous improvement to optimize the flow of materials and information, reduce costs, and increase customer value.

So, what are you waiting for to start eliminating the eight wastes that plague the construction industry? Let’s do it!

Bibliography

McGee-Abe, J. (2015, August 12). The eight deadly lean wastes: DOWNTIME. Process Excellence Network. https://www.processexcellencenetwork.com/lean-six-sigma-business-performance/articles/the-8-deadly-lean-wastes-downtime

Lean Construction Institute. (2023, April 26). 8 Wastes of Lean: An Introduction to Waste. Lean Construction Institute. https://leanconstruction.org/lean-topics/8-wastes-of-lean/#:~:text=What%20Are%20the%208%20Wastes,Unused%20Creativity%20of%20Team%20Members.

Want your crews to see and remove waste every day? Check out our training or our Lean Superintendent program.

On we go!

FAQ

What does DOWNTIME stand for in lean?

Defects, Overproduction, Waiting, Non-utilized talent, Transportation, Inventory, Motion and Extra-processing.

Which waste is the worst in construction?

Overproduction, because building or stocking ahead of the work creates most of the other wastes: inventory, transportation, motion and waiting.

People Also Read:
Lean Onboarding Series – The 8 Wastes

If you want to learn more we have:

-Takt Virtual Training: (Takt Virtual Training)
-Check out our YouTube channel for more info: (Elevate Construction on YouTube)
-Listen to the Elevate Construction podcast: (Elevate Construction Podcast)
-Check out our training programs and certifications: (Training Programs and Certifications)
-The Takt Book: (The Takt Book on Amazon)

Discover Jason’s Expertise:

Meet Jason Schroeder, the driving force behind Elevate Construction. As the company’s Founder and COO, he’s dedicated to taking construction to new heights. With a wealth of industry experience, he’s crafted the Field Engineer Boot Camp and Superintendent Boot Camp – intensive training programs engineered to cultivate top-tier leaders capable of steering their teams towards success. Jason’s vision? To expand his training initiatives across the nation, empowering construction firms to soar to unprecedented levels of excellence.